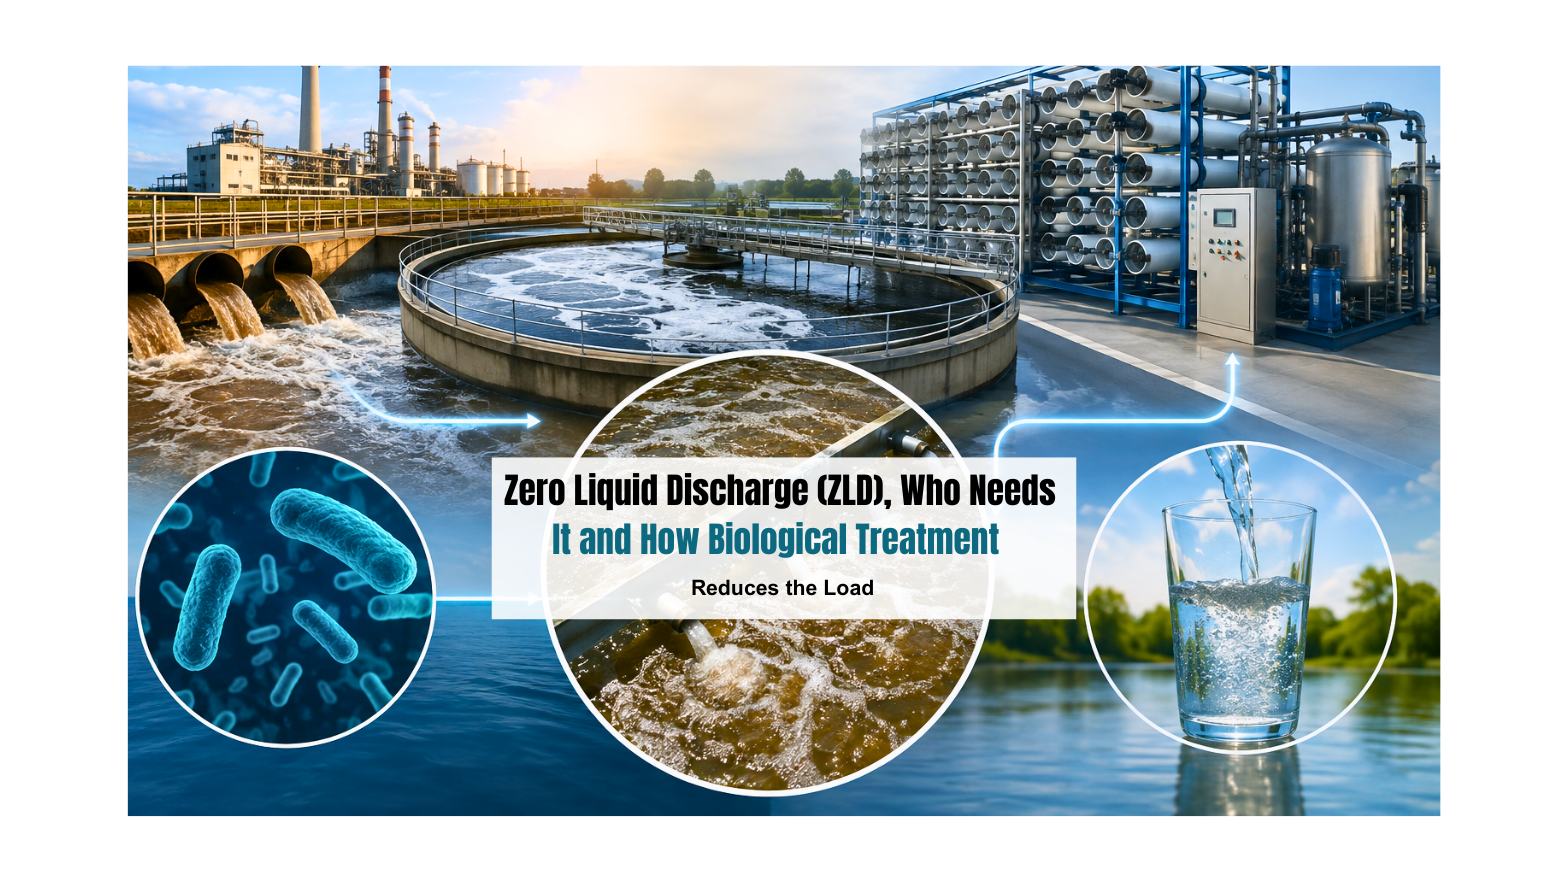
Zero Liquid Discharge (ZLD), Who Needs It and How Biological Treatment Reduces the Load

It is a Tuesday morning, and your compliance manager walks into your office with a printed directive. The letterhead reads CPCB. Somewhere in the second paragraph, the words “Zero Liquid Discharge” are underlined in red ink. The room goes quiet.

For a large number of plant directors and environmental heads across India, this is not a hypothetical. It is a moment that has already happened, or one they are quietly dreading. ZLD feels, at first glance, like an enormous, expensive, technically complex mandate handed down without a practical roadmap. The instinct is to panic, call three vendors, and receive three wildly different cost estimates that make things worse.

Before your team reaches that point, let us slow down. What ZLD actually means, which industries genuinely need it, what the compliance landscape looks like, and, most importantly, why the right biological treatment strategy can make the entire system far more manageable than the initial sticker shock suggests. That is what this guide is here to walk you through.

ZLD Full Form and What It Actually Means in Practice
ZLD Full Form and What It Actually Means in Practice

ZLD full form is Zero Liquid Discharge.

The definition, stripped of jargon, is this: a water management approach where no effluent leaves the plant boundary in liquid form. Every drop of wastewater generated within your facility is treated, recovered, and recycled back into your process. Nothing is discharged into a drain, a river, a municipal sewer, or any external body of water.

It is important to clarify what “zero” actually means here, because it trips people up. Zero Liquid Discharge does not mean zero water consumption. Your plant still uses water. It means zero untreated or partially treated liquid discharge leaving your premises. The water that enters must eventually either leave as solid waste, crystallised salts, sludge for disposal, or return to your process as recovered water.

In practice, a ZLD system moves through several stages. Incoming wastewater first goes through primary treatment, where solids and debris are removed. It then passes through secondary treatment, which is the biological stage, where microbial activity breaks down organic matter, reducing biochemical oxygen demand (BOD) and chemical oxygen demand (COD). After that comes tertiary treatment, including membrane filtration systems like reverse osmosis, which push water purity higher. Finally, the remaining concentrated reject stream goes through evaporation and crystallisation, where water is extracted as vapour and the dissolved solids are left behind as dry cake for disposal.

Each stage builds on the one before it. The quality of work done in your biological treatment stage directly determines how hard every stage after it has to work, and how much that costs you.

Zero Liquid Discharge India mandates are growing more stringent each year, and understanding the system architecture is the first step to approaching it rationally.

CETP Full Form and How It Fits Into the ZLD Conversation
CETP Full Form and How It Fits Into the ZLD Conversation

CETP full form is Common Effluent Treatment Plant.

A common effluent treatment plant is exactly what the name suggests: a shared treatment facility, typically set up by a cluster of small and medium-scale industries operating in proximity, to collectively treat their wastewater. Instead of each unit building and operating its own treatment infrastructure, which many small dyeing units, tanneries, or pharmaceutical manufacturers cannot afford, they pipe their effluent into a centralised CETP plant that handles treatment on their behalf.

In the context of industrial biochemistry, a CETP handles mixed-stream effluent. These streams tend to be complex: they carry high biological oxygen demand from organic matter, elevated chemical oxygen demand from synthetic compounds, variable pH, colour load, and in some cases heavy metals or residual solvents. The cetp full form in biochemistry context therefore implies not just shared infrastructure but shared biological and chemical treatment challenges, often in effluent streams that no single standard treatment protocol can address cleanly.

Here is where many industries make a dangerous assumption: they believe that discharging into a CETP exempts them from ZLD obligations. It does not. If your industry falls under a sector regulated for Zero Liquid Discharge, your wastewater does not get a free pass simply because it is pooled with others. The CETP itself may be required to meet ZLD norms, and the member industries may still carry regulatory responsibility. This is a compliance grey area that has caught several cluster units off guard during inspections.

Which Industries in India Are Legally Required to Implement ZLD
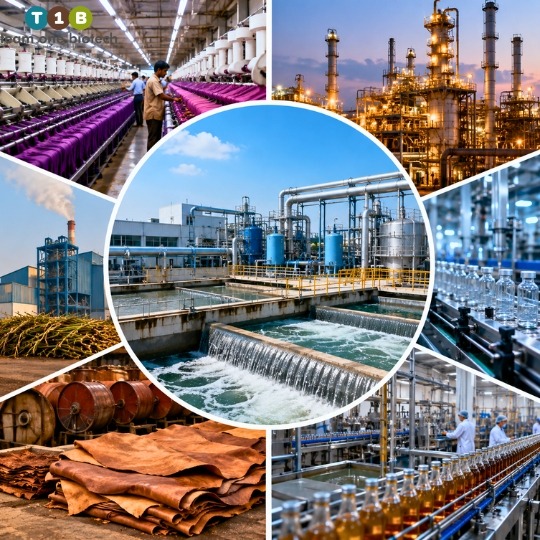
Which Industries in India Are Legally Required to Implement ZLD

The regulatory foundation here is significant. The Central Pollution Control Board (CPCB) and State Pollution Control Boards (SPCBs) across India have issued mandates requiring ZLD compliance for a defined set of industries, those characterised by high water consumption, complex effluent chemistry, and historically significant environmental impact. Non-compliance is not a matter of receiving a warning letter and carrying on. It can mean plant shutdown, cancellation of operating permits, and in serious cases, legal proceedings under the Environment Protection Act.

The following sectors are subject to ZLD mandates or intensive enforcement in India:

Textile and dyeing units sit at the top of this list. ZLD norms for textile industry India are among the most rigorously enforced in the country. Dyeing and bleaching operations generate effluent that is heavily coloured, high in TDS, and laden with reactive dyes that resist conventional treatment. Several SPCBs, particularly in Gujarat, Tamil Nadu, and Maharashtra, have issued sector-specific compliance timelines, and enforcement has become increasingly active. If your unit is in the textile or dyeing segment, ZLD is not a future consideration. It is a present obligation.

Distilleries and breweries generate some of the highest COD effluent loads of any industrial sector. Spent wash from distilleries is notoriously difficult to treat and has been the subject of specific SPCB directions in states including Uttar Pradesh, Maharashtra, and Punjab.

The sugar industry, while seasonal in its discharge cycle, produces large volumes of high-strength effluent during crushing season. The episodic nature of the discharge makes management harder, and ZLD requirements have been applied to sugar mills in several states.

Pulp and paper manufacturers have been on the CPCB’s regulated polluter list for decades. Effluent from paper mills contains chlorinated compounds, lignin, and high suspended solids loads that make discharge into natural water bodies unacceptable.

Pharmaceutical and bulk drug manufacturers are under increasing enforcement pressure, particularly in industrial clusters in Hyderabad (Patancheru, Bollaram) and Gujarat (Ankleshwar, Panoli). The effluent from bulk drug synthesis contains complex organic molecules, residual solvents, and active pharmaceutical ingredients that conventional treatment does not fully eliminate.

Tanneries produce effluent containing chromium compounds, sulfides, and high biological load, a combination that has resulted in severe enforcement action in clusters such as Vellore in Tamil Nadu and Kanpur in Uttar Pradesh.

Thermal power plants, particularly those managing ash pond discharge and cooling tower blowdown, face ZLD-adjacent requirements around water use efficiency and zero discharge from specific streams.

One important caveat: compliance requirements are not uniform across states. The CPCB sets the national framework, but SPCBs have discretion over timelines, specific norms, and enforcement intensity. Always verify your current obligations directly with your relevant state board or through a qualified compliance advisor.

ZLD vs ETP, Understanding the Difference Before You Invest
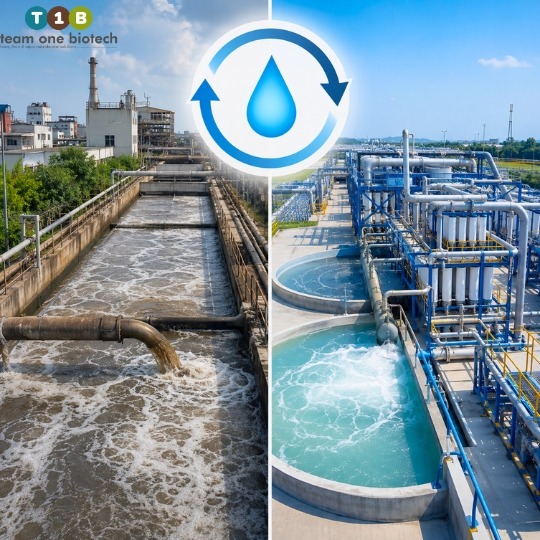
ZLD vs ETP, Understanding the Difference Before You Invest

When plant engineers and utility heads search for information on ZLD vs ETP, they are usually at a decision point: they have an existing system, they know something needs to change, and they are trying to understand how large that change needs to be.

An Effluent Treatment Plant, or ETP, treats your wastewater to permissible discharge limits and then releases the treated water, into a drainage channel, a river, or a municipal network, depending on your permit conditions. An ETP does its job and lets go of the water. It does not recover it.

A ZLD system does not let go. It goes several stages beyond an ETP, recovering water through membrane systems and thermal evaporation until nothing liquid remains to discharge. The recovered water goes back into your process. The residual becomes solid waste.

What is critical to understand is that ZLD is not a replacement for an ETP. It is an extension of one. A well-designed ETP with robust biological treatment is the foundation that a ZLD system is built on top of. You cannot skip the biological stage and bolt on an evaporator and expect things to work efficiently. That is not a technical opinion, it is a practical reality that plants across India have discovered the hard way.

Here is a general comparison of the two approaches:

ParameterETPZLD System
Liquid discharge allowedYes, within regulatory limitsNo liquid discharge permitted
Water recoveryPartialNear-complete
Primary cost driverChemical and biological treatmentEvaporation energy
Regulatory statusStandard compliance requirementMandatory for regulated sectors
Downstream destination of treated waterExternal drain, river, or sewerRecycled back into plant process

Disclaimer: The above is a general comparison. Actual performance parameters vary based on influent quality, plant design, technology selection, and operational conditions specific to each facility.

The underlying message: if you are in a regulated sector, ZLD is not an upgrade you choose. It is the standard you are required to meet. The question is not whether to build it but how to build it in a way that does not drain your operating budget every month.

Why Biological Treatment Is the Most Underrated Step in Any ZLD System

Here is where a great deal of industrial investment goes wrong, and where it can be corrected.

When the ZLD conversation starts inside a plant, the instinct is to focus on the visible, capital-intensive end of the system: the evaporators, the crystallisers, the multiple-effect evaporation units. These are the big-ticket line items. They look like the solution. And they are part of the solution, but they are the last part, not the whole.

The single most expensive mistake in ZLD system planning is rushing toward thermal evaporation without adequately addressing organic load upstream. The reason is straightforward: evaporation systems are energy-intensive by design. Every litre of water that enters an evaporator must be heated to the point of vaporisation. The higher the BOD and COD load in that water, the more the system fouls, scales, and struggles. The more it struggles, the more energy it consumes. The more energy it consumes, the higher your operating cost climbs, month after month, year after year.

Biological treatment, particularly advanced solutions using microbial consortia developed for specific effluent compositions, can reduce BOD and COD by a substantial margin before water reaches the thermal stage. This is not a marginal improvement. In well-designed systems, significant organic load reduction at the biological stage translates directly into reduced volume and strength of water entering evaporation, which translates into measurably lower energy consumption and operating expenditure.

What effective biological pre-treatment achieves within a ZLD system:

  • Significant reduction in BOD and COD before water reaches secondary and tertiary processing stages
  • Reduced fouling and scaling in membrane systems such as ultrafiltration and reverse osmosis, extending membrane life and cutting replacement frequency
  • Extended operational life of evaporation equipment by reducing the chemical aggressiveness of the concentrated stream
  • Lower consumption of chemicals in downstream polishing and pH correction stages
  • A materially reduced energy footprint for the ZLD system as a whole

The logic is simple: every unit of organic load you remove biologically is a unit of load your evaporator does not have to deal with. Biological treatment is cheaper per unit of load removed than thermal evaporation. Therefore, investing adequately in biological treatment before your evaporator is not a compromise, it is the economically rational decision.

Disclaimer: Reduction efficiencies vary depending on influent composition, hydraulic retention time, microbial culture selection, temperature, and plant-specific operating conditions. The benefits described above are indicative and reflect observations across typical industrial applications. Plant-specific assessment by a qualified engineer is recommended before system design decisions are made.

What Does a ZLD System Cost in India, And How Biological Treatment Affects That Number

One of the most common questions plant directors ask is straightforward: what will this cost?

The honest answer is that ZLD system cost in India varies considerably, and anyone who gives you a firm number without understanding your influent quality, discharge volume, recovery targets, and technology selection is guessing. Mid-sized industrial plants implementing ZLD in India have seen costs range from a few crores on the lower end, for plants with simpler effluent chemistry, existing pre-treatment infrastructure, and modest recovery requirements, to significantly higher for plants handling complex, high-volume, high-TDS effluent streams.

What matters more than the headline number is understanding where the costs come from and where they can be managed intelligently.

Capital cost in a ZLD system is dominated by evaporation and crystallisation equipment. These are expensive to procure, install, and maintain. Operating cost is dominated by energy, specifically the thermal energy required to run evaporators.

The single most effective lever available to reduce both capital and operating cost is upstream biological treatment. A plant that invests in a well-designed biological pre-treatment system can reduce the organic and dissolved load entering its evaporator. A reduced load means a smaller evaporator can do the job, lower capital cost. A reduced load also means less energy per litre of water processed, lower operating cost. Over a ten or twenty-year system life, the savings from right-sizing your evaporator based on biologically pre-treated water can be substantial.

Framed differently: the question is not whether biological treatment costs money. It does. The question is whether that investment reduces a larger cost elsewhere in the system. In well-designed ZLD systems, the answer is consistently yes.

Frequently Asked Questions

What is the ZLD full form?

ZLD full form is Zero Liquid Discharge, a wastewater management approach in which no liquid effluent is released outside the plant premises. All wastewater is treated, recovered, and recycled internally.

What is CETP full form in biochemistry?

CETP full form is Common Effluent Treatment Plant. In the context of industrial biochemistry, a CETP handles mixed effluent streams from multiple industries, typically streams with high biological oxygen demand and chemical oxygen demand, within a shared treatment facility serving an industrial cluster.

Is ZLD mandatory for textile industries in India?

Yes. ZLD norms for textile industry India have been mandated by CPCB and multiple State Pollution Control Boards, with particular enforcement focus on dyeing and bleaching units. Compliance timelines and specific norms differ by state, and units should verify their current obligations with their relevant SPCB.

How does biological treatment reduce ZLD operating costs?

By reducing BOD and COD before water reaches evaporation stages, biological treatment lowers the organic and dissolved load on energy-intensive thermal equipment. This reduces energy consumption, slows fouling of membranes and evaporators, and in many cases allows right-sizing of downstream equipment, cutting both capital expenditure and ongoing operating costs.

ZLD Is Not Optional, But It Does Not Have to Break Your Budget

Three things are worth carrying away from everything covered here.

First, Zero Liquid Discharge India compliance is a regulatory reality for most high-polluting industrial sectors, not a future consideration and not something that can be deferred indefinitely. The enforcement environment is tightening, and the cost of non-compliance, in legal exposure, reputational damage, and potential plant shutdown, is considerably higher than the cost of building the right system.

Second, biological treatment is the most underutilised cost-reduction lever in ZLD system design. Plants that invest in robust upstream biological pre-treatment consistently find that their downstream evaporation systems are smaller, cheaper to run, and longer-lasting than those of plants that skipped or underinvested in this stage.

Third, the intelligence in ZLD design is upstream. Over-sizing your evaporator because your biological treatment is inadequate is not a safety margin, it is an avoidable expense that compounds every time your energy bill arrives.

ZLD is not optional. But with the right treatment architecture, it does not have to define your plant’s economics in the way that first CPCB directive made it feel.

Team One Biotech works with industrial plants across India to design and deploy bioremediation solutions that make ZLD systems leaner, more efficient, and more cost-effective. Whether you are planning a new ZLD system or optimising an existing one, our technical team is ready to support you. Contact us today for a no-obligation consultation.

Disclaimer: Cost ranges mentioned above are general industry indicators and may vary significantly based on influent characteristics, plant scale, technology selection, and site-specific conditions. These figures should not be treated as project estimates. Detailed techno-commercial proposals from qualified vendors are essential for accurate cost assessment.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!
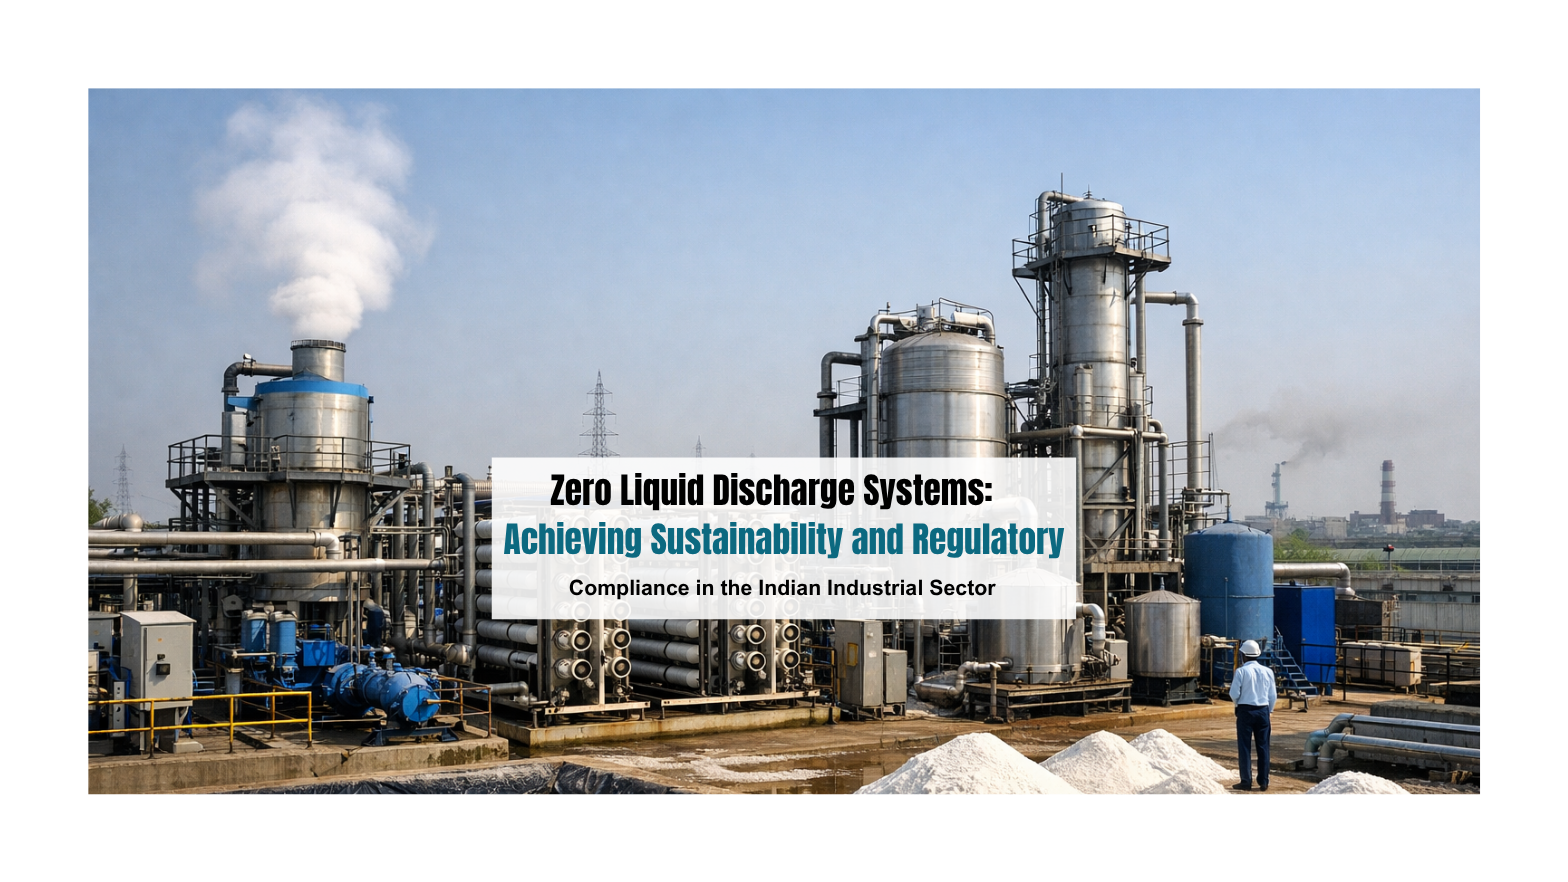
Zero Liquid Discharge Systems: Achieving Sustainability and Regulatory Compliance

There is a particular kind of pressure that plant managers in Ahmedabad, Ludhiana, Vapi, and Ankleshwar know intimately. It is not the pressure of a quarterly review or a supply chain delay. It is the pressure of standing at the edge of a genuine environmental reckoning, knowing that the decisions made in your facility today will determine whether your business exists a decade from now.

India’s industrial groundwater crisis is not a projection. It is a present-tense emergency. Textile dyeing clusters in Gujarat and Punjab collectively discharge millions of litres of high-TDS, chemical-laden effluent daily. The pharmaceutical corridor of Hyderabad generates wastewater streams so complex in their chemical signatures that conventional ETPs have routinely struggled to achieve consent standards. Chemical manufacturing clusters in Maharashtra and Rajasthan face escalating CPCB show-cause notices, NGT orders, and the looming reality of forced operational shutdowns. The question is no longer whether Indian industry must adopt Zero Liquid Discharge. The question is how to do it intelligently, cost-effectively, and in a way that creates genuine long-term competitive advantage.

This guide is written for those responsible for that decision.

What Zero Liquid Discharge Actually Means, Beyond the Regulatory Checkbox

The phrase “Zero Liquid Discharge plant” has become so common in compliance conversations that it risks losing its meaning. Strip away the regulatory context for a moment, and what ZLD water treatment actually represents is a fundamental reimagining of how industrial facilities relate to water as a resource.

In a conventional effluent treatment workflow, treated water is discharged into a water body or municipal drain after meeting prescribed quality norms. Even in well-managed facilities, this means a net loss of water from the industrial ecosystem. In a Zero Liquid Discharge system, no treated effluent leaves the plant boundary in liquid form. Every litre of wastewater generated by the production process is recovered, concentrated, and either recycled back into operations or converted into a solid or semi-solid residue for safe disposal. The water recovery rates achieved by well-engineered ZLD systems typically fall in the range of 90% to 98%, depending on influent quality and system configuration. Please note that these are general values and performance metrics vary significantly based on the specific ETP configuration and influent characteristics.

For a large-scale textile dyeing unit consuming 2 to 3 million litres of water per day, that recovery rate translates into tangible balance sheet impact. But beyond economics, it means achieving something that compliance documents rarely capture: true stewardship of a resource that is becoming structurally scarce across industrial India.

The Science of ZLD, Membrane Technology vs. Thermal Evaporation

Understanding why ZLD systems succeed or fail requires a working knowledge of the two dominant technology pathways available to Indian plant operators: membrane-based separation and thermal evaporation. The majority of modern ZLD installations combine both, but the design decisions around sequencing and sizing define the economics and performance of the entire system.

Membrane-Based ZLD Processes

Membrane technology forms the front end of most ZLD water treatment configurations because it is energy-efficient relative to thermal processes and capable of handling high volumes. The typical sequence involves ultrafiltration (UF) followed by reverse osmosis (RO), often with a second or third-pass RO stage for high-TDS applications.

Ultrafiltration removes suspended solids, colloidal matter, and larger organic molecules through a pressure-driven membrane with pore sizes in the 0.01 to 0.1 micron range. This stage is critical because it protects the downstream RO membranes from fouling, a failure mode that is responsible for the majority of ZLD plant operational disruptions in Indian industrial facilities.

Reverse osmosis then handles the bulk of dissolved solids rejection. A single-pass RO stage at a well-operated ZLD plant will typically achieve water recovery in the range of 50% to 75% of the feed volume, producing a concentrated reject stream with significantly elevated TDS levels. Please note that these are general values and performance metrics vary significantly based on the specific ETP configuration and influent characteristics.

This concentrate, sometimes called brine, cannot simply be discharged. In a ZLD configuration, it must be further processed. This is where the thermal stage begins.

Thermal Evaporation and Crystallisation

The concentrate stream from the RO stage enters the thermal section of the ZLD plant, which typically comprises a multiple-effect evaporator (MEE) and, in full ZLD configurations, a crystalliser downstream.

Multiple-effect evaporators work by using the steam generated in one effect to heat the feed in the next, recovering energy across several stages. This cascading approach reduces the specific energy consumption of the evaporation process, a critical consideration given that thermal processes remain significantly more energy-intensive than membrane processes. MEE systems operating on industrial brine streams typically achieve evaporation efficiencies in the range of 30% to 45% steam economy, meaning each kilogram of primary steam drives evaporation of 30 to 45 kilograms of water across the effects. Please note that these are general values and performance metrics vary significantly based on the specific ETP configuration and influent characteristics.

The crystalliser handles the final concentration step, forcing dissolved salts out of solution into a crystalline solid. Depending on the feed chemistry, the resulting salt may have commercial recovery value, a point we will return to in the economic analysis section, or may require regulated disposal as solid hazardous waste under the Hazardous Waste Management Rules, 2016.

The total specific energy consumption of a combined membrane-thermal ZLD system varies considerably by application and influent TDS, but typically falls in the range of 15 to 35 kWh per kilolitre of feed processed. Please note that these are general values and performance metrics vary significantly based on the specific ETP configuration and influent characteristics.

Total Dissolved Solids in Water, The Industrial Damage You Cannot Always See

Total Dissolved Solids in Water, The Industrial Damage You Cannot Always See

One of the most underappreciated aspects of industrial water quality management is the cumulative, progressive damage caused by elevated TDS in water, both to production equipment and to the receiving environment. Plant managers often focus on visible pollution indicators, colour, COD, BOD, while TDS builds silently until it manifests as capital equipment failure or regulatory action.

Total dissolved solids in water is a composite measurement of all inorganic and organic matter dissolved in a water sample, expressed in milligrams per litre (mg/L) or parts per million (ppm). In industrial contexts, the TDS profile of a water source includes a complex matrix of calcium, magnesium, sodium, potassium, chloride, sulphate, bicarbonate, and a range of process-specific dissolved solids depending on the industry.

Equipment Degradation and Production Losses

High-TDS process water accelerates scaling in boilers, heat exchangers, cooling towers, and pipelines. Calcium carbonate and calcium sulphate scale deposits in boilers reduce heat transfer efficiency, increase fuel consumption, and create hot spots that contribute to premature tube failure. Scaling in cooling tower fill media and distribution systems reduces thermal efficiency and increases biological fouling risk.

The economic cost of unmanaged TDS in industrial cooling and steam generation systems, when expressed as increased energy consumption, maintenance expenditure, and unplanned downtime, typically ranges between 8% to 18% of total utility costs in affected facilities. Please note that these are general values and performance metrics vary significantly based on the specific ETP configuration and influent characteristics.

In textile processing, high-TDS process water directly degrades dyeing outcomes. Elevated calcium and magnesium concentrations interfere with dye uptake, leading to inconsistent colour yield, increased dye and chemical consumption, and quality rejections, none of which show up in an effluent compliance report, but all of which represent real production costs.

Environmental and Regulatory Dimensions of TDS

From a regulatory standpoint, the CPCB has prescribed TDS limits for treated effluent discharge to inland surface waters, with general standards typically setting a threshold that many high-intensity industrial effluents significantly exceed prior to treatment. State Pollution Control Boards in Gujarat, Maharashtra, Tamil Nadu, and Telangana have issued sector-specific consent conditions with TDS limits that reflect the cumulative carrying capacity of local water bodies.

The NGT has repeatedly intervened on TDS-related environmental harm, particularly in cases where high-TDS industrial discharge has resulted in soil salinity damage to agricultural land downstream of industrial clusters. Penalties in such cases have ranged from facility closures to compensation orders running into crores of rupees.

Monitoring and controlling TDS is therefore both an equipment protection imperative and a core water quality parameter in the regulatory compliance framework governing Indian industry.

Where Bioremediation Fits, Team One Biotech’s Role in the ZLD Ecosystem

Where Bioremediation Fits, Team One Biotech's Role in the ZLD Ecosystem

A critical and often misunderstood aspect of ZLD plant design is that membrane and thermal technologies work best when the organic load in the influent has been substantially reduced before the feed stream reaches the ZLD train. High COD and BOD in the ZLD feed stream causes accelerated membrane fouling, reduces flux rates, increases cleaning frequency, and shortens membrane life, all of which translate directly into higher operating costs and reduced system availability.

This is where biological pre-treatment, and specifically bioremediation using specialised microbial consortia, plays a decisive upstream role.

Team One Biotech’s bio-augmentation solutions are designed to address precisely this challenge. By deploying high-performance, application-specific microbial consortia into the ETP biological treatment stage, organic degradation efficiency is substantially enhanced before the effluent stream approaches the ZLD feed header. The result is a lower-COD, lower-TSS feed to the membrane stage, with measurable downstream benefits across the entire ZLD system.

In industrial ETP configurations where bio-augmentation has been applied prior to the ZLD train, facilities have reported reductions in RO membrane cleaning frequency, extended membrane replacement intervals, and lower specific chemical consumption in the CIP (Clean-In-Place) process. Organic load reduction at the biological stage translates into a cleaner, more consistent ZLD feed, which is the single most important controllable variable in long-term ZLD system performance.

For plant managers operating in textile, pharma, or chemical manufacturing, integrating bio-augmentation into the ETP prior to the ZLD investment is not a supplementary consideration. It is a foundational design decision that affects the capital cost, operating cost, and operational reliability of the entire ZLD installation.

If you are in the pre-engineering or FEED phase of a ZLD investment, consult with our compliance specialists to future-proof your facility, and ensure that your biological pre-treatment strategy is designed to support, rather than compromise, your ZLD performance targets.

The Regulatory Roadmap, What Indian Law Actually Requires, and What Non-Compliance Costs

The regulatory framework governing industrial effluent management in India has become substantially more stringent in the past decade, driven by a combination of NGT activism, CPCB enforcement, and a series of Supreme Court interventions that have fundamentally changed the risk calculus for industrial polluters.

CPCB and SPCB Mandate Overview

The Environment (Protection) Act, 1986 and the Water (Prevention and Control of Pollution) Act, 1974 form the legislative backbone of industrial effluent regulation in India. The CPCB issues general standards for effluent discharge under the Environment (Protection) Rules, 1986, while State Pollution Control Boards issue facility-specific Consent to Operate (CTO) conditions that translate these general standards into site-specific obligations.

The CPCB has progressively tightened effluent standards across highly polluting industries, a category that includes large-scale textile processing, pharmaceuticals, dyes and dye intermediates, chlor-alkali, and tanneries, among others. For textile dyeing and printing units, the CPCB’s sector-specific standards prescribe not only COD, BOD, and TSS limits but also colour and TDS benchmarks that are effectively unachievable without a ZLD or near-ZLD configuration.

NGT Mandates and Their Implications

The National Green Tribunal has been an active enforcement actor, particularly in relation to industrial clusters. The NGT’s orders on the Pali textile cluster in Rajasthan, the Tirupur dyeing cluster in Tamil Nadu, and the CETP-linked industries in Vapi have established a clear judicial posture: industries that fail to achieve prescribed effluent quality standards face closure orders that the Tribunal has shown willingness to enforce. The NGT has also directed that industries within specified distances of sensitive water bodies must achieve ZLD, regardless of whether their effluent technically meets individual discharge norms.

The True Cost of Non-Compliance

The financial risk of non-compliance extends significantly beyond the direct penalty amounts prescribed under environmental statutes, which themselves have been enhanced in recent years. Facilities facing enforcement action under the Water Act or the Environment Protection Act risk suspension of Consent to Operate, which triggers immediate production stoppage. In industries where CTO suspension affects export-linked operations, the consequential losses from order cancellations, customer penalties, and bank covenant breaches can dwarf the original environmental fine by orders of magnitude.

Beyond immediate financial exposure, unresolved compliance failures increasingly affect access to institutional credit. Several scheduled banks and development finance institutions now incorporate environmental compliance status into credit appraisal frameworks, particularly for loans above certain thresholds. Facilities with pending SPCB notices or NGT orders are encountering difficulties in loan renewals and capacity expansion financing.

The question, for any serious industrial leader, is not whether the cost of ZLD investment is justified. It is whether the business can afford the compounding cost of deferring it.

The Economic Case for ZLD, Turning Waste Streams Into Working Capital

The Economic Case for ZLD, Turning Waste Streams Into Working Capital

The financial argument for ZLD water treatment has shifted materially over the past five years, for two reasons. First, freshwater costs have risen across Indian industrial belts as groundwater depletion has forced industry toward tanker supply, Common Effluent Treatment Plant charges, and municipal industrial supply, all more expensive per kilolitre than the groundwater sources they replace. Second, ZLD technology costs, particularly on the membrane side, have declined meaningfully as the Indian market for UF and RO membranes has deepened.

Water Recovery as Cost Avoidance

For a large-scale industrial facility consuming between 1 and 5 million litres of process water per day, ZLD water recovery at 90% to 95% recovery efficiency effectively replaces 9 to 9.5 of every 10 litres with recycled water. Expressed as cost avoidance at current industrial water supply costs in water-stressed states like Gujarat, Rajasthan, and Maharashtra, this represents a significant annual saving. Plants that have transitioned from tanker-dependent fresh water supply to ZLD-recovered water have reported reductions in freshwater procurement costs in the range of 55% to 75% of their pre-ZLD water expenditure. Please note that these are general values and performance metrics vary significantly based on the specific ETP configuration and influent characteristics.

Salt Recovery and Secondary Revenue

Pharmaceutical and chemical sector ZLD installations that generate high-purity crystallised sodium chloride, sodium sulphate, or ammonium sulphate from their crystalliser output have explored the potential for secondary revenue through salt recovery. Where the recovered salt stream is sufficiently pure and consistent, it may be saleable to commercial salt processors or industrial users, partially offsetting the operating cost of the crystallisation stage. The commercial viability of this depends on the specific salt type, purity, and available off-take arrangements in the local market.

The Payback Period Question

ZLD systems carry significant capital investment, and it would be misleading to present this as a low-cost option. However, the payback period calculation must include the avoided cost of regulatory penalties, the insurance value against forced production shutdowns, the freshwater cost savings, and, where applicable, the value of recovered salt or heat. When these factors are aggregated, well-structured ZLD investments in high-water-intensity industries have demonstrated payback periods in the range of 5 to 9 years in Indian industrial contexts. Please note that these are general values and performance metrics vary significantly based on the specific ETP configuration and influent characteristics.

For high-value manufacturing, speciality chemicals, pharmaceutical APIs, technical textiles, where a single production shutdown carries costs that can exceed the entire ZLD capital investment, the insurance logic alone may justify the expenditure independent of the operating economics.

Request a technical audit of your recovery cycle to develop a facility-specific ROI model before making a capital commitment.

Maintenance, Failure Modes, and Operational Discipline in ZLD Plants

The most common reason ZLD plants fail to deliver on their design performance in Indian industrial settings is not a technology deficiency. It is a gap between the operational discipline required to run a ZLD system and the institutional capability of the facility managing it.

Membrane Fouling, The Primary Failure Mode

RO membrane fouling is the single most common cause of underperformance and premature failure in ZLD installations. Fouling occurs when dissolved or suspended matter accumulates on or within the membrane matrix, reducing flux and increasing trans-membrane pressure. In Indian industrial applications, the leading foulants are calcium carbonate scale, silica scale, biological fouling, and organic matter.

Prevention requires consistent monitoring of the Silt Density Index (SDI) of the UF permeate, rigorous adherence to CIP protocols at defined intervals, antiscalant dosing at correctly calibrated rates, and temperature monitoring of the feed stream. Membrane life in well-operated ZLD plants typically falls in the range of 5 to 8 years per module. In poorly maintained systems, premature failure at 2 to 3 years is not uncommon. Please note that these are general values and performance metrics vary significantly based on the specific ETP configuration and influent characteristics.

Evaporator Scaling and Corrosion

In the thermal section, scaling on heat exchanger surfaces and corrosion of wetted materials are the primary maintenance concerns. Evaporators handling high-chloride brine streams require careful materials selection, typically duplex stainless steel or titanium, and regular descaling to maintain heat transfer efficiency. Facilities that undersize their descaling budget invariably face higher long-term operating costs than those that invest in preventive maintenance at the prescribed intervals.

Instrumentation and Control Systems

ZLD plants are highly instrumented systems, and the failure of online analysers, particularly TDS, pH, and flow meters, frequently cascades into process deviations that compromise effluent quality or damage equipment. Maintaining a calibrated spare instrument inventory and conducting scheduled calibration checks on all critical online instruments is a non-negotiable operational discipline for ZLD plants that consistently perform to design.

For facilities experiencing persistent performance gaps in their existing ZLD or ETP systems, a structured root-cause diagnostic is typically more cost-effective than a capital investment in additional treatment stages. Request a technical audit of your recovery cycle to identify where your current system is losing performance, and what it will take to recover it.

Building a Compliance-Ready Industrial Operation for the Next Decade

The Indian regulatory trajectory on industrial water management is unambiguous. The CPCB’s online continuous effluent monitoring mandates, the NGT’s willingness to impose closure orders, and the integration of environmental compliance into credit and insurance frameworks all point in the same direction: facilities that treat environmental compliance as a fixed cost to be minimised will find that cost rising dramatically. Facilities that treat water stewardship as a strategic investment will find it creates competitive insulation.

ZLD water treatment is not a small undertaking. It requires significant capital, genuine operational capability, and a willingness to maintain system discipline over years rather than quarters. But for industries in India’s most water-stressed and regulatory-scrutinised sectors, it is increasingly not a choice. It is the price of continued operation.

The question is not whether to make this transition. The question is whether to make it on your own terms, with a technology and pre-treatment configuration that maximises recovery and minimises long-term operating cost, or to make it reactively, under enforcement pressure, with the timeline and cost structure determined by a regulator rather than a business case.

Team One Biotech works with plant managers and facility heads to ensure that the biological pre-treatment foundation supporting your ZLD investment is engineered to deliver the feed quality your membrane and thermal systems need to perform. If you are planning a ZLD investment, expanding an existing ETP, or facing compliance challenges that require a technical response rather than a regulatory one, consult with our compliance specialists to future-proof your facility.

The water is not coming back on its own. But with the right systems in place, you can make sure your facility never has to depend on it from outside again.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!
Zero Liquid Discharge (ZLD): Can Bioremediation Make It Cost-Effective?

The global water crisis continues to intensify, driven by pollution and scarcity. This issue not only threatens current industries but also poses long-term environmental risks. To address these challenges, modern wastewater treatment innovations have introduced Zero Liquid Discharge (ZLD) — a comprehensive system that enables industries to recover, reuse, and recycle water with minimal environmental impact.Upgrade your wastewater management with Team One Biotech — delivering advanced biological treatment solutions that make sustainability and cost-efficiency work together contact us now.

What is Zero Liquid Discharge (ZLD)?

Zero Liquid Discharge is an effluent treatment process designed to ensure that no wastewater is released into the environment. It enables complete water recovery while isolating solid residues such as sludge and salts for disposal.

Industries such as textiles, power plants, chemicals, and pharmaceuticals frequently deal with high TDS, high COD and BOD, and ammonical nitrogen reduction challenges. In such cases, ZLD in wastewater treatment ensures efficient resource utilization while maintaining environmental compliance. The ultimate goal is zero discharge and maximum water reuse.Wastewater treatment is an essential step toward achieving Zero Liquid Discharge, ensuring that every drop of effluent is treated, recycled, and reused to minimize environmental impact.

Illustration of the process:

The Cost Factor in ZLD Implementation

While Zero Liquid Discharge systems are highly effective, they also involve significant CAPEX and OPEX. Implementation can increase wastewater treatment costs by up to 300% when dependent solely on physical and chemical processes. Incorporating biological or anaerobic treatment stages can substantially reduce these expenses and improve long-term sustainability.

How Does a ZLD System Work?

A standard ZLD process integrates physical, chemical, and biological stages to achieve complete recovery. The primary stages include:

1. Pre-Treatment

This step removes suspended solids, oils, and greases through chemical dosing, pH correction, and equalization. It ensures that the influent entering the next stages is stable and easier to process.

2. Biological Treatment

This involves microbial degradation of organic matter to lower COD and BOD levels. Commonly applied in textile, pharma, and tannery industries, it helps minimize scaling, fouling, and odour issues.

3. Reverse Osmosis (RO) / Membrane Bioreactor (MBR)

These systems separate clean water from dissolved salts and pollutants. The permeate is reused within the plant, while the reject moves to the evaporation stage for further concentration and recovery.

4. Evaporation (Multi-Effect Evaporator – MEE)

RO rejects are treated in Multi-Effect Evaporators (MEE) or Mechanical Vapour Recompression (MVR) units. These thermal processes recover clean water through vapor condensation while concentrating the remaining brine.

5. Crystallization

The final step converts concentrated brine into solid form for safe disposal or possible recovery, ensuring complete zero liquid discharge.

Challenges in Sustaining ZLD Operations

Despite its benefits, maintaining Zero Liquid Discharge operations is often difficult due to technical and operational constraints.

High Energy Consumption

Evaporators and crystallizers require large amounts of steam or electricity, accounting for 40–60% of total ZLD OPEX. High COD, TDS, and ammonical nitrogen loads further increase energy consumption.

Scaling and Fouling

Inadequate pre-treatment or high phenol content can lead to scaling and fouling in RO membranes. This reduces permeate recovery, increases cleaning frequency, and shortens membrane life.

Frequent Shutdowns

Industries handling variable effluents—such as textile, dye, and pharmaceutical units—face fluctuations in high COD and BOD loads. This can trigger growth of filamentous bacteria, excess sludge formation, and frequent system shutdowns, increasing operational costs.

Role of Bioremediation in Cost Reduction

Bioremediation offers a sustainable solution for optimizing effluent treatment in ZLD systems. By utilizing specialized microbial strains bioculture, it enhances organic degradation, minimizes sludge generation, and stabilizes biological processes.

Key benefits include:

1. COD and BOD Reduction

Microbes effectively degrade organic compounds, reducing COD/BOD by up to 90%. This lowers aeration energy and chemical usage, while preventing membrane fouling.

2. Sludge Reduction

Bioremediation converts organic waste into carbon dioxide and water, resulting in minimal sludge accumulation and preventing MEE tube blockage. This reduces power and maintenance requirements.

3. Reduced Evaporator Load

Improved settling and clear supernatant reduce the volume sent to evaporators, cutting down energy demand and improving overall ZLD efficiency.

4. Enhanced Operational Stability

By controlling filamentous bacteria and supporting anaerobic treatment, bioremediation strengthens system resilience, stabilizing operations during variable or shock loads.

Compliance and Environmental Benefits

Implementing bioremediation aligns with NGT, CPCB, and PCB guidelines for zero discharge systems. It ensures reduced reliance on chemicals, improved odour control, and better compliance with national environmental regulations. The approach contributes to sustainable development goals by promoting biological wastewater treatment over purely mechanical systems.

Conclusion: Achieving Cost-Effective Zero Liquid Discharge

Zero Liquid Discharge remains critical for sustainable industrial wastewater management, but its high operational costs require strategic optimization. Incorporating bioremediation enhances biological pre-treatment, reduces sludge generation, and improves overall efficiency, making ZLD more affordable and environmentally responsible.

When properly managed, pretreated effluent acts like a well-balanced system—easier to process, more energy-efficient, and more reliable. Integrating bioremediation ensures long-term operational stability and significant cost savings for industries implementing ZLD in wastewater treatment.Achieve compliance, efficiency, and sustainability in every drop. Get in touch with Team One Biotech for expert-driven ZLD solutions.

To achieve sustainable Zero Liquid Discharge with reduced operational costs, contact Team One Biotech for tailored biological solutions. 

As one of the leading biotech companies in India and trusted bioremediation companies in India, Team One Biotech continues to deliver solutions that redefine sustainability across wastewater treatment, agriculture, aquaculture, and hygiene management.

Email: sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!
Scan the code