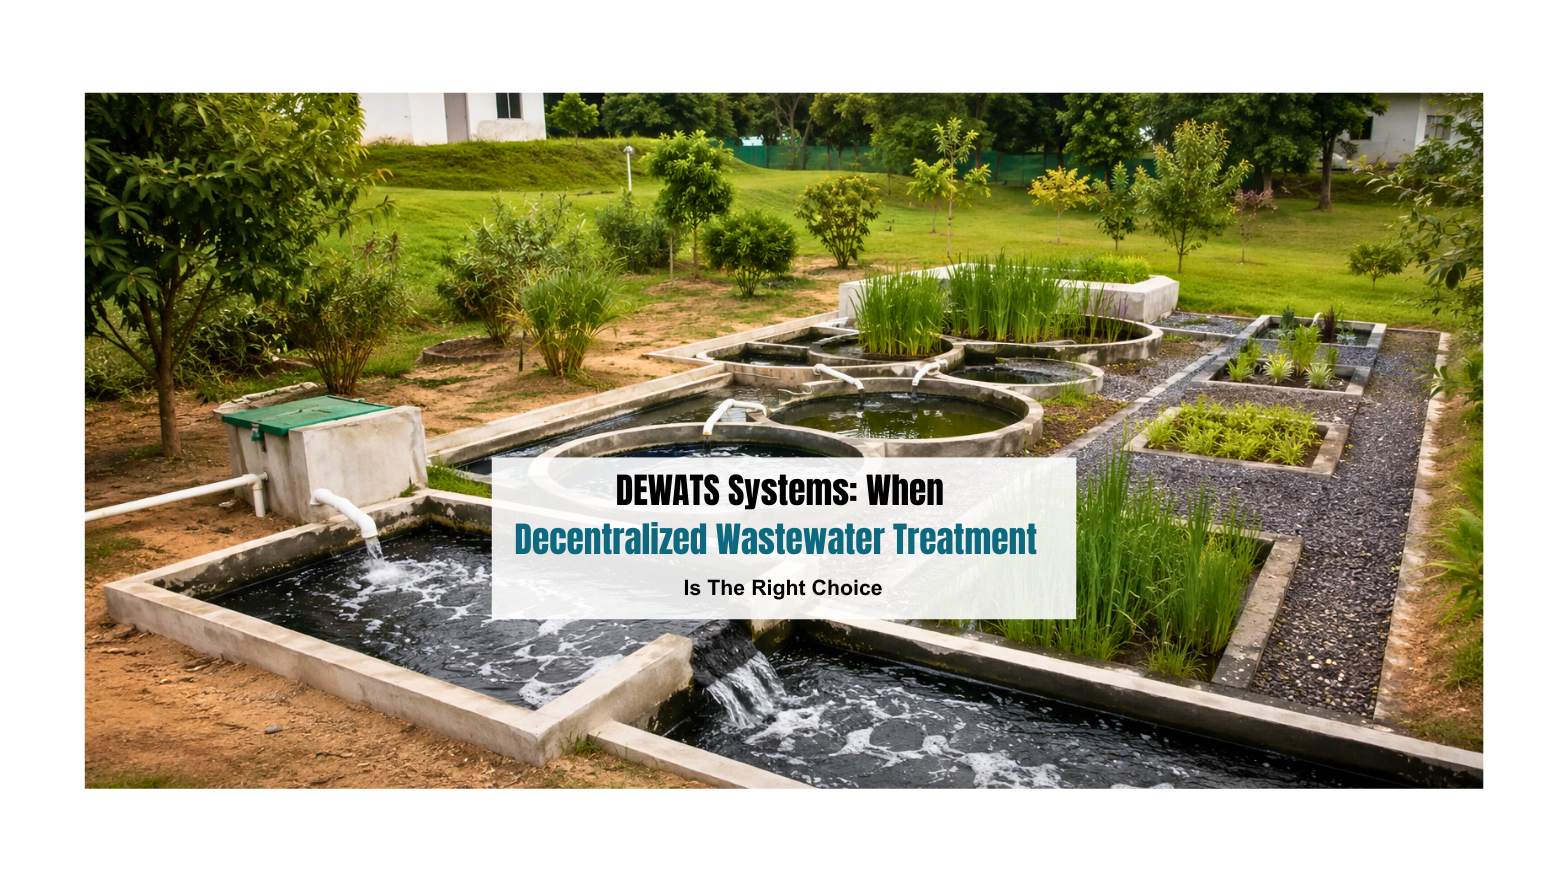
DEWATS Systems: When Decentralized Wastewater Treatment Is The Right Choice

You’ve got a residential project half-built, occupancy certificates are pending, and the municipal sewage line your project was supposed to connect to is still years away from actually reaching your site. Or maybe you’re running a hospital campus and you’ve just received a compliance notice because your existing treatment setup can’t keep pace with the load. Or you’re a facility manager fielding complaints from residents about tanker trucks rumbling through the gate every other day, kicking up dust and leaving behind that unmistakable smell.

These aren’t rare scenarios. They’re the everyday reality for a lot of developers, campus managers, and municipal planners across India who assumed centralized sewage infrastructure would simply be there when they needed it, and then discovered it wasn’t, or wouldn’t be for a long while.

This is where DEWATS systems enter the conversation. DEWATS stands for Decentralized Wastewater Treatment System, and at its core, it’s a philosophy as much as a technology: treat wastewater close to where it’s generated, using biological and gravity-driven processes instead of leaning on heavy machinery, constant electricity, or a sprawling network of pipes connecting back to a central plant.

In this article, we’ll walk through how DEWATS systems actually work, when they make more sense than a centralized treatment plant, how they help you stay compliant with CPCB and SPCB norms, and what to look for when picking a provider. If you’re weighing your options for a new project, a campus expansion, or a township that’s outgrown its current setup, this should give you a clear, practical starting point.

What Is a DEWATS System, and How Does It Actually Work
What Is a DEWATS System, and How Does It Actually Work

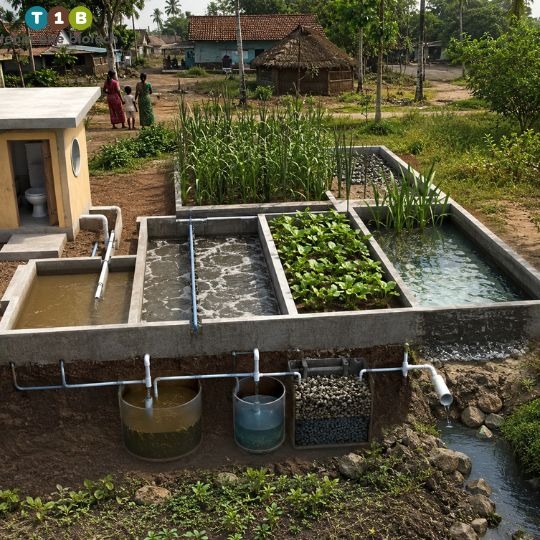
The DEWATS full form, Decentralized Wastewater Treatment System, tells you most of what you need to know upfront. It’s decentralized, meaning treatment happens on-site or close to the source rather than being piped miles away to a centralized municipal plant. And it’s designed around a simple idea: let natural biological processes, combined with smart engineering, do the heavy lifting instead of pumps, blowers, and constant power draw.

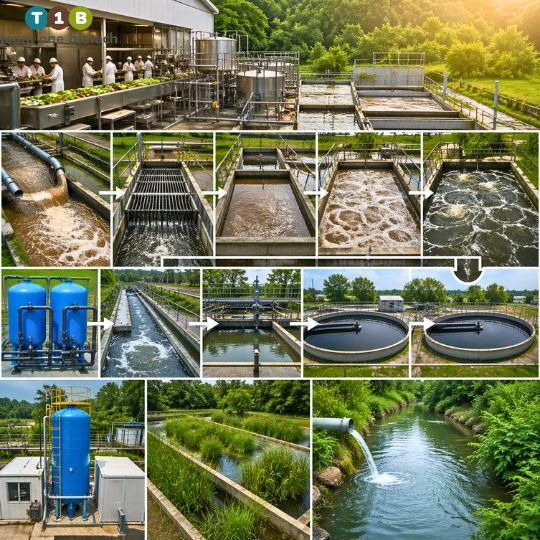
A typical DEWATS setup moves wastewater through a series of stages, each one doing a specific job:

  • Settling and primary treatment (often an anaerobic baffled reactor): Wastewater first passes through chambers where solids settle out and anaerobic bacteria begin breaking down organic matter, all without any mechanical agitation.
  • Anaerobic filtration: The partially treated water then moves through filter media, where bacteria attached to the filter surface continue digesting remaining organic pollutants.
  • Root zone treatment, also called constructed wetland treatment: Water is directed through a planted gravel bed, where plant roots and the surrounding microbial ecosystem absorb and break down nutrients and remaining contaminants.
  • Polishing pond or final treatment stage: A final holding stage allows further natural purification before the water is discharged or reused, often for irrigation or landscaping.

What makes this approach genuinely appealing to developers and facility managers is what’s absent from the process. There’s no dependency on continuous electricity, no complex array of moving mechanical parts that need constant servicing, and no requirement for specialized operators running the plant around the clock. That translates into a system that’s far less likely to break down, far cheaper to keep running, and far more forgiving if your site experiences power cuts, which, let’s be honest, is not exactly a rare occurrence in a lot of semi-urban and rural parts of the country.

Root Zone Treatment and Constructed Wetlands Explained
Root Zone Treatment and Constructed Wetlands Explained

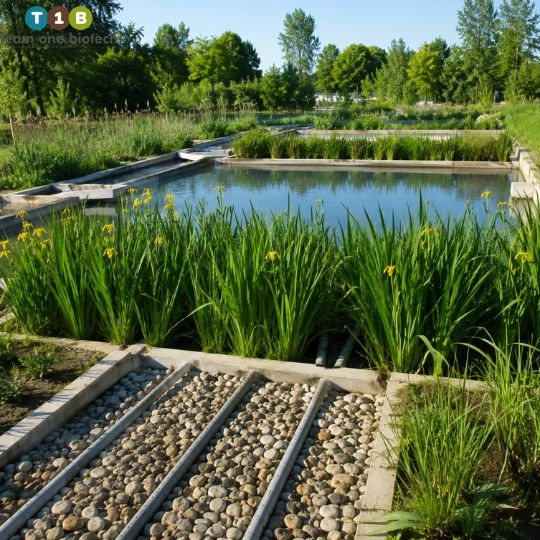
Root zone treatment deserves its own spotlight because it’s genuinely one of the more elegant pieces of this whole system, and it’s also the part that tends to win over clients who care about sustainability.

Here’s the basic concept: wastewater flows horizontally or vertically through a bed of gravel planted with specific wetland species, think reeds, canna, or similar hardy plants. The plant roots create a dense underground network that hosts a thriving community of microorganisms. Those microorganisms do the actual pollutant breakdown, while the plants themselves absorb nutrients and help maintain the right conditions for the biological process to keep working efficiently.

From the outside, a constructed wetland doesn’t look like a treatment plant at all, it looks like a landscaped garden bed. That’s a real selling point for real estate developers who don’t want an eyesore near their clubhouse or entrance, and for campus managers who’d rather have a green space than a mechanical structure humming away in the background.

There’s also a quieter appeal here for the more eco-conscious client. Root zone treatment leans almost entirely on natural processes, produces minimal sludge compared to conventional mechanical systems, and generally requires far less day-to-day intervention. For a project head managing a rural township or a campus with a small maintenance team, that lower-maintenance profile can be the deciding factor over a system that demands specialized technicians and constant monitoring of mechanical components.

DEWATS vs Centralized Treatment: When Decentralized Wins
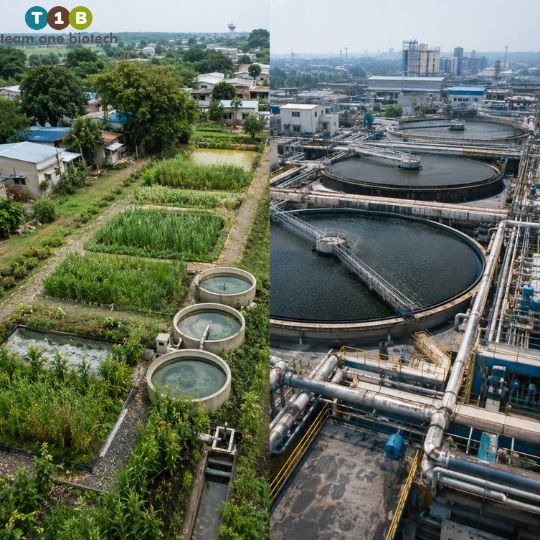
DEWATS vs Centralized Treatment: When Decentralized Wins

This is usually the question that actually brings people to an article like this one: should we go decentralized, or should we wait for or invest in a centralized system? The honest answer is that it depends on your specific project, but there are some decision factors that consistently tip the scale one way or the other.

Site location and distance from municipal sewer lines. If your project sits well outside the existing municipal sewage network, which is common for townships on the outskirts of growing cities, or for campuses in semi-urban areas, running a connecting pipeline can involve a long wait and a significant capital outlay. A DEWATS system sidesteps that dependency entirely.

Land availability and layout flexibility. Centralized plants typically need a sizeable, dedicated plot, often at a specific point in the drainage layout. DEWATS systems, by contrast, can often be designed to fit into irregular or constrained plots, and in the case of root zone treatment, can even double as usable green space.

Budget and phased development. Many real estate projects are built and occupied in phases. A decentralized system can often be scaled or expanded in step with construction phases, whereas a centralized plant usually requires the full design capacity to be committed to upfront.

Community size and scalability needs. For scattered residential clusters, smaller townships, or campuses with a defined and fairly stable population, a decentralized approach avoids the inefficiency of over-building a large centralized plant for a population that doesn’t need that scale.

Energy and grid reliability concerns. In areas where power supply is inconsistent, a system that doesn’t lean heavily on electricity for its core treatment stages is a genuinely practical advantage, not just a sustainability talking point.

To be clear, centralized systems absolutely have their place. For large, dense urban developments with strong grid reliability and an existing municipal network close at hand, a well-designed centralized plant can offer economies of scale that a decentralized approach won’t match. The point isn’t that one approach is universally superior, it’s that the right choice depends on where your project sits, how it’s phased, and what your site conditions actually look like. A credible design partner should be willing to have that honest conversation with you rather than pushing one solution regardless of fit.

Compliance Angle: Staying on the Right Side of CPCB/SPCB Norms
Compliance Angle: Staying on the Right Side of CPCB/SPCB Norms

Here’s the part that often gets underestimated until it becomes a crisis: compliance with CPCB and SPCB discharge and reuse standards isn’t a paperwork formality. It’s a real operational and legal risk. Developers have seen occupancy certificates delayed over treatment plant compliance issues. Facility managers have had to explain to leadership why a routine inspection turned into a legal notice. Municipal planners have watched community trust erode after a poorly maintained system led to visible or reported violations.

A well-designed DEWATS system is built with these standards in mind from the outset, aiming to consistently deliver treated water quality that falls within the ranges expected for discharge or reuse under applicable municipal and pollution control board guidelines. But, and this is important, the design alone doesn’t guarantee ongoing compliance. Consistency comes from proper commissioning, periodic monitoring, and a maintenance routine that doesn’t get neglected once the initial excitement of the project fades.

This is also where choosing a credible manufacturer or design partner really matters. A system built by a team with a genuine track record in compliance-focused design, and one that offers structured monitoring support after installation, meaningfully reduces the risk of the kind of surprises that lead to legal liability or reputational damage down the line.

A quick but important note: any performance figures, treatment efficiency ranges, or capacity numbers referenced in discussions around DEWATS or centralized systems are general and indicative only. Actual outcomes vary considerably from one installation to another, depending on factors like influent load, site conditions, climate, and how consistently the system is maintained. Anyone evaluating a system for a specific project should treat broad ranges as a starting point for conversation, not a guarantee, and should work with their design partner to understand what’s realistic for their particular site.

Who Should Consider DEWATS

DEWATS systems tend to make the most sense for a fairly specific set of readers, and if you fall into one of these categories, it’s worth a closer look:

  • Real estate developers working on projects located away from established municipal sewage infrastructure, or building in phases where a scalable, on-site solution avoids upfront over-investment.
  • Campus and facility managers, schools, hospitals, corporate parks, who need a low-maintenance system that won’t demand a large dedicated technical team and can operate reliably even through power interruptions.
  • Municipal planners assessing options for townships or peri-urban developments where extending centralized sewage lines isn’t currently practical or cost-effective.
  • Rural and semi-urban project heads who need a treatment solution that’s rugged, low-tech in the right ways, and doesn’t fall apart the moment the local grid goes down.

If your project fits any of these profiles, a decentralized approach is worth serious evaluation rather than being treated as a fallback option only used when a centralized connection isn’t available.

What to Evaluate Before Choosing a DEWATS Provider

Not all DEWATS providers are equal, and the difference between a system that runs smoothly for years and one that becomes a recurring headache often comes down to who designed and built it. Before committing to a provider, it’s worth working through a short checklist:

  • Design experience across varied site conditions. Ask whether the provider has handled projects with similar land constraints, population sizes, and soil or terrain conditions to yours.
  • Compliance track record. Look for a provider who can speak knowledgeably and specifically about CPCB and SPCB requirements relevant to your region, not just generic assurances.
  • After-installation support. A system is only as reliable as the maintenance and monitoring behind it. Ask what ongoing support looks like, inspections, troubleshooting, and responsiveness when something needs attention.
  • Material and construction quality. Reactor chambers, filter media, and wetland bed construction all need to be built to last; ask about the materials and construction standards being used.
  • Site assessment approach. A provider who takes the time to properly assess your soil, water table, expected load, and layout before proposing a design is signaling that they’re not just selling a one-size-fits-all package.

This is an area where Team One Biotech has spent considerable time refining its approach, not because every project looks the same, but because every project doesn’t, and a design that ignores that tends to underperform.

Bringing It Together: Peace of Mind, Not Just a Treatment Plant

Going back to where we started, the stalled project, the compliance notice, the tanker trucks nobody wants rolling through the gate, the underlying thread across all of these situations is the same. A wastewater treatment decision isn’t just an engineering choice; it’s a decision about risk, reliability, and how much of your attention you want this system to demand over the years ahead.

A thoughtfully designed DEWATS system offers a path to sidestep a lot of that friction: no dependency on an uncertain municipal connection, a lower ongoing maintenance burden, and a design built with compliance in mind rather than as an afterthought. That doesn’t mean it’s the right fit for every project, but for scattered developments, campuses, townships, and rural or semi-urban sites, it’s very often the more practical answer.

If you’re currently weighing your options, whether you’re planning a new project, dealing with a compliance concern, or simply trying to figure out whether decentralized treatment makes sense for your site, schedule a site assessment with Team One Biotech. Our team can walk through your specific land, load, and compliance requirements and help you figure out what actually fits, rather than pushing a generic solution.

And if you’re not ready for a full consultation just yet, feel free to reach out for more detail on how our DEWATS systems are designed, or get in touch through our contact page to have an informal conversation about your project.

Frequently Asked Questions

What is the full form of DEWATS?

DEWATS stands for Decentralized Wastewater Treatment System, an approach to treating sewage on-site or close to its source, using low-energy, largely biological treatment stages instead of a centralized municipal plant.

Is DEWATS suitable for large housing societies, or only small sites?

DEWATS systems are flexible in scale. While they’re a natural fit for smaller or scattered developments, they can also be designed for larger housing societies and townships, particularly when a project is built out in phases or sits far from municipal sewage infrastructure.

Does a DEWATS system require electricity to run?

One of the defining features of DEWATS is that the core treatment stages, settling, anaerobic filtration, and root zone treatment, operate without a continuous electricity supply, relying instead on gravity flow and biological processes. Some ancillary components may use minimal power, but the system isn’t dependent on constant electricity to function.

How is compliance with CPCB/SPCB norms ensured in a decentralized system?

Compliance comes from a combination of sound initial design, proper commissioning, and consistent ongoing monitoring and maintenance. A well-designed DEWATS system aims to keep treated water quality within applicable discharge or reuse standards, but this needs to be paired with regular checks rather than assumed to be automatic.

What is the difference between root zone treatment and conventional STPs?

Root zone treatment relies on planted gravel beds and natural microbial activity to break down pollutants, with minimal mechanical equipment involved. Conventional STPs typically use mechanical aeration, pumps, and other electrically driven processes to achieve treatment, which generally means higher energy use and a greater maintenance burden.

Note: All figures, ranges, and comparisons discussed in this article are general and indicative only. Actual performance, costs, and design parameters vary from one installation to another depending on site-specific factors, and should be assessed individually with a qualified design partner.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!

Anaerobic Digestion in STP/ETP: Turning Waste into Wealth

Every month, industrial facilities across India receive electricity bills that eat into already-thin operating margins. Simultaneously, their ETP and STP units are quietly generating tonnes of organic sludge that must be dewatered, transported, and disposed of at significant cost. What if both problems shared the same solution? What if that sludge, widely treated as a liability, was actually an untapped energy asset sitting beneath your feet?

This is not a theoretical proposition. It is the commercial reality of anaerobic digestion (AD), a biological process that is reshaping how forward-thinking plant operators and sustainability managers in India look at wastewater treatment. The question is no longer whether AD works. The question is how long your facility can afford to ignore it.

What Is Anaerobic Digestion and Why Does It Matter to Indian Industry?

What Is Anaerobic Digestion and Why Does It Matter to Indian Industry?

The anaerobic digestion process is a series of microbial reactions that break down organic matter in the complete absence of oxygen, producing two commercially valuable outputs: biogas (primarily methane) and digestate (a nutrient-rich residue usable as fertilizer or soil conditioner).

In the Indian industrial context, this process carries outsized significance. Sectors such as distilleries, dairy processing, paper and pulp, pharmaceuticals, food and beverage, and municipal sewage treatment are all operating under tightening CPCB and SPCB compliance mandates. These regulations are not softening. The Central Pollution Control Board’s evolving discharge norms and the push toward Zero Liquid Discharge (ZLD) compliance are forcing plant operators to rethink sludge management from the ground up.

Meanwhile, the cost of grid electricity continues to climb, and industrial consumers in states like Maharashtra, Gujarat, Tamil Nadu, and Uttar Pradesh are acutely aware of how energy expenditure affects their cost per unit of production. Anaerobic digestion offers a pathway to reduce both the environmental liability of sludge and the financial burden of purchased energy, simultaneously.

The Four Biological Stages of the Anaerobic Digestion Process

The Four Biological Stages of the Anaerobic Digestion Process

Understanding how AD works at a microbial level is critical for operators who want to optimize performance rather than simply install a reactor and hope for results. The process unfolds in four distinct, interdependent stages.

Stage 1: Hydrolysis

The process begins with hydrolysis, where complex organic polymers including carbohydrates, proteins, and lipids are broken down into simpler soluble compounds such as sugars, amino acids, and fatty acids. Specialized hydrolytic bacteria secrete extracellular enzymes to catalyze this breakdown.

This stage is often the rate-limiting step in systems treating high-solid or complex industrial effluents. Indian textile or pharmaceutical ETPs, for instance, frequently encounter effluents with recalcitrant organics that resist rapid hydrolysis, making microbial selection and inoculation at this stage critically important.

Stage 2: Acidogenesis

The soluble products from hydrolysis are then fermented by acidogenic bacteria into volatile fatty acids (VFAs), alcohols, carbon dioxide, and hydrogen. This is the fastest stage in the sequence and produces an acidic intermediate environment.

Operational challenges arise when acidogenesis outpaces the subsequent stages, causing VFA accumulation and a drop in pH that can inhibit or completely crash the system. Managing this balance is one of the most common pain points in Indian industrial AD installations, particularly in distilleries and food processing plants where organic loads fluctuate significantly with production cycles.

Stage 3: Acetogenesis

Acetogenic bacteria convert the VFAs and alcohols from the previous stage into acetic acid, hydrogen, and carbon dioxide, the direct precursors for methane generation. This stage operates in close syntrophic partnership with methanogens. The relationship is exquisitely sensitive to hydrogen partial pressure, and any operational disruption, whether from toxic influent, sudden organic overload, or temperature variation, can break this partnership and suppress biogas output.

Stage 4: Methanogenesis

This is the stage that generates wealth. Methanogenic archaea, the most environmentally sensitive microorganisms in the entire consortium, convert acetic acid and hydrogen into methane (CH4) and carbon dioxide (CO2). The methane fraction in the resulting biogas typically ranges between 55% and 75%, depending on the substrate composition and reactor conditions.

Methanogens are slow-growing, obligate anaerobes. They are extraordinarily sensitive to oxygen intrusion, pH swings, ammonia toxicity, and the presence of heavy metals, all of which are common challenges in mixed industrial effluents across Indian manufacturing sectors.

This is precisely why microbial consortium quality is not an afterthought. It is the foundation of AD performance.

At Team One Biotech, our proprietary microbial cultures for Anaerobic Digestion are developed and tested specifically for the organic profiles common in Indian industrial wastewater. Whether your ETP is treating distillery spent wash, dairy whey permeate, or paper mill effluent, the right biological inoculant can dramatically accelerate startup, stabilize performance, and push biogas yields to the upper end of achievable ranges.

Consult with Team One Biotech today for a free biological assessment of your ETP/STP influent.

Turning the Process into Profit: The Three Pillars of Wealth Generation

Turning the Process into Profit: The Three Pillars of Wealth Generation

Pillar 1: Biogas Recovery and Energy Independence

The most immediate and quantifiable financial return from AD is the recovery of combustible biogas. This gas can be used directly in boilers to replace furnace oil or natural gas, fed into gas engines for combined heat and power (CHP) generation, or, in larger installations, upgraded to compressed biomethane for vehicle fuel or grid injection under the Sustainable Alternative Towards Affordable Transportation (SATAT) scheme.

For medium to large ETPs treating high-strength organic effluent, the energy recovered through biogas can offset a meaningful share of total plant energy consumption. The exact offset depends heavily on influent COD concentration, flow volume, reactor design, and operational consistency. Systems with stable, high-COD inputs and well-managed microbial populations consistently outperform those operating reactively.

The SATAT initiative, promoted by the Ministry of Petroleum and Natural Gas, provides Indian industry with a structured offtake channel for surplus biomethane, creating a genuine revenue stream from what was previously a waste output.

Pillar 2: Reduction in Sludge Handling and Disposal Costs

In conventional aerobic treatment, sludge generation is high and the costs associated with its dewatering, transportation, and disposal can constitute a substantial portion of the ETP operating budget. Anaerobic digestion significantly reduces volatile solids in the sludge stream, resulting in a lower sludge volume requiring final disposal.

The digestate that remains after AD is stabilized, odor-reduced, and in many cases suitable for agricultural land application as a soil amendment, subject to applicable state SPCB norms. This alone can convert a recurring disposal cost into a potential revenue stream or at minimum eliminate a logistics burden that many plant managers underestimate.

Pillar 3: Carbon Credits and ESG Positioning

India’s voluntary carbon market is maturing, and regulatory frameworks around carbon credits are gaining traction. Biogas plants that displace fossil fuels are eligible to generate Verified Carbon Units (VCUs) under recognized methodologies. For industries with aggressive ESG targets or those supplying to multinational buyers with Scope 3 emission requirements, this adds a non-trivial financial and reputational layer of value to an AD investment.

More immediately, demonstrating active energy recovery from wastewater is a powerful narrative for sustainability reporting, green financing applications, and environmental compliance submissions to state pollution control boards.

Addressing Real-World Challenges in Indian AD Installations

Addressing Real-World Challenges in Indian AD Installations

Indian industrial AD systems face a set of challenges that are distinct from those encountered in European or North American installations.

Fluctuating Organic Loads: Seasonal production variations in agro-based industries create wide swings in influent COD and flow, which stress microbial populations adapted to stable conditions. Robust biological seeding and real-time monitoring are essential buffers against this variability.

Temperature Variability: Unlike temperate climates, certain Indian regions experience extreme seasonal temperatures. Mesophilic AD reactors operating in the range of 30 degrees Celsius to 38 degrees Celsius generally perform well across most Indian geographies, but insulation and heating strategies remain important in northern states during winter months.

Inhibitory Compounds: Effluents from pharmaceutical, chemical, and textile sectors frequently contain compounds that are toxic to methanogens at certain concentrations. Pretreatment strategies and the use of inhibitor-tolerant microbial strains are essential in such applications.

Startup and Seeding: Many AD installations in India underperform not because of poor design but because of inadequate or mismatched biological inoculation during startup. A reactor seeded with the wrong microbial community or insufficient biomass will take months to reach design performance, costing operators in both lost biogas and treatment inconsistency.

Team One Biotech’s specialized bio-cultures for anaerobic systems are engineered to address precisely these conditions. Contact us for a plant-specific microbial consortium recommendation and startup protocol.

From Linear Waste to Circular Economy: The Strategic Shift

The traditional model of industrial wastewater management is fundamentally linear. Waste is generated, treated at cost, and discharged or disposed of. Every rupee spent on treatment is a pure operating expense with no return.

Anaerobic digestion fundamentally disrupts this logic. It inserts a value recovery loop into the treatment chain, converting an expense center into a partial revenue center. Organic waste becomes biogas. Biogas becomes electricity or fuel. Digestate becomes soil amendment. Carbon displacement becomes credits. A facility that once paid to manage its waste now extracts value from it at multiple points.

This is the circular economy in industrial practice, and it is not aspirational language. It is an engineering and financial architecture that Indian industry is increasingly positioned to adopt, given the regulatory tailwinds, energy pricing pressures, and the availability of proven biological solutions.

The shift requires commitment at the management level, technical expertise at the operational level, and the right biological foundation at the microbial level.

Team One Biotech works alongside plant engineers and sustainability teams to design, seed, and optimize anaerobic digestion systems tailored to your specific wastewater profile. Schedule a plant audit with our technical team and take the first step from waste liability to energy asset.

Disclaimer: All numerical values, performance metrics, percentage ranges, and yield estimates referenced in this article are general indicative figures based on published literature and industry experience. Actual biogas yields, COD reduction efficiencies, sludge reduction rates, and energy outputs will vary significantly depending on site-specific influent characteristics, reactor design, hydraulic and solid retention times, temperature conditions, microbial population health, and operational management practices. These figures should not be used for detailed engineering design or financial projections without a site-specific technical assessment.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!
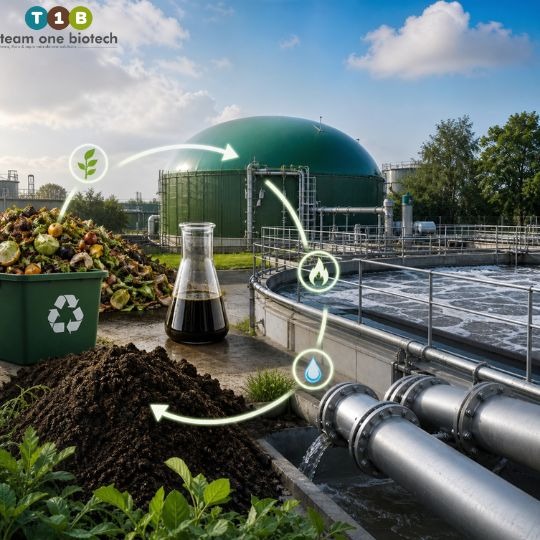
Biogas vs. Incineration: Which Is the Better Sludge Disposal Method for Indian ETPs?

Every ETP operator in India knows the feeling. The sludge pits are filling up faster than budgets can handle, the transporter just hiked his rates again, and the latest CPCB circular is sitting on the desk waiting to ruin the morning. Industrial sludge disposal has quietly become one of the most expensive and legally precarious problems in Indian manufacturing, and the traditional answer of “just haul it away” is running out of road.

Between tightening Hazardous Waste Management Rules, mounting pressure from State Pollution Control Boards, and the sheer logistics of managing high-moisture sludge in a land-scarce country, ETP operators are being pushed, often urgently, toward more sustainable, closed-loop disposal strategies. Two technologies are consistently at the center of that conversation: anaerobic digestion for biogas recovery and thermal incineration. Both promise volume reduction and regulatory compliance. But they deliver very different outcomes when you look at costs, carbon footprints, operational demands, and long-term value.

This is not a theoretical comparison. This is a ground-level evaluation for the conditions that actually exist in Indian ETPs.

The Sludge Crisis Quietly Reshaping Indian Industry

The Sludge Crisis Quietly Reshaping Indian Industry

India’s industrial expansion has been a remarkable story, but it has produced an equally remarkable volume of wet, chemically complex sludge. Textile clusters in Surat and Tiruppur, pharmaceutical corridors in Hyderabad and Ahmedabad, food processing belts in Punjab and Maharashtra, and tanneries in Vellore are all dealing with the same compounding problem: sludge generation is outpacing responsible disposal capacity.

The regulatory environment has changed fundamentally. The Hazardous Waste (Management, Handling and Transboundary Movement) Rules have become significantly more stringent. CPCB’s prescribed standards for landfill co-disposal and the increasing scrutiny on common treatment, storage, and disposal facilities (TSDFs) mean that the days of offloading sludge responsibility to a third-party contractor and forgetting about it are largely over.

Meanwhile, the Government of India’s “Waste to Wealth” mission under the Office of the Principal Scientific Adviser has created a formal policy framework encouraging industries to recover energy and materials from waste streams. Industrial sludge, long treated as a pure liability, is now recognized as a potential resource, if the right technology is applied.

This is the context in which the biogas versus incineration debate becomes genuinely important.

Understanding Your Two Primary Options

Understanding Your Two Primary Options

Biogas (Anaerobic Digestion): The Biological Route

Anaerobic digestion is the process of breaking down organic matter in the absence of oxygen using microbial communities. When applied to ETP sludge, the output is twofold: biogas (primarily methane, with a composition that typically ranges between 55% and 70% methane depending on feedstock quality) and digestate, a stabilized, nutrient-containing residue.

Why India’s conditions favor this technology:

India’s tropical and subtropical climate is a natural advantage for anaerobic digestion. Mesophilic digestion, the most commonly deployed mode, performs optimally in the temperature range that much of India maintains for the majority of the year without additional heating input. This translates directly into lower energy costs for maintaining digester temperature, which is one of the more significant OPEX items in colder climates.

Indian ETP sludge, particularly from food processing, dairy, distillery, and pharmaceutical sectors, tends to carry a high organic load. This is precisely the profile that anaerobic systems digest most efficiently. High volatile solids content means more biogas yield per unit of sludge processed.

Energy recovery and financial value:

The biogas generated can be used to run generators for captive power consumption, fuel boilers replacing furnace oil or LPG, or be upgraded to compressed biomethane for vehicle fuel. Across typical Indian ETP configurations, energy recovery from sludge biogas can fall between 30% and 50% of the theoretical energy equivalent, though this varies significantly by sludge composition and system design.

Industries that successfully close this loop report reductions in grid power consumption and fuel procurement costs that meaningfully improve their operational economics over a three-to-seven-year horizon.

The role of bioremediation in enhancing digestion:

This is where Team One Biotech’s core expertise becomes directly relevant. Raw ETP sludge often contains inhibitory compounds, residual disinfectants, heavy metals at trace concentrations, recalcitrant organics, that suppress the microbial populations responsible for digestion. Bioremediation solutions, specifically the application of specialized microbial consortia prior to or within the digestion stage, can measurably enhance volatile solids destruction rates and improve biogas yields. Pre-treatment with targeted bacterial inoculants has been shown across multiple case studies to reduce digestion cycle times and improve process stability in variable-feed industrial environments.

The digestate question:

The solid fraction remaining after digestion, the digestate, retains nutrients, primarily nitrogen and phosphorus. Depending on the industry and the regulatory classification of the sludge, this digestate may be eligible for use as a soil amendment, which represents an additional avoided cost compared to hazardous waste disposal. Not all sludge qualifies, and a site-specific characterization is essential before assuming this pathway.

Limitations to acknowledge:

Anaerobic digestion is not a fit for every sludge type. Sludge with very high inorganic content, significant heavy metal contamination (as in metal finishing or electroplating ETPs), or very low organic loading will produce marginal biogas yields. The technology also requires operator training, consistent monitoring, and a tolerance for biological variability.

Incineration: The Thermal Route

High-temperature incineration oxidizes sludge completely, destroying organic compounds and pathogens and reducing mass volume dramatically. For hazardous or highly toxic sludge profiles that cannot be biologically treated, it is often the only compliant option.

Where incineration makes clear sense:

  • Sludge from industries with persistent organic pollutants (POPs) or high halogenated compound content
  • Mixed hazardous waste streams where biological activity would be suppressed or unsafe
  • Situations demanding extremely rapid volume reduction where land is critically constrained

The economics are challenging:

Incinerators designed for sludge, particularly those meeting the emission norms specified under the Environment Protection Act and CPCB’s guidelines for hazardous waste incineration, are capital-intensive assets. CAPEX for a compliant industrial incinerator can range across a wide band depending on throughput capacity and pollution control equipment specifications. The OPEX picture is similarly demanding: auxiliary fuel is almost always required to sustain combustion temperatures when sludge moisture is high (which is the norm in Indian ETPs), and this represents a recurring operational cost that does not diminish over time.

Air quality and regulatory exposure:

India’s regulatory framework for incinerator emissions covers particulate matter, sulphur dioxide, nitrogen oxides, hydrogen chloride, heavy metals, and dioxins/furans. Compliance with these norms requires significant investment in air pollution control equipment, wet scrubbers, bag filters, secondary combustion chambers. Operating outside these norms creates substantial legal and reputational risk. This is not a theoretical concern; SPCB enforcement actions against non-compliant incinerators have been documented across multiple states.

Energy recovery is possible but limited:

Waste heat recovery from incineration is technically feasible and practiced at larger installations. However, energy recovery rates for wet sludge incineration are generally lower than those achievable through anaerobic digestion of equivalent organic-rich feedstocks, primarily because significant energy input is consumed in evaporating moisture before combustion can become self-sustaining.

Operational Factors: What Actually Matters on the Ground

Operational Factors: What Actually Matters on the Ground

FactorBiogas (AD)Incineration
Space requirementModerate (digesters can be underground or covered)Higher (combustion chamber, flue gas treatment, ash handling)
Operating expertiseMicrobiology and process monitoringHigh-temperature thermal operations, emission compliance
Sludge moisture sensitivityPerforms well with high-moisture sludgeHigh moisture requires auxiliary fuel, increasing OPEX
Residue managementDigestate (potentially reusable)Ash (requires classified disposal)
CPCB compliance complexityModerateHigh (continuous emission monitoring required)

For smaller and mid-sized ETPs, which constitute the majority of the Indian industrial base, the operational footprint and expertise requirement for incineration can be prohibitive without shared facility arrangements.

Economic Outlook: Thinking in Ranges, Not Promises

Economic Outlook: Thinking in Ranges, Not Promises

Responsible analysis resists the temptation to quote specific payback figures without knowing site conditions. That said, general patterns are observable:

Biogas systems at industrial ETPs with suitable organic sludge profiles have demonstrated payback periods that typically fall somewhere between four and eight years when energy savings, avoided disposal costs, and potential digestate value are modeled together. The range is wide because it depends enormously on current fuel prices, sludge volume, organic content, and whether the biogas is used for power, heat, or vehicle fuel.

Incineration as a standalone investment rarely generates positive financial returns in the traditional sense, it is a compliance cost management tool. The economic case rests on avoided liability, regulatory assurance, and the value of destroying material that cannot be treated any other way.

If your sludge profile is suitable for anaerobic digestion, the economic and environmental case for biogas over incineration is, in most Indian scenarios, substantially stronger.

Making the Right Decision for Your ETP

There is no universal answer, and any consultant or vendor who tells you otherwise is selling rather than advising. The right sludge disposal method is determined by sludge characterization, regulatory classification, existing infrastructure, available capital, and operational capacity.

What is clear is that Indian ETP operators who treat this decision as purely a compliance exercise will continue to face rising costs and tightening pressure. Those who approach it as a resource management decision have the opportunity to recover energy, reduce liability, and align with the direction that Indian environmental policy is clearly moving.

If you are at the point of evaluating sludge disposal options for your facility, the most valuable first step is a detailed site audit, one that characterizes your sludge properly, maps your regulatory obligations, and models realistic performance ranges for technologies applicable to your specific context.

Team One Biotech’s team of bioremediation and ETP specialists conducts exactly this kind of site-specific evaluation. If you would like a ground-level assessment of whether biogas recovery, enhanced biological treatment, or a hybrid approach fits your operation, reach out for an initial consultation. The conversation costs nothing; the wrong technology decision costs significantly more.

Disclaimer

All numerical ranges, performance estimates, payback period references, energy recovery figures, and operational comparisons presented in this article are general indicative estimates drawn from broad industry experience and publicly available studies. Actual results will vary, often significantly, based on individual ETP sludge characteristics, facility design, feedstock variability, equipment specifications, local regulatory requirements, energy tariff structures, and site-specific operational factors. No figures in this article should be treated as performance guarantees or used as the basis for investment decisions without a detailed, site-specific technical and financial assessment conducted by qualified professionals.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!
Textile vs. Chemical vs. Pharma ETP: How Biological Cultures Perform Differently

There is a particular kind of stress that EHS Managers know intimately. It arrives unannounced, sometimes on a Monday morning when the shift report shows a spike in COD discharge values, sometimes when an SPCB inspection notice lands on your desk with forty-eight hours’ notice. You have checked the equipment. The aerators are running. The settling tanks look normal to the eye. And yet something in your ETP is quietly failing, and you may not even know where to look.

The answer, more often than not, lives in the biology.

Every industrial effluent treatment plant runs on an invisible workforce: billions of microorganisms, bacteria, archaea, fungi, and protozoa, that consume, transform, and neutralize the toxic load your process generates. These organisms are not passive. They respond to temperature shifts, toxic shock, pH swings, and organic loading fluctuations with the sensitivity of a living ecosystem, because that is precisely what they are. When they are healthy and diverse, your ETP performs. When they are stressed, depleted, or mismatched to your specific effluent chemistry, your compliance numbers begin to drift.

What most plant operators do not realize is that the biological cultures optimized for treating textile dyeing effluent are fundamentally different from those that thrive in a pharmaceutical ETP, and both are different again from what works inside a chemical manufacturing treatment plant. Treating these as interchangeable is one of the most common and costly mistakes in Indian industrial effluent treatment.

This blog post is written for EHS Managers, Plant Heads, and Operations Engineers across pharma, textiles, chemicals, dairy, food processing, paper, and tannery sectors who need a clearer map of what is happening inside their biological systems, and what to do when it stops working.

Indian ETP Compliance Pressure

Indian ETP Compliance Pressure

India’s Central Pollution Control Board (CPCB) and the respective State Pollution Control Boards (SPCBs) have progressively tightened discharge norms under the Environment Protection Act and sector-specific effluent standards. Parameters like BOD, COD, Total Dissolved Solids (TDS), suspended solids, color, and specific toxic compounds are monitored with increasing frequency, and penalties for non-compliance have grown sharper.

Indian manufacturing hubs face a unique combination of challenges that global benchmarks do not fully account for:

  • Extreme seasonal temperature variation: Summer months in Gujarat, Rajasthan, and Maharashtra can push ambient temperatures above 42°C, accelerating microbial metabolism but also stressing sensitive cultures. Winter in Punjab and Himachal facilities can suppress biological activity dramatically.
  • Erratic power supply: Load shedding in Tier 2 and Tier 3 industrial areas causes aeration interruptions that can collapse aerobic biomass within hours.
  • Variable raw material sourcing: Production shifts mean influent chemistry changes batch to batch, making biological acclimatization a constant challenge.
  • Water scarcity and ZLD mandates: Many industrial clusters are now under Zero Liquid Discharge directives, placing enormous pressure on biological systems to perform at the front end of the treatment train.

Against this backdrop, understanding how your specific biological culture is behaving, and whether it is the right culture for your effluent, is not an academic exercise. It is an operational necessity.

Sector Breakdown: The Three Most Challenging Effluent Profiles

Textile ETP: The Problem of Refractory Dyes and High Color Load

Textile dyeing and processing units generate some of the most visually alarming and biologically challenging effluent in Indian industry. The Tirupur cluster in Tamil Nadu, the Surat textile belt, and the Bhilwara region in Rajasthan together represent massive discharge volumes that have defined the evolution of effluent treatment challenges in India.

What makes textile effluent uniquely difficult for biological cultures?

The core challenge is the presence of synthetic dyes, particularly azo dyes, reactive dyes, vat dyes, and disperse dyes, which are specifically engineered to resist degradation. That chemical stability is what makes them effective as colorants. It is also what makes them refractory, meaning resistant to conventional biological breakdown.

Standard activated sludge systems, populated with generic heterotrophic bacteria, will achieve reasonable BOD reduction in textile effluent but fail significantly on color removal and on degrading the aromatic amine compounds that azo dye cleavage produces. These intermediates are not just aesthetically problematic, several are classified as potentially mutagenic and are specifically flagged in CPCB discharge standards.

How specialized biological cultures approach textile effluent:

  • Sequential anaerobic-aerobic treatment is the established framework. Under anaerobic conditions, the azo bond in dye molecules can be reductively cleaved by specific anaerobic bacteria, breaking the chromophore. The aromatic amines released are then further oxidized under aerobic conditions.
  • Specialized facultative anaerobes and white-rot fungal cultures (where integrated) have demonstrated capacity to decolorize a broader spectrum of textile dyes.
  • Biomass health in textile ETPs is typically maintained at Mixed Liquor Suspended Solids (MLSS) levels in a range broadly between 2,500–4,000 mg/L in the aerobic zone, though optimal ranges depend on the specific SBR, MBBR, or conventional ASP design in use.

These are general values provided for guidance; actual parameters vary based on specific ETP design, influent characteristics, and local operational conditions.

Key operational stressors in textile ETPs include salt loading from reactive dye processes (which can osmotically stress microbial cells), pH fluctuations from alkali scouring steps, and temperature spikes from hot dyebath discharges.

If your textile ETP is consistently meeting BOD discharge norms but failing on color or showing rising COD trends, this is a strong signal that your biological culture profile needs reassessment. Team One Biotech’s microbial audit service can identify exactly which functional guilds are underrepresented in your biomass and recommend targeted bio-augmentation.

Chemical ETP: High COD, TDS, and the Inhibitory Cocktail

Chemical manufacturing, including dye intermediates, agrochemicals, specialty chemicals, and petrochemical derivatives, generates effluent that is simultaneously high in organic load, chemically diverse, and frequently toxic to the very microorganisms needed to treat it.

Plants across the Ankleshwar-Panoli cluster in Gujarat, the Navi Mumbai chemical belt, and the Hyderabad pharma-chemical corridor deal with effluent where a single batch change upstream can alter the COD profile by several thousand mg/L.

The defining characteristics of chemical ETP effluent:

  • Very high COD values, often driven by organic solvents, reaction byproducts, and unconverted raw materials
  • Elevated TDS from inorganic salts used in synthesis and process water
  • Presence of specific inhibitory compounds, surfactants, heavy metals (in some processes), halogenated organics, that can suppress microbial enzyme activity
  • Inconsistent BOD:COD ratio, which is a critical indicator of biodegradability; in chemical effluent this ratio is frequently low, indicating that a large fraction of the organic load is not readily bioavailable

Biological culture behavior in chemical ETPs:

Generic sludge inoculants, even when seeded from well-functioning municipal or food-processing ETPs, typically fail to establish stable performance in chemical effluent environments. The selective pressure of the toxic compounds eliminates sensitive organisms rapidly, leaving a depleted, functionally narrow community.

Specialized chemical-industry cultures, developed and adapted under controlled enrichment conditions, incorporate robust degraders of specific compound classes, aromatic hydrocarbons, halogenated solvents, nitrogenous organics, alongside organisms with elevated tolerance to osmotic stress and pH variability.

  • Anaerobic treatment stages in chemical ETPs typically target COD removal efficiency broadly in the range of 60–80% as a pre-treatment step, before aerobic polishing.
  • Dissolved Oxygen (DO) management in the aerobic stage is particularly critical, levels maintained broadly between 1.5–3.5 mg/L are commonly targeted in high-COD aerobic systems, though this varies by system design and organic loading.

These are general values provided for guidance; actual parameters vary based on specific ETP design, influent characteristics, and local operational conditions.

Shock loading, when a process upset sends an unusually high-strength batch to the ETP, is the single biggest threat to biological stability in chemical ETPs. Systems augmented with adapted cultures recover significantly faster from shock events than those relying on acclimatized generic sludge alone.

Pharmaceutical ETP: When Your Effluent Fights Back

Of the three sectors discussed here, pharmaceutical ETP management presents the most technically demanding biological challenge, and it is the one where the gap between compliance expectation and operational reality is most often felt.

The effluent from Active Pharmaceutical Ingredient (API) manufacturing, bulk drug synthesis, and formulation plants contains compounds that are, by design, biologically active, molecules engineered to interfere with cellular processes. When these reach an ETP, they do not conveniently deactivate. They inhibit microbial metabolism, disrupt nitrification, and in high concentrations can cause acute toxicity to the biological community.

What pharma ETP operators deal with daily:

  • Antibiotic residues that suppress or eliminate sensitive bacterial populations in the biomass
  • Solvent loads from extraction and purification steps, methanol, acetone, dichloromethane, ethyl acetate, each presenting different biodegradation kinetics
  • Fermentation broth residues from antibiotic and enzyme manufacturing, which are high in BOD but accompanied by inhibitory secondary metabolites
  • High nitrogen loads in fermentation-based processes requiring specific nitrification-denitrification biological stages

The role of specialized pharma-adapted cultures:

Conventional ETP biology often suffers from what engineers call “wash-out” in pharmaceutical systems, the inhibitory load selectively kills off the most sensitive functional groups, including the nitrifying bacteria responsible for ammonia removal, which are among the most inhibition-susceptible organisms in an ETP.

Pharma-adapted biological cultures are enriched specifically from environments where pharmaceutical compound exposure has driven natural selection toward tolerant strains. These cultures:

  • Maintain functional nitrification activity at antibiotic concentrations that would collapse standard nitrifier populations
  • Include organisms capable of co-metabolic degradation of specific API molecules
  • Are designed for staged introduction to allow gradual acclimatization rather than shock inoculation

MLSS targets in pharmaceutical aerobic systems are broadly maintained in ranges between 3,000–5,000 mg/L in high-load applications, with careful sludge retention time (SRT) management to protect slow-growing nitrifiers.

These are general values provided for guidance; actual parameters vary based on specific ETP design, influent characteristics, and local operational conditions.

For pharma plant operators managing CETP connections or independent ETPs, a biological culture audit before monsoon season, when dilution effects on influent change the loading profile, is a proactive step that consistently pays returns in compliance stability. Reach out to Team One Biotech to schedule a pre-monsoon microbial health assessment for your ETP.

The Biological Edge: Specialized Cultures vs. Generic Sludge

The Biological Edge: Specialized Cultures vs. Generic Sludge

The industrial effluent treatment sector in India has historically under-invested in biological intelligence. The equipment, aerators, clarifiers, filter presses, receives maintenance attention and capital budget. The biology is often treated as a self-sustaining background process that only gets attention when visible failure occurs.

This is the fundamental gap that bio-augmentation addresses.

What specialized cultures offer over generic activated sludge:

  • Functional diversity: Specialized consortia contain organisms selected for specific degradation tasks, color removal, COD reduction of refractory compounds, nitrification under inhibitory stress, rather than generic heterotrophic BOD removal
  • Shock resilience: Adapted cultures carry genetic machinery for stress response, including efflux pump systems and enzyme induction pathways that allow survival and recovery under transient toxic loading
  • Faster establishment: Seeding with specialized cultures reduces the biological start-up period from weeks to days in new ETPs or after catastrophic sludge loss events
  • Reduced sludge generation: Specialized degraders operating efficiently often produce lower excess sludge per unit COD removed, reducing disposal cost, a significant operational saving for large plants

Waste Characteristics Across the Three Sectors

ParameterTextile ETPChemical ETPPharmaceutical ETP
Primary PollutantsSynthetic dyes, auxiliaries, saltSolvents, organics, TDSAPI residues, solvents, fermentation byproducts
Key Biological ChallengeRefractory color, azo compoundsInhibitory organics, shock loadingAntibiotic inhibition, nitrification suppression
COD ProfileModerate to high, variableHigh to very highHigh, variable with batch production
BOD:COD RatioModerateLow to very lowLow to moderate
Best Biological ApproachAnaerobic-aerobic sequentialAdapted aerobic + anaerobic pre-treatmentPharma-adapted cultures, staged SRT management
Critical Indian Compliance ConcernColor, BOD, TDSCOD, TDS, specific organicsCOD, Ammonia-N, ecotoxicity
Seasonal VulnerabilityHigh (temperature, dilution)High (shock loading variation)Very High (nitrifier sensitivity)

Values and characterizations are indicative based on sector-wide trends. Individual plant profiles vary significantly.

A Roadmap to Compliance Peace of Mind

A Roadmap to Compliance Peace of Mind

Compliance peace of mind is not a product of better monitoring alone. Dashboards and sensors tell you what is happening; they do not fix the underlying biology that determines whether your ETP meets its discharge standards on a consistent, day-after-day basis.

The path forward for Indian EHS Managers and Plant Operators is clear:

  • Audit your biology, not just your equipment. A microbial community analysis tells you which functional groups are present, which are depleted, and what your biomass is actually capable of treating.
  • Match your culture to your effluent chemistry. Generic sludge is not a one-size-fits-all solution across textile, chemical, and pharmaceutical applications. The specificity of the biological challenge demands specificity in the biological solution.
  • Build resilience before a crisis. Bio-augmentation as a proactive measure, particularly before seasonal loading changes or production ramp-ups, is dramatically less costly than emergency intervention after a compliance breach.
  • Partner with specialists who understand Indian operational realities. Temperature variability, CPCB/SPCB specific norms, ZLD requirements, and the economics of Indian industrial operations require localized expertise, not generic global benchmarks.

Team One Biotech works with industrial facilities across pharma, textiles, chemicals, dairy, food processing, tannery, sugar, and paper sectors to deliver customized microbial consortia, bio-augmentation programs, and ongoing biological performance support. Whether you are commissioning a new ETP, recovering from a biological crash, or simply trying to move from reactive compliance to proactive stability, our team of environmental engineers and microbiologists is equipped to assess your specific situation.

Contact Team One Biotech today to schedule a customized microbial audit for your ETP. Because the most important part of your treatment plant is the part you cannot see, and understanding it is the first step to compliance you can count on.

Disclaimer: All numerical ranges provided in this article are general guidance values intended for educational purposes. Actual operational parameters depend on specific ETP design, influent characteristics, hydraulic and organic loading rates, local climatic conditions, and regulatory requirements. Consult a qualified environmental engineer before making changes to your ETP operations.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!
Food Processing Effluent Treatment: A Complete Guide for FSSAI and CPCB Compliance

When Compliance Becomes a Crisis: The Stakes Are Real

In March 2023, the Central Pollution Control Board issued closure notices to dozens of food processing units across Punjab and Uttar Pradesh for failing to meet discharge standards. These were not small, unregistered operations. Several had functional ETPs on paper. The problem was not always the absence of treatment infrastructure, it was the failure of that infrastructure to perform consistently under the actual organic load their processes generated.

If you are an EHS manager or plant director in the Indian food, dairy, sugar, or allied processing sector, you already understand the pressure. CPCB enforcement has grown significantly more rigorous in the post-COVID period. Simultaneously, FSSAI has made it explicitly clear that poor environmental hygiene, including inadequate effluent management, can trigger license reviews and public scrutiny. The regulatory environment is no longer forgiving of “we’re working on it.”

This guide exists to help you work through it, systematically, technically, and with a clear roadmap toward genuine compliance.

The Regulatory Landscape: CPCB, FSSAI, and the Space Between Them

The Regulatory Landscape: CPCB, FSSAI, and the Space Between Them

Many plant operators treat CPCB compliance and FSSAI compliance as two separate checklists. This is one of the most consequential mistakes in industrial environmental management in India.

CPCB discharge norms under the Environment (Protection) Act govern what leaves your ETP and enters the receiving water body or municipal drain. For food processing units, the General Standards for Discharge of Environmental Pollutants specify parameters including BOD (Biochemical Oxygen Demand), COD (Chemical Oxygen Demand), TSS (Total Suspended Solids), pH, and oil and grease.

FSSAI’s regulatory framework, while primarily focused on product safety and manufacturing hygiene, increasingly intersects with environmental standards. A facility that cannot demonstrate responsible wastewater management raises red flags during inspections, not just about environmental intent, but about overall process control discipline.

The synergy is this: a well-designed and consistently operated ETP demonstrates that your facility has the microbial control, process monitoring, and operational discipline that FSSAI auditors are also looking for inside your plant. Poorly treated effluent is often symptomatic of broader process hygiene failures, and regulators on both sides of the equation are beginning to recognize this connection.

Practical compliance benchmarks to be aware of:

  • BOD at discharge: General CPCB norms require levels below 30 mg/L for inland surface water discharge (site-specific standards may be stricter)
  • pH at discharge: Typically within the range of 6.5 to 8.5
  • TSS: Not exceeding 100 mg/L for most inland water bodies
  • Oil and grease: Within 10 mg/L for most categories

The values and metrics provided are general industry ranges; actual parameters and performance will vary based on specific ETP design and influent characteristics.

What You Are Actually Treating: Characteristics of Food Processing Effluent

The phrase “food processing wastewater treatment” covers an extraordinarily wide spectrum. Dairy wastewater behaves differently from sugar mill effluent. Meat processing effluent has different microbial profiles than beverage plant discharge. However, there are shared characteristics that define the challenge across sectors.

BOD and COD: The Organic Load Problem

Food processing effluent is, by nature, organically rich. Raw ingredients, cleaning chemicals, process wash-downs, and product losses all contribute to what arrives at your ETP inlet. BOD values in untreated food industry effluent commonly range from 500 mg/L to over 5,000 mg/L depending on the process. COD values can run even higher.

This is not comparable to domestic sewage or even many industrial effluents. A dairy plant processing large milk volumes, for instance, can generate influent with BOD concentrations that would overwhelm an ETP designed without accounting for seasonal milk fat content or CIP (Clean-in-Place) chemical loads.

TSS: The Suspended Solid Burden

Solid particles, from fine food material, cellulose, protein aggregates, and fat globules, add another dimension. High TSS not only violates discharge standards but chokes biological treatment systems, reducing their effectiveness exactly when you need it most.

FOG: Fats, Oils, and Grease

FOG is often underestimated until it causes a catastrophic failure in a biological treatment stage. Fat layers on aeration tanks, clogged diffusers, and inhibited microbial populations are common consequences of inadequate FOG pre-treatment. In a tropical climate like India’s, FOG can congeal rapidly in channels and pipes during cooler months, creating blockages that demand emergency intervention.

The Monsoon Variable

Indian ETPs face a challenge that most global treatment guides do not adequately address: the monsoon season. Hydraulic overloading during heavy rainfall, temperature fluctuation effects on microbial populations, and dilution of treatment chemicals all simultaneously impact performance from June through September. Any robust compliance strategy must account for this seasonal variability, not as an exception, but as a design parameter.

Traditional Chemical Treatment vs. Bioremediation: A Practical Comparison

Traditional Chemical Treatment vs. Bioremediation: A Practical Comparison

The Chemical Treatment Approach

Conventional food processing wastewater treatment has historically relied on coagulation-flocculation using chemicals like alum, ferric chloride, and lime. These are effective at reducing TSS and some BOD in primary stages. They are also relatively predictable in performance, when the chemistry is controlled.

The limitations, however, are significant:

  • High operational cost: Chemical procurement, dosing systems, and sludge disposal all carry recurring expenses that escalate with effluent volume
  • Sludge management burden: Chemical treatment generates considerable sludge that must be handled and disposed of in compliance with Hazardous Waste Management Rules
  • Incomplete BOD/COD reduction: Chemicals alone rarely bring high-strength food effluent to CPCB discharge standards without a robust biological stage
  • pH sensitivity: Incorrect dosing can create its own compliance problem at the discharge point

The Bioremediation Advantage

Bioremediation, specifically, the use of specialized microbial consortia engineered for high-strength organic effluent, addresses the limitations of purely chemical approaches. In food processing wastewater treatment, microbial solutions work by accelerating the natural biodegradation of organic compounds, using them as a carbon and energy source.

Well-formulated microbial products for food industry ETPs can achieve:

  • BOD reduction efficiencies in the range of 75% to 90% in biological treatment stages
  • COD reduction in the range of 60% to 85% under optimized conditions
  • Significant FOG degradation through lipase-producing microbial strains
  • Odor reduction through suppression of hydrogen sulfide-generating organisms

The advantage of bioremediation over chemicals is not just cost, it is specificity and adaptability. Microbial consortia can be selected and augmented based on the actual organic profile of your effluent. A dairy ETP and a sugar processing ETP have fundamentally different treatment needs. Tailored microbial solutions address those differences in a way that generic chemical dosing cannot.

The values and metrics provided are general industry ranges; actual parameters and performance will vary based on specific ETP design and influent characteristics.

Team One Biotech’s specialized microbial cultures are formulated specifically for the high-BOD, high-FOG effluent profiles common in Indian food processing operations. Contact us for a site assessment to determine which consortium is right for your process profile.

The Compliant ETP: Breaking Down Each Stage

The Compliant ETP: Breaking Down Each Stage

Primary Treatment

The goal here is physical separation. Screening removes large solids. A grease trap or dissolved air flotation (DAF) unit handles FOG. Equalization tanks buffer the flow and concentration variability before biological stages, critical for Indian operations where production scheduling often creates surge loads.

A well-designed primary stage protects your biological treatment from shock loading. Without it, even the best microbial consortium cannot perform consistently.

Secondary Treatment (Biological Stage)

This is where the real BOD and COD reduction happens. Options include:

  • Activated Sludge Process (ASP): Reliable for moderate to high-strength effluent when augmented with appropriate microbial cultures
  • Sequential Batch Reactors (SBR): Increasingly popular for space-constrained facilities; offers operational flexibility
  • Moving Bed Biofilm Reactors (MBBR): Suitable for high-strength effluent and expanding capacity without major civil work
  • Anaerobic treatment (UASB or anaerobic lagoons): Particularly effective for very high COD effluent from sugar and starch processing; generates biogas as a recoverable energy source

Microbial augmentation, adding concentrated, process-adapted bacterial cultures, is particularly impactful in the secondary stage. It helps establish robust biofilm communities faster, maintains treatment efficiency during monsoon temperature swings, and recovers system performance after upset events.

Tertiary Treatment

Tertiary stages polish the final effluent. Sand filtration, activated carbon adsorption, and UV or chlorine disinfection are commonly employed depending on the receiving water body and local discharge conditions. For zero liquid discharge (ZLD) mandated facilities, increasingly common in water-stressed areas of Rajasthan, Gujarat, and parts of Tamil Nadu, tertiary stages must be followed by evaporation or membrane-based concentration systems.

Building Your Compliance Roadmap: Practical Steps for EHS Managers

1. Conduct an honest influent characterization. Do not design or optimize treatment based on assumed values. Measure your actual BOD, COD, TSS, and FOG across shifts and seasons. Monsoon samples matter as much as peak production samples.

2. Audit your existing ETP design against your current production load. Facilities that have expanded production since their ETP was installed frequently find that their treatment capacity was never updated proportionally.

3. Evaluate your biological stage health. Mixed liquor suspended solids (MLSS), dissolved oxygen profiles, and sludge volume index (SVI) readings will tell you whether your microbial community is thriving or under stress.

4. Address FOG at the source. Pre-treatment of FOG-rich streams before they enter the main ETP is almost always more cost-effective than trying to manage FOG accumulation in biological stages.

5. Document everything. CPCB compliance is not just about what your ETP achieves, it is about demonstrating a consistent, monitored process. Online flow meters, daily logbooks, and third-party effluent testing records are your evidence of good faith.

6. Plan for upset recovery. Monsoon season, power failures, and production surges will all periodically stress your ETP. Having a protocol, and a supply of targeted microbial cultures for rapid bioaugmentation, is the difference between a temporary exceedance and a prolonged compliance failure.

Compliance Is Not a Destination, It Is an Operating Standard

The food processing sector in India is under a level of environmental scrutiny that will only intensify. CPCB’s online continuous effluent monitoring requirements for large units, combined with FSSAI’s increasing integration of environmental responsibility into its compliance framework, means that reactive ETP management is no longer a viable strategy.

The facilities that avoid closures, penalties, and reputational damage are those that have moved beyond compliance as a checkbox, toward genuine, technically grounded wastewater management that reflects the organic complexity of their actual processes.

Team One Biotech works with food, dairy, pharmaceutical, sugar, tannery, and paper industry facilities across India to design bioremediation programs that are matched to real operational conditions. Our microbial consortia are developed for Indian organic loads, Indian temperatures, and the variable demands of the Indian production calendar.

If you are ready to move from reactive to robust, reach out to Team One Biotech today. Our team offers confidential site audits, influent characterization support, and customized microbial culture recommendations, with no obligation beyond the conversation.

Your effluent compliance challenge has a technical solution. Let us help you find it.

Disclaimer: The values and metrics provided throughout this article are general industry ranges. Actual parameters, treatment efficiency, and regulatory thresholds will vary based on specific ETP design, influent characteristics, local CPCB notifications, and site-specific consent conditions. Always consult a qualified environmental engineer and your regional pollution control board for facility-specific guidance.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!
Paper and Pulp Effluent Treatment: How Biological Cultures Cut Colour and BOD

If you manage an ETP at a paper or pulp mill in India, you already know the feeling. The consent conditions sit on your desk. The CPCB ambient water quality norms have been tightened. Your State Pollution Control Board inspector is due next quarter, and the treated effluent flowing out of your clarifier still carries that unmistakable brown tint.

Paper mill effluent treatment is not a checkbox exercise anymore. In the current regulatory climate, with the National Green Tribunal actively penalizing non-compliant industrial units and SPCBs empowered to issue closure notices, the margin for error at your ETP is essentially zero. Real-time online monitoring systems (OCEMS) now transmit your treated effluent data directly to CPCB servers. There is no hiding a bad day at the plant.

The operators who are sleeping soundly at night are the ones who have moved beyond conventional treatment and invested in understanding the biology of their wastewater. This post explains exactly how Biological Cultures for Paper and Pulp Effluent Treatment are now doing what chemicals and physical processes alone never could: breaking down the stubborn organic load in paper and pulp effluent and delivering consistent compliance, month after month.

Why Paper Mill Effluent Is Among the Hardest Industrial Wastewaters to Treat

Why Paper Mill Effluent Is Among the Hardest Industrial Wastewaters to Treat

Before we discuss solutions, we need to respect the problem. Paper mill effluent treatment is uniquely challenging, and anyone who tells you otherwise is selling something oversimplified.

The core difficulty comes down to three factors:

1. Lignin-based colour is chemically recalcitrant

Lignin is the structural polymer that gives wood its rigidity. During the pulping process, whether kraft, sulphite, or mechanical, lignin is broken down and released in large quantities into the process water. The resulting effluent carries complex, high-molecular-weight chromophores that give paper mill discharge its characteristic dark brown to black colour.

These compounds do not respond well to conventional biological treatment because most common heterotrophic bacteria simply lack the enzymatic machinery to attack aromatic ring structures. Chlorine bleaching in older mills adds chlorinated lignin derivatives to the mix, further complicating biodegradation and potentially pushing you into the territory of acute aquatic toxicity.

2. High and variable Organic Loading Rates (OLR)

Paper mills do not produce uniform effluent. A mill running 100% recycled fibre will generate a different effluent profile than one using virgin wood pulp. OLR can swing dramatically based on:

  • Grade of paper being produced (tissue, kraft board, newsprint, writing paper)
  • Seasonal raw material variations
  • Machine wash-down cycles and felt changes
  • Chemical recovery system upsets

This variability is the enemy of a stable biological treatment system. A conventional activated sludge process tuned for average conditions will underperform on peak-load days, precisely the days when you can least afford it.

3. The BOD:COD ratio problem

Healthy aerobic digestion processes thrive on a favourable BOD:COD ratio. In paper mill effluent, the presence of non-biodegradable COD, principally from lignin and its derivatives, can push the BOD:COD ratio to values where standard microbial communities struggle to deliver meaningful COD removal. You can have perfectly functioning biomass and still fail your discharge norms because the recalcitrant fraction passes through untouched.

The Biological Solution: Bio-Augmentation for Lignin Degradation and BOD Reduction

The Biological Solution: Bio-Augmentation for Lignin Degradation and BOD Reduction

This is where the science becomes genuinely powerful, and where paper mill effluent treatment has seen the most significant advances in the last decade.

Bio-augmentation refers to the deliberate introduction of selected microbial strains or consortia into an existing biological treatment system. These are not generic cultures. For paper and pulp applications, the relevant organisms are typically:

  • White-rot fungi such as Phanerochaete chrysosporium and related basidiomycetes, which produce lignin peroxidase and manganese peroxidase, extracellular enzymes specifically evolved to depolymerise lignin
  • Laccase-producing bacteria including select Bacillus, Pseudomonas, and Streptomyces strains capable of oxidising phenolic compounds
  • Specialised heterotrophic consortia that efficiently convert the lower-molecular-weight fragments produced by the above into carbon dioxide and water through conventional aerobic metabolism

The process works in a cascade. Lignin peroxidase and laccase break the high-molecular-weight chromophores into smaller, more biodegradable units. Downstream heterotrophic bacteria then mineralise these fragments, reducing both colour and soluble BOD simultaneously.

What does this look like in practice?

When properly applied and acclimatised to your specific effluent, a well-designed bio-augmentation programme targeting paper mill wastewater can be expected to deliver:

  • BOD reduction in the range of 85% to 95%
  • COD reduction in the range of 70% to 88%
  • Colour reduction (ADMI units) in the range of 60% to 80%

Important Disclaimer: The numerical ranges cited in this article are general performance benchmarks drawn from field experience across multiple installations. Actual results will vary based on your specific ETP design, hydraulic retention time (HRT), sludge retention time (SRT), influent chemistry, temperature, and operational discipline. Contact Team One Biotech for a site-specific performance assessment before setting internal targets.

Paper Mill Effluent Treatment in the Indian Context: The Challenges Nobody Talks About

Paper Mill Effluent Treatment in the Indian Context: The Challenges Nobody Talks About

Global case studies are useful. Indian field realities are what matter when your phone rings at 2 AM because the final effluent is failing colour.

Seasonal temperature swings

Biological treatment systems are temperature-sensitive. In northern and central India, effluent temperatures in January can drop to 12°C to 16°C, dramatically slowing microbial metabolism. The same system in May may see influent temperatures exceeding 38°C to 42°C, stressing mesophilic organisms and risking process upset. A culture formulation that works in Maharashtra in February may behave very differently in Uttarakhand in December.

Effective bio-augmentation for Indian mills must account for this range. The microbial consortia supplied should demonstrate metabolic activity across a broad thermal window, and dosing protocols should be adjusted seasonally, not set once and forgotten.

Raw material and process variability in Indian mills

Many Indian paper mills operate on a mixed furnish, recycled OCC, agricultural residues like bagasse and wheat straw, and imported pulp. This creates an influent with a compositional complexity that European or North American mills rarely encounter. Bagasse-based effluents carry different hemicellulose fractions and silica loading than wood-based effluents. Your biological culture needs to be acclimated to your specific substrate chemistry, not a generic paper mill profile.

MLSS management under load shock

Maintaining Mixed Liquor Suspended Solids (MLSS) within the target range during production upsets is a persistent operational challenge. When a mill runs a grade change or recovers from a machine breakdown, the OLR spike that hits the aeration tank can crash a fragile biomass within 24 to 48 hours, setting back your compliance position by weeks.

Bio-augmented systems, particularly those using spore-forming bacterial strains, show significantly higher resilience to OLR shocks than conventional activated sludge alone. Dormant spores survive the upset and germinate rapidly once conditions stabilise, shortening recovery time considerably.

The push toward Zero Liquid Discharge

ZLD is no longer a future aspiration for many Indian paper mills, it is a regulatory condition of consent in several states. Biological pre-treatment quality directly determines the efficiency and cost of the downstream ZLD train (ultrafiltration, RO, MEE, and ATFD). Poor COD and colour removal at the biological stage means your RO membranes foul faster, your evaporator scaling increases, and your overall cost per kilolitre of recovered water rises sharply.

Investing in high-performance biological cultures is not just a compliance decision. In a ZLD framework, it is an operational cost management decision.

How Team One Biotech’s Biological Cultures Are Formulated for Paper Mill Applications

At Team One Biotech, our approach to paper mill effluent treatment begins with understanding that no two mills are identical. Our process:

Step 1, Influent characterisation. We analyse your raw effluent for BOD, COD, colour (ADMI), TSS, pH, TDS, sulphate, chloride, and the BOD:COD ratio. This tells us the biodegradable fraction we are working with and the recalcitrant COD we need to attack enzymatically.

Step 2, Culture selection and acclimation. Based on your effluent chemistry, we select and acclimate a consortium specifically prepared for your substrate. This is not an off-the-shelf product, it is a living, engineered microbial community tuned to your wastewater.

Step 3, Dosing protocol and integration. We provide a structured seed dosing protocol, typically delivered over a phased startup period of two to four weeks, followed by a maintenance dosing regime. Our technical team supports your plant operators through the process.

Step 4, Performance monitoring. We recommend a monitoring schedule targeting BOD, COD, MLSS, SVI, and colour at defined intervals through the startup phase to verify culture establishment and performance trajectory.

The result is a biological system that is more robust, more consistent, and better positioned to absorb the operational variability inherent in Indian paper mill production.

Practical Guidance for ETP Operators Running Paper Mill Wastewater

Practical Guidance for ETP Operators Running Paper Mill Wastewater

Whether or not you are currently using bio-augmentation, the following operational disciplines will strengthen any paper mill effluent treatment system:

  • Monitor your F/M ratio regularly. Food-to-microorganism ratio is your early warning system for biomass health. A declining F/M in the face of consistent loading often signals a culture quality issue before it becomes a compliance event.
  • Maintain dissolved oxygen in the aeration basin between 2.0 and 3.5 mg/L. Lignin-degrading organisms are obligate aerobes with high oxygen demand. Inadequate DO is the single most common reason bio-augmentation programmes underperform.
  • Track SVI (Sludge Volume Index) weekly. Bulking sludge is a frequent consequence of low F/M and poor selector design in paper mill ETPs. High SVI will compromise your secondary clarifier and push TSS into your final effluent.
  • Avoid sudden pH swings. Maintain aeration basin pH between 6.8 and 7.6. Paper mill effluents can be acidic or alkaline depending on the process stage contributing to the drain. Buffering capacity matters.
  • Document OLR trends. If you can predict the days your OLR spikes, grade changes, week-end startups, rainy-season dilution events, you can pre-dose your biological cultures to have elevated biomass activity ready before the shock arrives, rather than reacting after.

The Bottom Line for EHS Managers

Colour and BOD in paper mill effluent are not problems that chlorine dosing or coagulant overdosing will solve sustainably. They are fundamentally biological problems that require biological solutions, specifically, the right microbial consortia, properly acclimated, correctly integrated, and operationally supported.

With CPCB and SPCB enforcement intensifying and ZLD mandates expanding, the question is no longer whether to invest in biological treatment performance. The question is whether you are getting the best possible biological performance from your current system.

If you are not consistently achieving your consent conditions, or if you are achieving them on borrowed time through chemical patches, it is time for a professional audit of your ETP’s biological health.

Team One Biotech offers site-specific ETP audits and customised microbial culture formulations for paper and pulp mills across India. Our technical team works directly with your plant operators, not just your corporate procurement team, because we understand that compliance is won or lost at the plant floor level.

Reach out to Team One Biotech today to schedule your consultation. Bring your last three months of influent and effluent data, and we will bring the science.

This Blog is intended for informational purposes for ETP/STP operators and EHS professionals. All performance ranges cited are general benchmarks only and do not constitute guaranteed outcomes. Actual treatment performance is dependent on site-specific conditions including ETP design, hydraulic and sludge retention times, influent chemistry, temperature, and operational management. Team One Biotech recommends a site-specific technical assessment before implementing any biological treatment programme.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!
Tannery Wastewater Treatment: Removing Chromium and Sulfide with Bioremediation

If you manage environmental health and safety at a tannery unit in Kanpur, Ambur, or Ranipet, you already know what it feels like to walk into your ETP shed at 6 AM and wonder whether today is the day an SPCB inspection team shows up unannounced. You know the weight of being responsible for what goes into the drain, and what that means for a river downstream, for a community nearby, and for your facility’s operating license.

Bio Cultures for Tannery Wastewater Treatment is not a back-of-house problem. It sits at the intersection of industrial survival and environmental accountability. The leather industry contributes billions to India’s export economy and employs millions of workers, but it also produces one of the most chemically complex effluent streams in any industrial sector. Chromium. Sulfides. High BOD. Extreme pH swings. And CPCB norms that grow stricter with every revision of the Environmental Protection Act.

For EHS managers who have been navigating this pressure for years, the real question is no longer whether to treat, it is how to treat smarter, at lower cost, with less sludge, and with outcomes that actually hold up during third-party audits. That is where bioremediation is changing the conversation.

What Makes Tannery Effluent So Difficult to Treat

What Makes Tannery Effluent So Difficult to Treat

Before talking solutions, it helps to be honest about the problem, because too many vendors oversimplify it.

Traditional chrome tanning processes use trivalent chromium (Cr III) as a tanning agent. Under most ETP conditions, this is manageable. The challenge emerges when your ETP is not optimized: pH fluctuations, oxidizing conditions, and high redox potential can convert Cr(III) to hexavalent chromium (Cr VI), a compound classified as a carcinogen under multiple international standards and explicitly listed under CPCB’s hazardous waste rules.

Indian discharge norms for total chromium in tannery effluent are set at 2 mg/L for inland surface water discharge and 1 mg/L for land application under General Standards for Discharge of Environmental Pollutants (Schedule VI of the Environment Protection Rules, 1986). Facilities operating in river-sensitive zones, particularly those near the Ganga basin in Uttar Pradesh or Palar River basin in Tamil Nadu, face even tighter scrutiny under NGT directives and state-level notifications.

Then there is the sulfide problem. Beam-house operations, liming, de-hairing, and soaking, generate effluent with sulfide concentrations that can range from several hundred to well over a thousand mg/L, depending on process chemistry and hides processed per day. Sulfide in untreated or undertreated discharge creates toxic hydrogen sulfide gas, causes acute aquatic toxicity, and contributes to the foul odor conditions that draw community complaints and media attention to tannery clusters.

The conventional response has been chemical precipitation, adding ferrous sulfate or lime to crash chromium out of solution, and using aeration or chlorination to oxidize sulfide. These methods work, to a point. But they generate enormous volumes of chemical sludge, require significant reagent procurement and storage, and often struggle to consistently hit discharge limits when influent quality fluctuates, which in tanneries, it does frequently.

The Bioremediation Shift: Microbes That Work Where Chemicals Fall Short

Bioremediation in tannery wastewater treatment is not a new concept, but its practical implementation in Indian industrial ETPs has accelerated significantly in the last several years, driven partly by the push for ZLD compliance and partly by the economics of chemical sludge disposal.

What Team One Biotech brings to this domain is a library of specialized microbial consortia that have been selected and conditioned specifically for high-chromium, high-sulfide industrial environments. These are not off-the-shelf bacterial cultures from a generic microbiology catalogue. They are strains that have been adapted to perform under the high-salinity, high-toxicity conditions that are typical of tannery ETPs in the Kanpur cluster or the Ambur-Ranipet belt.

The core distinction between chemical treatment and bio-based treatment is what happens after the contaminant is captured. Chemical precipitation immobilizes chromium in a sludge cake that must then be landfilled or treated as hazardous waste. Bioremediation does something different, and, in many ways, more elegant.

How the Microbial Mechanism Actually Works

How the Microbial Mechanism Actually Works

Chromium Sequestration Through Microbial Reduction

Certain strains of chromate-reducing bacteria, including species from genera such as Bacillus, Pseudomonas, and Desulfovibrio, are capable of enzymatically reducing hexavalent chromium (Cr VI) to the far less toxic trivalent form (Cr III). This reduction typically occurs through electron transfer driven by organic carbon in the effluent, which means the bacteria are using the wastewater’s own chemistry as fuel.

Once reduced, Cr(III) can be further immobilized through biosorption, a process where microbial cell walls, with their negatively charged surface groups, bind to metal cations and remove them from solution. The result is chromium locked into a biomass matrix rather than floating in solution or leaching from a chemically unstable sludge cake.

In optimized bioaugmentation programs, total chromium reduction efficiencies in tannery ETPs have been reported in the range of 70% to 90% in the biological treatment stage alone, before any final polishing. Specific results depend on influent loading, hydraulic retention time, microbial acclimatization period, and the baseline performance of the existing ETP. These figures are benchmarks; actual outcomes vary from plant to plant and require site-specific evaluation.

Sulfide Oxidation Through Microbial Metabolism

The sulfide challenge is addressed through a different but equally elegant mechanism. Sulfur-oxidizing bacteria, which naturally thrive in environments rich in reduced sulfur compounds, convert sulfide (S²⁻) to elemental sulfur and ultimately to sulfate (SO₄²⁻), which is far less toxic and odorous.

In a bioaugmented ETP, this process is accelerated and stabilized compared to what happens in a conventional aeration system. The biological pathway does not require continuous addition of chemical oxidants, and it does not produce the chlorinated by-products associated with hypochlorite-based sulfide control.

Sulfide removal efficiencies in augmented biological treatment stages typically fall in the range of 75% to 92% under stable operating conditions. Again, these are generalized ranges. Actual performance depends on your specific influent sulfide load, reactor configuration, and dissolved oxygen management.

The Indian Industry Context: Why This Matters More Here

The Indian Industry Context: Why This Matters More Here

Indian tannery clusters operate at a scale that makes chemical reagent costs a serious line item. A mid-sized tannery processing 500 to 1,000 hides per day can spend significantly on ferrous sulfate, lime, and acid for pH adjustment alone, before accounting for the cost of sludge disposal, which in hazardous waste categories under the Hazardous and Other Wastes (Management and Transboundary Movement) Rules, 2016 requires authorized TSDF facilities.

Bioaugmentation does not eliminate chemical treatment entirely, most ETPs will continue to use some chemical precipitation for rapid chromium knockdown, but it substantially reduces reagent consumption and sludge volume. Facilities that have integrated microbial treatment into their process have reported reductions in chemical sludge generation in the range of 30% to 55%, though this varies considerably depending on baseline chemistry and process configuration. These figures are indicative and should not be assumed to apply universally without a proper site assessment.

From a ZLD compliance standpoint, reducing the contaminant load entering your RO or evaporation systems also extends membrane life and reduces scaling, which translates directly into lower maintenance costs and longer intervals between system overhauls.

For EHS managers under SPCB scrutiny or NGT compliance orders, particularly those operating in notified zones around the Ganga, Yamuna, or Palar river basins, demonstrating a biological treatment layer in your ETP is increasingly viewed favorably during compliance reviews as evidence of best-available-technology adoption.

If your facility is currently navigating a compliance notice or preparing for a renewal inspection, this is exactly the kind of documented process improvement that regulators want to see. Contact Team One Biotech for a no-obligation audit of your current ETP’s biological treatment potential.

Integrating Bioremediation Into Your Existing ETP: A Practical Path

Retrofitting an existing tannery ETP for bioaugmentation does not require demolishing what you have. The approach is additive, not disruptive. Here is how the implementation typically unfolds:

  • Baseline ETP Assessment, Team One Biotech’s technical team evaluates your current influent parameters: chromium speciation, sulfide load, BOD/COD ratio, pH profile, and sludge generation rates. This gives you a data-backed starting point rather than a guess.
  • Microbial Strain Selection, Based on the assessment, a specific consortium is recommended. High-chromium environments need strains with proven chromate-reduction capacity; high-sulfide environments need dominant sulfur oxidizers. The formulation is not one-size-fits-all.
  • Seeding and Acclimatization, Microbial cultures are introduced into your existing biological treatment tanks, typically the aeration tank or equalization basin. An acclimatization period of two to four weeks is standard before performance benchmarks are meaningful.
  • Monitoring and Optimization, Effluent quality is tracked at defined intervals. Dosing frequency and quantity are adjusted based on observed performance. This is not a one-time application; it is a managed biological process.
  • Documentation for Compliance, Treatment logs, influent and effluent data, and microbial performance records are maintained in a format suitable for SPCB submissions and third-party environmental audits.

Speak to Team One Biotech’s technical team today to understand whether your ETP’s existing infrastructure is ready for bioaugmentation, or what modifications might be needed to maximize outcomes.

Long-Term ROI and the Environmental Legacy You Leave Behind

The economics of bioremediation in tannery wastewater treatment improve over time. In the first year, the primary returns are in chemical savings, reduced sludge disposal costs, and improved consistency in hitting discharge limits. Over a three-to-five year horizon, the return also includes reduced equipment wear on downstream systems, lower compliance-related legal and administrative costs, and the reputational capital that comes with demonstrably responsible effluent management.

For tannery units in clusters like Kanpur, where the Ganga Action Plan and successive NGT orders have made the leather industry a focal point of environmental scrutiny, this is not a peripheral benefit. It is a strategic necessity.

The EHS managers who are building facilities that will still be operating a decade from now are not just chasing compliance thresholds. They are making a considered decision about the kind of industrial legacy their facility leaves in the local ecosystem, the local water table, and the communities around them.

Bioremediation is one of the most credible tools available to make that decision count.

To explore a site-specific bioremediation strategy for your tannery ETP, reach out to Team One Biotech for a detailed technical audit and customized treatment recommendation.

Disclaimer: All numerical values, reduction percentages, and concentration ranges cited in this article are general industry benchmarks compiled from published literature and field observations. Actual results vary from plant to plant and depend on influent characteristics, ETP design, operational parameters, and site-specific conditions. These figures should not be used as guaranteed performance indicators without a formal site assessment.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!
Sugar Mill Effluent Under Pressure: Biological Solutions for High-Load Shocks and CPCB Compliance

Every October, the same alarm starts ringing across sugar belt states,  Uttar Pradesh, Maharashtra, Karnataka, Tamil Nadu. The cane arrives faster than any ETP was designed to absorb. Clarifier overflow. Sludge turning grey. COD spiking to levels that would make an inspector reach for his clipboard before he even finishes his chai.

For an EHS manager standing between a 24-hour production cycle and an SPCB show-cause notice, this is not a theoretical problem. This is a recurring operational crisis,  one that can trigger NGT fines, plant shutdowns, and reputational damage that lingers long after the season ends.

The hidden cost of non-compliance is rarely just the penalty. It is the productivity loss during corrective shutdowns, the cost of emergency chemical dosing, the overtime hours troubleshooting a biological system that was never built for the load it is receiving. And increasingly, with CPCB tightening effluent discharge standards under the Environment Protection Act and NGT maintaining active oversight on Red Category industries, the margin for error has narrowed to almost nothing.

Biological treatment for sugar mills done right is not a backup plan. It is the foundation of a compliant, resilient sugar mill operation.

What Makes Sugar Mill Effluent a Biological Treatment Challenge

Sugar mill effluent is not ordinary wastewater. It is a concentrated, chemically complex mix that includes washings from cane preparation, barometric condenser water, juice spillage, molasses residues, and floor washdowns from the boiling house. During peak crushing, this mix arrives in volumes and concentrations that fluctuate dramatically,  sometimes hour to hour.

The core parameters that drive treatment difficulty:

COD loads typically range from 2,000–15,000 mg/L depending on the unit operation and dilution, though values outside this range are documented during startup and peak throughput.

BOD values commonly fall in the 800–6,000 mg/L range in raw influent, with significant variation tied to molasses carryover and process leakages.

pH swings across 4.5–9.5 in untreated streams, driven by fermentation of residual sugars in collection channels and alkaline process water from sulphitation.

Suspended solids, including bagasse fines and soil from cane washing, regularly read between 500–3,000 mg/L in raw streams entering primary treatment.

Colour, primarily from melanoidins,  the compounds formed when amino acids react with reducing sugars under heat,  is one of the most persistent treatment challenges and a visible indicator of non-compliance even when COD numbers look acceptable.

All values expressed throughout this article represent general industry ranges. Actual figures vary significantly based on plant-specific machinery, cane variety, feedstock quality, process water management, and ETP/STP design configuration. Site-specific characterisation is essential before any treatment design decision.

The Science Behind Biological Degradation of Sugar Mill Wastewater

The Science Behind Biological Degradation of Sugar Mill Wastewater

Why Microbial Consortia Outperform Chemical Treatment Alone

Chemical treatment,  coagulation, flocculation, lime dosing,  addresses the physical load. It does not address the dissolved organic fraction that drives your COD reading and determines whether your discharge will pass consent conditions.

That work is done by microorganisms. Specifically, by diverse consortia of aerobic heterotrophs, facultative anaerobes, and specialised fermenters that collectively degrade the complex organic matrix of sugar mill effluent.

The primary substrates these organisms are breaking down include:

Sucrose, glucose, and fructose,  rapidly consumed fermentable sugars that provide a fast-acting BOD spike in the early stages of biological treatment.

Polysaccharides and starches,  from bagasse and cane pith, which require cellulolytic and amylolytic bacterial populations to hydrolyse before further degradation is possible.

Organic acids,  acetic, lactic, and butyric acids formed during fermentation of residual sugars in collection sumps and anaerobic pockets of the treatment system.

Melanoidins,  high-molecular-weight recalcitrant compounds requiring specialised peroxidase-producing fungi and bacteria, such as Phanerochaete-type organisms or ligninolytic populations, that many generic microbial seed cultures simply do not contain in sufficient density.

The Anaerobic-Aerobic Sequence: Getting the Biology Right

Well-designed biological treatment of sugar mill effluent typically follows a staged approach:

Anaerobic pretreatment,  UASB reactors or anaerobic lagoons reduce the gross organic load, converting 55–70% of incoming COD to biogas and reducing the aerobic stage loading. COD reduction across the anaerobic stage typically falls in the 50–65% range.

Aerobic biological treatment,  Extended aeration, activated sludge, or sequencing batch reactors (SBRs) handle the residual BOD and COD. Well-seeded and maintained aerobic systems achieve BOD reductions of 88–96% across the combined treatment train.

Tertiary polishing,  Filtration, constructed wetlands, or advanced oxidation handles colour and residual suspended solids before ZLD or discharge.

The biology only performs at this level when the microbial population is correctly seeded, adequately fed, and protected from shock events.

Where Operations Go Wrong, The Most Common ETP Failures in Sugar Mills

Sludge Bulking and Settleability Collapse

One of the most frequently reported operational failures in sugar mill ETPs is filamentous sludge bulking,  the proliferation of thread-like bacterial species that create a voluminous, poorly settling sludge blanket. This typically occurs when:

Carbon-to-nitrogen ratios are skewed by high sugar loads without proportional nitrogen supplementation. The ideal C:N:P ratio for aerobic biological treatment is approximately 100:5:1, but in sugar mill systems, this ratio can be thrown to 300:5:1 or worse during high-load periods.

Dissolved oxygen sags below 1.5–2.0 mg/L in aeration tanks during peak load, favouring filamentous organisms over floc-forming bacteria.

Hydraulic retention times are shortened during peak production to maintain inlet flow acceptance, starving the biological population of contact time.

The Failure of Generic Microbial Seeding

This is a pattern that repeats across sugar mills that are attempting biological recovery without specialist input. The plant inoculates with cow dung slurry or municipal sludge,  standard practice passed down through operating teams,  and then waits for the biomass to establish.

The problem is selection pressure. The microbial populations in generic seed material were never exposed to the specific substrates in sugar mill effluent,  melanoidins, complex polysaccharides, high-temperature process water. Establishment is slow, COD reduction remains in the 40–60% range instead of the 85–95% range a specialist consortium can achieve, and the plant operates in a perpetual state of marginal compliance.

Monsoon-Season Biomass Instability

Monsoon creates specific problems for sugar mill ETPs in India that are rarely addressed in treatment design documents but are felt acutely by every plant operator.

Temperature drops across aerobic tanks of 8–14°C relative to pre-monsoon conditions can reduce microbial metabolic rates by 30–50%, stretching biological treatment response times and elevating discharge COD.

Stormwater ingress dilutes mixed liquor suspended solids (MLSS),  the active biological mass,  from stable operating ranges of 2,500–4,000 mg/L down to values below 1,000 mg/L in poorly bunded facilities.

Additionally, the crushing season in northern states begins immediately post-monsoon, meaning biomass is already stressed before it faces the season’s peak organic shock.

Regulatory Pressure and ZLD,  What CPCB and NGT Are Actually Demanding

Regulatory Pressure and ZLD,  What CPCB and NGT Are Actually Demanding

Under CPCB’s effluent standards for sugar industries and the downstream pressure from NGT judgments on critically polluted areas, many large sugar mills are now operating under consent conditions that require discharge COD below 250 mg/L,  and in some states, below 150 mg/L,  into inland surface water bodies.

ZLD aspirations are growing. Several state pollution control boards have begun mandating ZLD compliance for sugar mills in water-stressed districts of Maharashtra, Rajasthan, and parts of Uttar Pradesh. ZLD shifts the entire treatment objective from effluent quality to volume reduction, a target that cannot be achieved without a stable, high-performing biological treatment stage at the base of the system.

For EHS managers preparing for SPCB renewals or NGT submissions, the biological treatment performance records , MLSS logs, SV30 data, effluent quality trends,  are no longer optional documentation. They are evidence.

Download Team One Biotech’s ETP Health Checklist for Sugar Mills,  a field-tested audit framework covering biological performance indicators, sludge management, and CPCB compliance documentation.

The Team One Biotech Approach,  Specialised Biology for Specialised Loads

Team One Biotech works with sugar mills not as a chemical supplier, but as a biological treatment partner. The difference is in the specificity of the microbial products and the depth of the technical support behind them.

The core of the approach involves:

Strain-selected microbial consortia formulated specifically for high-sucrose, melanoidin-heavy wastewater streams. These are not general-purpose cultures,  they carry cellulolytic, lipolytic, and ligninolytic populations capable of degrading the recalcitrant organic fraction that generic seed material misses.

Nutrient balancing protocols that accompany every dosing plan, addressing the N:P deficiencies that are almost universal in sugar mill treatment systems.

Biomass protection strategies ahead of the crushing season,  a pre-seeding programme that builds MLSS levels and microbial diversity before the high-load shock arrives, rather than attempting biological recovery in the middle of peak production.

Ongoing monitoring support across aerobic and anaerobic stages, with dosing adjustments tied to incoming load data rather than fixed schedules.

Team One Biotech’s product range spans industrial wastewater treatment, agricultural soil health, and aquaculture water quality,  a breadth of biological expertise that brings cross-sector learning into every site-specific solution.

Request a site audit from Team One Biotech’s technical team,  field diagnostics, effluent characterisation, and a biological treatment gap analysis built around your plant’s specific operational profile.

Moving From Firefighting to Forward Management

The sugar mill operations that achieve consistent CPCB compliance and are positioned for ZLD mandates are not necessarily those with the most capital-intensive infrastructure. They are the ones whose biological treatment is actively managed,  seeded correctly at the start of the crushing season, supported through monsoon transition, monitored through the season’s peak loads, and backed by a technical partner who understands the difference between sugar mill effluent and generic industrial wastewater.

The shift from reactive crisis management to proactive biological stability is not a technology upgrade. It is an operational philosophy, supported by the right microbial science.

Sugar mill effluent treatment has a biological solution. The season does not have to be a crisis every year.

Contact Team One Biotech today for a customised microbial dosage plan built around your mill’s effluent profile, crushing schedule, and compliance targets. Treatment that works with your biology, not against your operational calendar.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!

Scan the code