SPCB Show-Cause Notice for Your STP? A 30-Day Response Framework

You know the feeling. The email lands, or the courier hands over the envelope, and your stomach drops. A show-cause notice. Your mind jumps straight to the worst outcomes: power or water disconnection, action on your bank guarantee, a direction of closure, and a very uncomfortable conversation with residents, tenants, or management.

Take a breath. A notice is serious, but it isn’t the end of the road. A show-cause notice is a formal request from your State Pollution Control Board (SPCB) asking you to explain, in writing, why action shouldn’t be taken for non-compliance. It sits within the powers the board holds under Section 33A of the Water (Prevention and Control of Pollution) Act, 1974. In general terms, that includes issuing directions, including closure and the stoppage or regulation of electricity or water supply.

This guide gives you a clear, week-by-week plan to fix what’s failing and build a strong SPCB show cause notice reply. It’s a general compliance framework, so please involve your legal or compliance team from day one.

The 30-Day Roadmap at a Glance
The 30-Day Roadmap at a Glance

WeekGoalKey Output
Week 1 (Days 1 to 7)Stabilize and investigateNotice analysis, root-cause findings, stabilized operations
Week 2 (Days 8 to 14)Restore biological performanceBioaugmentation plan, daily monitoring records
Week 3 (Days 15 to 21)Verify with dataNABL-accredited lab reports, organized documentation
Week 4 (Days 22 to 30)Draft and fileEvidence-backed reply, proof of submission

These are general values. Actual figures differ for every STP and ETP based on design, load, and site conditions.

What an SPCB Show-Cause Notice for an STP Really Means
What an SPCB Show-Cause Notice for an STP Really Means

A notice rarely comes out of nowhere. Usually, something triggered it: a routine inspection, a sampling visit, a complaint from neighbors, or lab results that showed your treated effluent didn’t meet the prescribed standards. This is what we call STP effluent non-compliance.

The parameters most often flagged are BOD (biochemical oxygen demand, the amount of oxygen microbes need to break down organic matter), COD (chemical oxygen demand, a broader measure of pollutants), TSS (total suspended solids), and FOG (fats, oils, and grease). Sometimes pH, ammoniacal nitrogen, and coliform counts appear too. Your treated water is measured against CPCB discharge norms and any specific limits your SPCB has set for your site.

Is a pollution board notice ETP different from an STP notice?

Not in the way that matters. Whether it’s a pollution board notice ETP (effluent treatment plant, usually industrial) or one for an STP (sewage treatment plant, usually residential or commercial), the logic is the same. The board has found a gap between what your plant discharges and what it’s supposed to discharge, and it wants a written explanation and a fix.

Show-cause notice vs. direction of closure

Think of it as an escalation path. A show-cause notice is the board asking you to explain. If the explanation or the corrective action isn’t convincing, the next step can be a formal direction, which may include closure and stoppage or regulation of power or water supply. A direction of closure for an STP is the stage you want to avoid, and this is exactly why your first response matters.

Possible consequences, if things escalate:

  • Environmental compensation or penalties
  • Action on the bank guarantee
  • Stoppage or regulation of electricity or water supply
  • A direction of closure
  • Reputational damage with residents, tenants, customers, and regulators

Received a notice today? Speak to a Team One Biotech compliance expert before your timeline runs out.

Week 1 (Days 1 to 7): Stabilize and Investigate
Week 1 (Days 1 to 7): Stabilize and Investigate

The first week is about two things: understanding exactly what the board is saying, and finding out why your plant failed. Don’t skip straight to fixes. A fix without a diagnosis is just a guess.

Read the notice line by line

Sit down with the document and highlight everything. Note the reply deadline, the parameters cited, the sampling dates, the sampling location, and exactly what the board is asking you to submit. Missing a small detail here can cost you later.

Assemble your response team

You need the right people in the room early:

  • Your plant operator, who knows the daily reality
  • The EHS head or facility director
  • Your legal or compliance team
  • An external microbial or process expert who can look at the plant with fresh eyes

Run a root-cause audit

This is the heart of the first week. A proper root cause analysis for your STP looks at what changed before the failure. Ask these questions:

  • Did the inflow load or flow pattern change, perhaps from new occupancy, a new kitchen, or a seasonal shift?
  • Did aeration fail or weaken? Check blowers, diffusers, and dissolved oxygen levels.
  • Is sludge age off, or has sludge built up or been wasted too aggressively?
  • Is there short-circuiting in tanks, so that water isn’t getting its full treatment time?
  • Were there chemical dosing errors?
  • Is FOG overloading the system from kitchens, canteens, or food outlets?

Don’t forget equipment health. Pumps, blowers, diffusers, and clarifier mechanisms all need an honest inspection.

Start immediate stabilization

You don’t need to wait for the full audit to stop the bleeding. Keep the steps general and safe:

  • Balance the inflow load with an equalization tank where available
  • Correct aeration so the biology gets the oxygen it needs
  • Manage sludge by removing excess and avoiding carryover
  • Control FOG at the source with grease traps and cleaning schedules
  • Fix obvious mechanical faults right away

Document everything you do and when you do it. This record becomes part of your reply later.

Week 2 (Days 8 to 14): Biological Recovery with Fast-Track Bioaugmentation
Week 2 (Days 8 to 14): Biological Recovery with Fast-Track Bioaugmentation

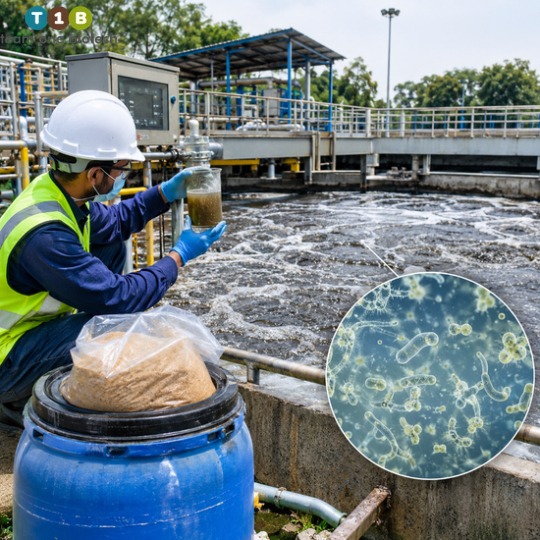
Here’s the plain truth about most STP failures. The machinery is usually fine. The microbes are struggling.

Your plant depends on a living microbial population to break down pollutants. When that population is shocked by a toxic load, starved of oxygen, or simply outnumbered, treatment performance collapses. BOD, COD, TSS, and FOG numbers drift out of limits, and a notice follows.

What bioaugmentation actually does

Bioaugmentation for STP means introducing selected, high-performing microbial cultures into the treatment system to strengthen or rebuild the working population. Microbial re-seeding is closely related. It restores the biology after a shock event, a shutdown, or a major washout. Done properly, these approaches help the system recover its ability to degrade organic load, reduce suspended solids, and break down grease.

How a structured program works

A credible program isn’t a bucket of powder tossed into a tank. It typically follows a clear sequence:

  • Baseline testing. Measure current performance and understand the inflow characteristics.
  • Tailored strain selection. Choose microbial cultures that suit your wastewater, whether it’s high in grease, high in organic load, or nitrogen-heavy.
  • Dosing schedule. Apply cultures at planned intervals, usually over a period of a few days to a couple of weeks depending on conditions.
  • Monitoring. Track parameters regularly and adjust the program based on what the data shows.

Many plants begin to see measurable improvement within a window of a few days to a few weeks, but this varies widely.

These are general values. Actual figures differ for every STP and ETP based on design, load, and site conditions.

At Team One Biotech, this is what we do every day as a provider of bioremediation solutions in India. We work with plant teams to design a recovery plan around their specific wastewater, not a generic one. You can explore our bioaugmentation for STP range and our wider effluent treatment solutions for both STP and ETP effluent treatment.

Need a fast-track bioaugmentation plan for your STP? Request a free effluent assessment, Contact a free assessment from Team One Biotech.

What to monitor daily

  • Dissolved oxygen in the aeration tank
  • pH of the incoming and treated water
  • Visual checks: color, odor, foam, and sludge settling
  • Sludge volume and settling behavior
  • Treated water clarity at the outlet
  • Equipment running hours and any faults

For deeper guidance on the numbers themselves, see our related blog on how to reduce BOD and COD in your STP.

Week 3 (Days 15 to 21): Verify with Data and Document Everything

By now your plant should be responding. But the board won’t take your word for it, and honestly, you shouldn’t take your own either. This week is about proof.

Collect samples at defined points, typically the inlet, the aeration tank, and the final outlet. Send them to a NABL-accredited laboratory. NABL stands for the National Accreditation Board for Testing and Calibration Laboratories, and accreditation tells the reader that the lab follows recognized testing standards.

Why does this matter so much? Because in-house readings, however careful, are easy to question. A third-party certified report carries independent weight. It tells the board you’ve measured honestly and that you’re serious about compliance.

Compare your results against the limits that apply to you, meaning the CPCB norms and the specific limits stated in your SPCB notice or consent conditions. Always treat your SPCB’s stated limits as the final reference.

Keep these documents ready:

  • NABL lab reports with sampling dates and locations
  • Operator logbooks and daily operating data
  • Dosing records for any bioaugmentation or chemicals
  • Calibration records for meters and instruments
  • Dated photographs of equipment, repairs, and the plant
  • Maintenance records and work orders
  • Any correspondence with the board

If your results show improvement but sit close to the limit, don’t panic. Plants often need a few more days to a couple of weeks to settle into steady performance after biological recovery.

These are general values. Actual figures differ for every STP and ETP based on design, load, and site conditions.

Want a second pair of eyes on your reply and lab data? Share your notice and parameters with our team. We’ll tell you honestly where you stand.

Week 4 (Days 22 to 30): Draft and File a Strong SPCB Show Cause Notice Reply

This is where all your work turns into a document the board will actually read. A strong SPCB show cause notice reply doesn’t need to be long. It needs to be clear, honest, and backed by evidence.

What a credible show cause reply contains

  • Acknowledgment. Confirm receipt of the notice and its reference details.
  • Root cause. State plainly what went wrong, based on your audit.
  • Corrective actions taken. List what you did, with dates.
  • Verifiable lab evidence. Attach your NABL-accredited reports.
  • An engineering compliance timeline. Share a realistic schedule for any remaining work. This is your STP compliance action plan.
  • A preventive maintenance plan. Show how you’ll keep the plant stable going forward.

Tone matters

Keep it factual, respectful, and evidence-led. Don’t make excuses. Don’t blame the board, the contractor, or the residents. Boards respond far better to accountability than to defensiveness. Own the problem, show the fix, and demonstrate the plan.

Submit properly

File within the deadline stated in the notice. Keep proof of submission, whether that’s a stamped copy, a courier receipt, or an email acknowledgment. If your situation calls for it, consider requesting a re-inspection or a hearing so the board can see the improvements for itself. Your legal or compliance team should guide this step.

Before you hit send

  • Does the reply address every point raised in the notice?
  • Are all lab reports attached, legible, and dated?
  • Do the numbers in your text match the lab reports exactly?
  • Is the timeline realistic and not overpromised?
  • Has your legal or compliance team reviewed it?
  • Have you kept a complete copy and proof of submission?

Common Mistakes That Weaken Your Show Cause Reply

After seeing plants go through this process, certain patterns show up again and again. Avoid these:

  • Waiting too long to act. Every day spent hoping the problem goes away is a day lost from your response window.
  • Relying on in-house readings only. Without independent lab proof, your claims are easy to dismiss.
  • Ignoring root causes. If you treat only the symptom, the failure will come back.
  • Submitting without lab evidence. A reply with no data is just a promise.
  • Overpromising timelines. A deadline you can’t meet damages your credibility more than a realistic, longer one.
  • Treating a quick fix as a permanent fix. A short-term improvement isn’t the same as sustained compliance. Plan for the long run.

Frequently Asked Questions

How long do I have to reply to an SPCB show-cause notice?

The deadline is stated in the notice itself, and it varies from one board and one case to another. Many notices allow somewhere from a few days to a few weeks. Always follow the exact timeline in your notice. If you need more time, speak to your legal team about requesting an extension in writing before the deadline passes.

Can bioaugmentation help bring my STP within limits quickly?

It can help, especially when the root cause is a weakened or shocked microbial population. Many plants see early improvement within a few days to a few weeks. However, results depend on your design, load, and site conditions, and bioaugmentation works best alongside proper mechanical and operational fixes. It supports compliance but doesn’t guarantee a specific outcome.

Do I need a NABL-accredited lab report for my reply?

It’s strongly advisable. Independent, accredited lab results make your reply far more credible than in-house readings. Check your notice and consent conditions for any specific laboratory requirements, and follow what your SPCB asks.

What happens if my STP still fails after the reply?

The board may review your reply, order a re-inspection, ask for further action, or escalate to formal directions under its powers, which in general terms can include closure or stoppage or regulation of utilities. This is why genuine corrective action and clear lab evidence matter. Involve your legal or compliance team and keep the board informed of your progress.

Do Not Let a Notice Become a Closure

Here’s the 30-day framework in a nutshell. Stabilize and investigate in week one. Rebuild your plant’s biology in week two. Prove it with accredited data in week three. File a clear, honest, evidence-backed SPCB show cause notice reply in week four.

A notice feels like a verdict, but it’s really a deadline with a path through it. Plants that act early, document well, and respond with humility give themselves the strongest possible case. You don’t have to figure it out alone.

Your 30-day clock is already ticking. Contact Team One Biotech now and move from notice to compliance with a clear plan. 

Disclaimer: The values, ranges, and timelines shared in this article are general indicators only. They differ for every STP and ETP depending on inflow characteristics, treatment technology, capacity, and the specific conditions in your notice. Always follow the limits and directions stated by your SPCB and consult a qualified professional before acting.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!
Tannery Effluent: Chrome, Sulphides and Biological Limits

It’s a Tuesday morning at your leather industry ETP, and the aeration tank looks wrong. Last week the mixed liquor was a healthy brown and the clarifier gave you a clean overflow. Today the tank has gone pale and grey, and the oxygen readings make no sense. Anyone who has done tannery effluent treatment for a few seasons has seen this.

Overnight, a slug of sulphide-rich liming liquor reached the equalisation tank, or a batch of chrome wastewater slipped past the tanyard drain. Your culture took the hit. The outlet sample goes to the lab, the report comes back failed, and then the phone rings. It’s the SPCB or the CETP management, and the word they use is penalty.

You can’t remove chrome, sulphide and salt from a tannery. You can stop them from killing your biology. This post walks through a practical way to do that, from stream segregation to bioaugmentation, without pretending any single step does the job alone.

Why Tannery Effluent Treatment Is One of the Toughest Jobs in Industrial Wastewater

Few industries hand an ETP operator a harder mix. A tannery doesn’t produce one effluent. It produces several, and they rarely arrive at a steady rhythm. Soaking, liming, unhairing, deliming, pickling, chrome tanning, retanning and dyeing each release different chemistry at different hours.

Then there’s hide-to-hide variation. Raw stock, wet-blue processing, buffalo versus goat skins, fresh versus long-cured hides: every change moves your load. A CETP serving a cluster has it worse. You receive the combined chemistry of many units, each with its own recipes and shift pattern.

The result is an influent that swings in pH, colour, salinity and toxicity within a single day. Biology likes stability. Tannery effluent offers almost none.

Five problem areas do most of the damage:

  • Trivalent chromium (Cr3+) from tanyard and chrome-tanning streams, toxic to microbes and stubborn in sludge
  • Sulphides (S2-) from beamhouse liming and unhairing, toxic, odorous and oxygen-hungry
  • Extreme salinity and TDS from hide curing salt, pickling and neutralisation chemicals
  • Recalcitrant proteinaceous solids from fleshing, hair and trimmings that hydrolyse slowly
  • Refractory organic nitrogen and ammoniacal nitrogen from protein breakdown and deliming salts

None of these is new. What catches plants out is the combination, arriving unbuffered in front of a biological system that never got a chance to cope. Treat each as its own problem with its own fix, and the aeration tank finally gets a fair chance.

Chrome Wastewater: Why Cr3+ Carryover Hurts Your Biology

Chrome Wastewater: Why Cr3+ Carryover Hurts Your Biology

Chrome wastewater is rarely your largest volume, but it’s often the most damaging per litre. Modest carryover, repeated day after day, can wear down a biological system that still looks fine on paper.

Where chrome enters the system

The main source is spent chrome-tanning liquor from the tanyard. Exhaustion is never complete, so some chromium always stays in the float. Rinse waters, draining and piling floors, sammying and shaving areas, and retanning washes add more.

Leaking valves and sloppy drain discipline do the rest. In a CETP, one member unit dumping chrome without pre-treatment can undo the discipline of everyone else.

How it inhibits microbial activity and settles in sludge

Trivalent chromium binds to cell surfaces and proteins, interfering with enzymes and slowing respiration. Nitrifiers go first because they’re slow-growing and sensitive. Heterotrophs follow, and the floc weakens.

Much of the chromium then precipitates into the biological sludge. That raises handling and disposal stress and complicates how you manage that sludge later.

Watch for these warning signs in the aeration tank:

  • Mixed liquor turning pale, thin or greyish-green
  • Oxygen uptake falling while dissolved oxygen climbs
  • Pin floc, turbid supernatant and a clarifier that won’t clear
  • Ammoniacal nitrogen rising in the outlet as nitrification stalls
  • Sudden foaming or a change in the smell of the tank

Chrome recovery and precipitation as the first line of defence

Collect spent chrome liquor separately, precipitate it with an alkali in a controlled pH window (roughly in the range of 8 to 9), settle it, and remove the bulk before the biology ever sees it. Many plants redissolve the recovered chromium sludge and reuse it in tanning, which cuts both toxicity and chemical cost. That pH range is a general value and varies from ETP to ETP, so confirm it with jar tests.

Chrome recovery isn’t a replacement for biology. It’s what lets biology survive. The trace chromium that still gets through is where chromium-resistant cultures step in.

Keep chrome liquor strictly off the general drain. A dedicated collection sump with a locked valve costs far less than restarting a dead aeration tank.

Sulphides in Beamhouse Effluent: The Silent Biomass Killer

Sulphides in Beamhouse Effluent: The Silent Biomass Killer

Beamhouse effluent is where most sulphide trouble starts. Liming and unhairing use sodium sulphide and lime, so the spent liquor is strongly alkaline and loaded with sulphide, hair pulp and dissolved protein. Tanyard effluent looks very different, which is why mixing the two is risky.

Toxicity, odour and oxygen demand effects

Sulphide is toxic to many aerobic microbes even at low concentrations. It also grabs oxygen chemically before your bacteria can use it.

A shock load can pull dissolved oxygen down within an hour or two. The culture starts to suffocate, and floc quality slips with it.

Odour follows because sulphide converts to hydrogen sulphide when pH drops. That’s a safety issue, not just a nuisance. Hydrogen sulphide is dangerous to your people.

Anywhere alkaline beamhouse flow meets acidic streams can release it: deliming and pickling drains, acid dosing points, or an equalisation tank whose pH has drifted down. Gas monitoring, ventilation and clear confined-space rules aren’t optional.

Catalytic sulphide oxidation and why segregation matters

Segregation comes first. Keep beamhouse effluent separate from tanyard and acidic streams at source, so sulphide-rich liquor reaches its own treatment tank.

There, catalytic oxidation (air with a manganese-based catalyst under alkaline conditions) converts sulphide into thiosulphate and eventually sulphate, which are far less harmful. Operating pH is usually kept alkaline, roughly in the range of 8 to 9, with contact time of several hours. These are general values and vary from ETP to ETP.

The aim isn’t perfection. It’s turning a violent shock into a steady, manageable load.

If you smell rotten egg at the equalisation tank around shift change, don’t blame the biology first. Check what the beamhouse released and what the pH did over the previous hour.

Salinity, Proteins and Organic Nitrogen: The Hidden Limiters

Salinity, Proteins and Organic Nitrogen: The Hidden Limiters

Handle chrome and sulphide well, and three quieter problems still cap what your biological system can deliver.

High TDS and osmotic stress

Hide-curing salt, pickling and neutralisation chemicals push tannery TDS well beyond what conventional activated sludge cultures tolerate. Cells lose water, activity drops and floc disperses.

Swinging salinity is worse than steady salinity. Microbes adapt to a stable level, not to constant jumps. Biology also doesn’t remove TDS, so high TDS wastewater is a limit you manage through segregation, dilution strategy and reject handling.

Proteinaceous solids and slow hydrolysis

Fleshings, hair pulp and trimmings are protein-rich and break down slowly. Without cultures that produce active proteases in saline, alkaline conditions, solids accumulate and COD stays stubborn. Your anaerobic unit then ends up overloaded with partly hydrolysed material.

Ammoniacal nitrogen and sensitive nitrifiers

Protein breakdown releases ammoniacal nitrogen, and deliming salts add more. Nitrifiers are slow-growing autotrophs and the first to suffer from chrome, sulphide and salt.

When nitrification fails, ammonia goes straight to your outlet report. Nitrifiers need adequate alkalinity, steady oxygen (dissolved oxygen typically in the range of 2 to 4 mg/L), and a long enough sludge age to hold on. As always, those ranges are general values and vary from ETP to ETP.

Untreated Stream ProblemPre-Treatment FixBiological Support
Chrome carryover from tanyardSegregation, recovery and precipitationChromium-resistant consortia for trace residuals
Sulphide shock from beamhouseSegregation and catalytic oxidationCultures that recover fast after oxygen dips
High and swinging TDSEqualisation, dilution and reject managementHalotolerant bacteria
Slow-hydrolysing proteinsScreening and fines removalProtease-active cultures
Ammoniacal nitrogen build-uppH and alkalinity controlAutotrophic nitrifying cultures

CPCB and SPCB Discharge Norms: What Non-Compliance Really Costs

Your consent conditions set the finish line, and for tanneries they’re tight. CPCB and the state boards regulate chromium, sulphides, ammoniacal nitrogen, BOD and COD, and the limits sit in the stringent low mg/L range. Chromium and sulphide are often held in the single-digit mg/L range or lower.

The exact figures depend on your state, your cluster and whether you discharge to a CETP, land or a water body. Check your current consent conditions rather than relying on any article, this one included.

Failing them carries consequences well beyond a bad lab report:

  • Environmental toxicity: chromium and sulphide harm aquatic life and soil microbes
  • Groundwater contamination: saline, chrome-bearing seepage from lagoons and drains is slow and costly to reverse
  • CETP penalties and over-fee charges: many CETPs levy extra charges on members whose inlet quality exceeds agreed limits
  • Closure directions: repeated violations can escalate from notices to closure directions for the unit or plant

Every one of these starts upstream. A stable biological unit is the cheapest compliance margin you’ll ever own.

How Biocultures Stabilise Aerobic and Anaerobic Units

Pre-treatment lowers the shock. Biology handles what’s left. That’s where bioaugmentation earns its place, as a stabiliser and not a substitute for good housekeeping.

Halotolerant, chromium-resistant consortia

Strains selected from saline and metal-exposed environments keep working when TDS rises and trace Cr3+ gets past your recovery step. They help hold the floc together and keep BOD and COD reduction going. They give the system a stable core population that doesn’t collapse at every swing.

Autotrophic nitrifying cultures

Nitrifiers convert ammoniacal nitrogen to nitrite and then nitrate. Because they grow slowly, a washout can take weeks to recover from on its own. Seeding with dedicated nitrifying bacteria for ammonia removal can shorten that recovery and protect your ammoniacal nitrogen compliance. Results depend on the site, and they’re never guaranteed.

Handling aerobic and anaerobic units correctly

In the aerobic tank, keep MLSS, oxygen and pH inside a workable window instead of chasing extremes. In the anaerobic unit, keep unoxidised sulphide out, since it inhibits methanogens, and keep pH and alkalinity steady.

Sulphate left after sulphide oxidation can still be reduced back to sulphide in anaerobic zones. That’s why oxidation and segregation upstream matter so much.

Recovery after shock loads

When a shock does hit, waiting for natural regrowth costs you days of non-compliance. A well-chosen bioculture for ETP and CETP re-seeds the system with active, tolerant cells, so recovery is quicker than it would be on its own.

Practical benefits you can expect to see:

  • Faster recovery after chrome, sulphide or salinity shocks
  • Steadier BOD and COD reduction through load swings
  • Lower sludge handling stress through better floc and hydrolysis
  • A wider compliance margin on ammoniacal nitrogen and COD

Is your biological unit losing ground to chrome or sulphide shocks? Talk to the Team One Biotech technical team for a site-specific assessment of your ETP. Explore our bioremediation solutions for industrial effluent or contact our technical team.

A Practical Stabilisation Checklist for Leather Industry ETP and CETP Teams

Disclaimer: The values and ranges mentioned in this article are general figures for reference. Actual values differ in every ETP depending on process, chemicals, hide type, water source and local consent conditions. Always validate through lab analysis and a site-specific trial.

Use this as a working list for your next review meeting:

  • Segregate streams at source. Keep beamhouse, tanyard and acidic flows separate so toxic liquors never mix.
  • Equalise properly. Give the plant enough mixing and buffering to flatten daily swings in pH, salinity and load.
  • Recover chrome. Collect spent liquor, precipitate, settle and reuse or dispose of it as per your regulations.
  • Oxidise sulphides. Treat beamhouse liquor through catalytic oxidation before it joins the main flow.
  • Check pH and dissolved oxygen. Track both at the equalisation tank and aeration tank, at least once every shift.
  • Seed with the right cultures. Use halotolerant, chromium-resistant and nitrifying cultures matched to your effluent.
  • Monitor closely. Follow oxygen uptake, floc quality, ammoniacal nitrogen and sludge settling, not only the outlet report.
  • Document everything. Log shocks, dosing and recoveries so you can show boards and management what happened and why.

Ready to put this into practice? Request a bioculture trial plan and sample analysis support from our process team, and we’ll help you set up a site-specific trial.

Frequently Asked Questions

Why does my aeration tank fail after chrome or sulphide shocks?

Chrome inhibits enzymes and floc formation, while sulphide poisons microbes and strips dissolved oxygen. Together they can collapse activity within hours, especially in unsegregated plants. Recovery takes longer when nitrifiers are lost.

Can biocultures work in high-TDS tannery effluent?

Yes, if they’re halotolerant strains selected for saline conditions. Conventional cultures lose activity as salinity climbs and swings. Results depend on your TDS range, stability and pre-treatment, so a site trial is the right way to confirm.

Is chrome recovery necessary if my ETP is already biological?

In most cases, yes. Biology can only handle trace chromium. Recovery and precipitation take the bulk away before it harms your culture and loads your sludge.

How do I improve ammoniacal nitrogen removal in a leather CETP?

Protect nitrifiers from chrome, sulphide and salinity shocks first. Then keep alkalinity, dissolved oxygen and sludge age in a supportive range, and consider seeding with autotrophic nitrifying cultures. Ranges vary from ETP to ETP.

Protect Your Plant Before the Next Shock Load Arrives

Reliable tannery effluent treatment comes down to sequence. Segregate at source, recover chrome, oxidise sulphide, then give your biology halotolerant, chromium-resistant and nitrifying cultures that can survive what’s left. Treat your leather industry ETP that way and chrome wastewater stops being a threat to your discharge report.

Do not wait for a failed discharge report or a closure notice. Contact Team One Biotech today to design a biological stabilisation plan for your tannery or CETP. Book a technical consultation, request a site assessment, or speak to our process team.

Disclaimer: The values and ranges mentioned in this article are general figures for reference. Actual values differ in every ETP depending on process, chemicals, hide type, water source and local consent conditions. Always validate through lab analysis and a site-specific trial.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!
Sugar Mill Effluent: Seasonal Operation and Biological Start-up

The crushing season is days away. The cane yard is filling, the boilers are being lit, and the mill is coming back to life. Down at the effluent plant, the aeration basin has sat still for months. The surface is dull, the walls are crusted, and nobody is quite sure what’s living in the bottom layer.

If you run the ETP, you already know what’s coming. The first week of effluent will test the biology and your compliance record at the same time. You can almost smell the complaints: a septic odour drifting towards the nearest village, a phone call from the board, an inspection at the worst possible moment. Then there’s the fear every ETP manager carries, a washout on the first day, with the basin turning sour before the biomass has a chance to establish.

This article is about getting through that moment. We’ll look at why sugar mill effluent treatment behaves so differently from other industries, where a sugar industry ETP usually stumbles at start-up, and how a structured biological start-up protocol can get a dormant basin working reliably, without weeks of anxious waiting.

A note before we begin: wherever we give numbers in this article, they are ranges and general values. They will differ from ETP to ETP depending on design, load, and site conditions.

Why Sugar Mill Effluent Treatment Is Different From Other Industries

Why Sugar Mill Effluent Treatment Is Different From Other Industries

Most industrial plants discharge effluent at a fairly steady rate all year. A sugar mill doesn’t. It runs hard for the length of the crushing season, then goes quiet for the long off-season. Your ETP has to wake up from near-zero activity and take a full load almost immediately. That’s the first thing that sets sugar mill wastewater treatment apart.

Seasonal swings are extreme

During the off-season, the biomass in the basin starves, dies off, or turns dormant. When crushing begins, effluent arrives in volume, and there is no gentle ramp-up on the mill side. The cane doesn’t wait for your biology.

The organic load moves constantly

Even within the season, high BOD COD effluent is the norm, and it doesn’t arrive evenly. The main contributors include:

  • Juice spillage and leakage from the extraction and clarification area
  • Floor and equipment washings, which can spike sharply during cleaning shifts
  • Barometric condenser water, which carries sugars and organics when entrainment occurs
  • Press mud contact wastewater, rich in dissolved and suspended organics

Any one of these can push a sudden seasonal shock load into the basin. In a mill where several things go wrong in the same shift, the combined load can be several times the usual level.

Plenty of carbon, almost no nitrogen or phosphorus

Sugar effluent is mostly sugars, which means carbon. What it lacks is nitrogen and phosphorus, the nutrients bacteria need to build new cells. Without proper N:P nutrient balancing, the biomass can’t grow in step with the load. You end up with weak, slimy, poorly settling sludge, or no real growth at all.

Anaerobic acidification happens fast

Sugars ferment quickly. If effluent sits in the equalisation tank or arrives in a basin without enough active biomass and oxygen, anaerobic acidification sets in. Volatile fatty acids build up and pH drops. That stresses whatever biomass is present, and the characteristic sour, septic smell follows. Once the basin has gone acidic, recovery is slow and painful.

Put these four problems together and you can see why a generic start-up approach fails here. Treating this as ordinary industrial wastewater is how most start-up trouble begins.

The Compliance Clock Starts on Day One of Crushing

The Compliance Clock Starts on Day One of Crushing

Here’s the uncomfortable reality. Regulators don’t give sugar mills a grace period for biological stabilisation. Your consent conditions apply from the first day effluent leaves the plant, and many mills also operate under Zero Liquid Discharge expectations for the sugar mill and its associated units.

In general terms, the CPCB SPCB discharge norms and your state’s consent conditions expect treated effluent to meet specified limits for parameters such as BOD, COD, suspended solids, and pH. Because limits and conditions vary by state, unit, and consent, we won’t quote values here. Please check your current consent to operate and any recent directions issued to your unit.

What happens when the early season goes wrong?

  • Biological washout, where the biomass is flushed or killed before it can establish, and the basin has to be re-seeded from scratch
  • Foul septic odour, which is often the first thing neighbours and local officials notice
  • Statutory penalties and environmental compensation
  • Show-cause notices, and in serious or repeated cases, closure directions

None of this is theoretical. A few bad days at the start of the season can leave a mark on a compliance record for the whole year, and it takes weeks of good performance to rebuild trust with the board.

Don’t let the first week of crushing decide your compliance record. If you’d like a second pair of eyes on your basin before the season begins, talk to the Team One Biotech technical team about a pre-season ETP assessment. It’s far easier to fix readiness issues in the off-season than during a washout.

Where Sugar Industry ETP Start-ups Usually Go Wrong

Where Sugar Industry ETP Start-ups Usually Go Wrong

After enough seasons, the same mistakes show up again and again. Most of them come from reasonable assumptions that don’t hold in a sugar effluent system.

  • Waiting for the effluent to “seed itself.” Some plants fill the basin and hope the incoming wastewater carries enough microbes to get going. It might, eventually. But sugar effluent acidifies faster than a natural population can establish, so the basin often sours before the right organisms take hold.
  • Relying only on old sludge or cow dung seeding. These are familiar, and they do provide some biomass. But old sludge from a long-idle basin is often weak and mixed in quality, and cow dung is a general-purpose seed that isn’t selected for high-carbon sugar wastewater. Both can work as part of a plan. On their own, they’re unreliable.
  • Ignoring nutrient dosing. This one is common. The basin is full, the aerators are running, and the biomass still doesn’t thrive, because there isn’t enough nitrogen and phosphorus to support growth against the carbon load.
  • Loading the basin too fast. The mill is running, the pressure is on, and the full effluent flow goes in before the biomass is ready. A young culture can’t handle a full load, and the result is a crash.
  • Skipping the pre-season inspection. Choked diffusers, damaged aerators, silted channels, and blocked lines turn up at the worst moment if nobody has checked them earlier.

Does any of this sound familiar? If so, you’re in good company. The good news is that each of these has a practical fix.

A Structured Biological Start-up Protocol That Works

A Structured Biological Start-up Protocol That Works

A good biological start-up protocol isn’t complicated. It’s disciplined. Each step prepares the ground for the next, and skipping one tends to cost more time than it saves.

Step 1: Pre-season basin readiness

Start well before the first cane is crushed. Walk the entire treatment train and check:

  • Aeration system: diffusers, blowers, surface aerators, and air lines for fouling, damage, and uniform mixing
  • Basin condition: accumulated sludge, grit, scum, and any dead zones that won’t mix
  • Equalisation and buffer tanks: capacity, mixing, and condition, since these protect the basin from sudden spikes
  • Pumps, valves, and flow measurement: you can’t control a load ramp-up you can’t measure
  • Dosing systems: nutrient and bioculture dosing points should be ready and calibrated
  • Lab readiness: meters for pH and DO, tools for SV30 and MLSS, and a microscope if available

Fix what’s broken now. A failed aerator in the first week of crushing is a problem you can avoid entirely.

Step 2: Rapid-activation bioaugmentation

This is where bioaugmentation for sugar industry effluent earns its place. Instead of waiting for a suitable population to develop on its own, you introduce a specialised microbial consortium selected to work on high-carbon, sugar-rich wastewater.

A well-matched consortium helps in three ways:

  • It establishes quickly, shortening the usual stabilisation period
  • It handles sugars and organic acids efficiently, which reduces the risk of acidification
  • It builds a stable, well-settling floc instead of weak, slimy growth

The consortium is typically dosed during the initial charging of the basin and then maintained at a lower level through the early weeks. Dosing rates depend on basin volume, available seed, and expected load, so they should be worked out with your technical team rather than copied from another plant.

Many mills find that combining bioaugmentation with a small amount of good-quality seed sludge gives the best result. The sludge provides biomass and the consortium provides the targeted capability.

Step 3: N:P balancing

Because sugar effluent is so carbon-rich, nutrient dosing is not optional. The aim is to keep nitrogen and phosphorus available in a proportion that matches the incoming organic load, so the biomass can grow and not merely survive.

In practice, N:P ratios are commonly targeted within a defined range relative to the BOD load, and the exact figures depend on your effluent characteristics and treatment configuration. Typical nutrient sources include urea or ammonium compounds for nitrogen and phosphate salts for phosphorus.

A few practical points:

  • Dose based on measured load, not a fixed routine
  • Check residual nutrients in the treated water, since too little starves the biomass and too much wastes money and adds to downstream load
  • Adjust as the load changes through the season

As always, ratios and doses are general and will differ from ETP to ETP depending on design, load, and site conditions.

Step 4: Controlled load ramp-up

Patience here pays off. Rather than sending the full flow in on day one, bring the load up in stages while the biomass builds.

  • Begin with a fraction of the design load, often somewhere in the range of a quarter to a half
  • Increase in steps once the basin shows stable pH, healthy DO, and improving settling
  • Use equalisation to smooth out peaks while the culture is still young
  • Expect a stabilisation period of roughly 5 to 10 days for many plants, though some settle sooner and some take longer

If the mill can divert or hold back the strongest streams, such as concentrated washings, during the first days, that helps considerably. A short conversation between the ETP team and the process team before start-up is worth more than most people expect.

These figures are general. Your own ramp-up schedule should reflect your design and the condition of your basin.

Step 5: Monitoring and shock load buffering

Once the basin is running, monitoring tells you whether the biology is healthy. Check these regularly during stabilisation, and more often when the load is changing:

  • pH: typically maintained between 6.5 and 8.0, with early warning of acidification if it begins to fall
  • Dissolved oxygen (DO): enough in the aeration basin to support aerobic activity throughout, with attention to dead zones
  • MLSS: a measure of how much biomass you’re carrying, expected to build steadily through start-up
  • SV30: a quick settling test that reveals sludge quality, with trends more useful than single readings
  • F/M ratio: keeps the food-to-microorganism balance within a workable range as load increases
  • Microscopic observation: healthy floc, active protozoa, and filament levels tell you things no meter can

Microscopy is often the first place trouble shows. A change in the microbial picture can appear a day or two before parameters shift, which gives you time to act.

For the rest of the campaign, plan for shocks. Maintain a bioculture top-up dose during the season, keep the equalisation tank mixed and in use, watch the weak points in the mill that generate spills, and have a response plan ready when pH starts to drop. A basin with a healthy, well-fed population recovers from a shock load far faster than one running on the edge.

Ranges for pH, DO, MLSS, and F/M are general guidance. Your own targets should be set from your ETP’s design and operating history.

Ready to plan your own start-up? Contact Team One Biotech to talk through your basin, your expected load, and the timeline to crushing. A short technical discussion now can save you a very long first week.

A Season-Wise Operating Snapshot

Here’s the whole year at a glance. Treat it as a planning aid, not a rulebook.

StageMain focusKey actions
Pre-season (weeks before crushing)ReadinessInspect aerators, diffusers, pumps, and tanks; clean and repair; calibrate dosing and monitoring; plan seed, bioculture, and nutrient supply
Start-up week (first days of crushing)Establish the biologyCharge basin with bioculture and seed; begin N:P dosing; start at a partial load; monitor pH, DO, and SV30 closely; observe under the microscope
Mid-season (stable campaign)Hold and protectRamp to design load as the basin allows; maintain bioculture top-ups; adjust nutrients to load; use equalisation to buffer spikes; track MLSS, F/M, and settling
End-of-season (closing weeks)PreservationReduce load gradually; keep the basin aerated at a low level where possible; avoid abrupt shutdown; remove excess sludge; plan the off-season care

All timelines are approximate and depend on the mill’s crushing schedule and ETP design.

The last stage is one that many plants overlook. How you close the season largely determines how easy next season’s start-up will be. A basin that is gently wound down and kept in reasonable condition is far easier to revive than one abandoned to rot over the off-season.

How Team One Biotech Supports Your Crushing Season Start-up

We make bioremediation solutions, and we work with plants that face exactly these problems every year. Our approach is practical. We’d rather help you avoid a crisis than rescue you from one.

Here’s what that support looks like:

  • Bioremediation solutions for sugar effluent: microbial products suited to high-carbon wastewater, applied through bioaugmentation as part of a planned start-up
  • Technical guidance on commissioning or reviving dormant aeration basins, from readiness checks through load ramp-up
  • Help with nutrient planning so your N:P balance matches your actual load
  • Advice on shock load management during the campaign, including what to do when pH or odour trends go the wrong way
  • Site-level discussion, because no two plants are alike, and what works at one mill may need adjusting at another

The goal is simple: to bring your aeration basin revival forward so you aren’t left waiting through a long, uncertain stabilisation period or watching a crash unfold. For ETP start-up for sugar mills, speed matters, but reliability matters more.

If your plant also includes a distillery, co-generation unit, or other linked processes, we can look at the full picture, because effluent streams from these units affect each other.

Frequently Asked Questions

How long does a sugar industry ETP take to stabilise at the start of the season?

It varies with design, seed quality, temperature, and how carefully the load is ramped. Many plants stabilise in roughly 5 to 10 days when bioaugmentation, nutrient balancing, and staged loading are done properly. Plants relying on natural seeding often take longer. These are general ranges and differ from site to site.

Is cow dung or old sludge enough to start a sugar mill ETP?

They can supply some biomass, but they rarely deliver the speed or consistency needed for sugar effluent. The organisms in them aren’t selected for high-carbon wastewater, and old sludge is often weak. Most plants get better results combining seed with a targeted microbial consortium and proper nutrient dosing.

Why is nutrient dosing so important in sugar mill wastewater treatment?

Sugar effluent is rich in carbon but short on nitrogen and phosphorus. Without enough of both, biomass can’t grow properly, settling suffers, and treatment efficiency drops. Nutrient dosing based on measured load keeps the biology healthy and helps the plant meet its consent conditions throughout the campaign.

What causes foul odour in a sugar mill ETP?

Mostly anaerobic acidification. Sugars ferment quickly when oxygen or active biomass is short, producing volatile acids and sulphide compounds that smell sour and septic. Common triggers include sudden shock loads, weak biomass, poor mixing, and equalisation tanks left standing. Good aeration, buffering, and active bioculture usually bring it under control.

Can a dormant aeration basin be revived quickly before crushing?

Yes, in most cases, provided the mechanical equipment is sound. Revival usually involves clearing accumulated solids, checking aeration, charging the basin with a suitable microbial consortium and seed, dosing nutrients, and ramping up load in stages. Starting preparation well before crushing gives the best outcome.

Plan the Start-up Before the Cane Arrives

The first week of crushing is where a sugar mill’s effluent record is quietly decided. A dormant basin, a carbon-heavy load, missing nutrients, and fast-souring effluent are a hard combination to meet without preparation. With a structured start-up, though, it’s a very manageable one.

To recap the essentials of good sugar mill effluent treatment:

  • Inspect and repair before the season, not during it
  • Introduce a suitable microbial consortium instead of waiting for natural seeding
  • Balance nitrogen and phosphorus against the carbon load
  • Ramp up gradually and watch the biology closely
  • Buffer shocks and wind the season down with next year in mind

A dependable sugar industry ETP is built in the weeks before crushing begins. Book a pre-season ETP assessment with Team One Biotech before the crushing starts. Call or write to our technical team, share your basin details and expected load, and plan your biological start-up now. Don’t let the first week decide your compliance record.

Disclaimer: The values, ranges, and timelines mentioned in this article are general in nature. Actual figures vary from one ETP to another based on design, effluent characteristics, seasonal load, and operating conditions. Please consult our technical team for a site-specific assessment.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!
Food Processing Wastewater: Variable Load and Odour Control

It starts with a production surge nobody planned for. By the next morning, the equalization tank smells sour, the aeration tank surface is covered in grey scum, and the operator on shift is already tired. Then the phone rings. A neighbour is complaining about the smell, and an audit is only days away.

If this sounds familiar, you are not alone. Food processing wastewater rarely behaves the same way two days in a row, and most plants only notice the problem once the odour has already left the boundary wall. This guide explains why it happens and what you can do about it. It covers practical biological and engineering steps that keep your food industry ETP stable, compliant, and quiet.

Why Food Processing Wastewater Is So Unpredictable

Why Food Processing Wastewater Is So Unpredictable

Walk through any meat, poultry, dairy, or vegetable processing unit and you will see why the effluent never settles into a pattern. The load going to your treatment plant is tied to what the production floor does, and the production floor changes constantly.

Variable loads, seasonal peaks, and wash-down cycles

A typical day brings batch cleaning, product changeovers, tank drain-downs, and equipment wash-downs. Each one sends a slug of concentrated waste to the drain in a short window. Add seasonal peaks such as harvest months, festival demand, or export orders, and the variable organic load can swing from mild to severe within hours.

That swing shows up as a BOD COD shock load. Biochemical oxygen demand (BOD) and chemical oxygen demand (COD) are the two numbers that tell you how much organic matter your biology must consume. In many food plants, COD can move across a very wide band, from a few hundred to several thousand mg/L, depending on what is being processed that day. These are general values and will differ in every ETP depending on the product, process, and plant design.

Your bacteria cannot grow overnight to match a sudden jump. That gap between load and biological capacity is where most problems begin.

Fast hydrolysis of starches and sugars

Vegetable, bakery, beverage, and grain-based processes add another twist. Starches and sugars break down quickly in water. This is called hydrolysis, and it produces simple organic acids within a short time, sometimes a few hours.

When that happens in a holding tank or equalization tank, the pH drops. The wastewater turns acidic before it even reaches the aeration basin. Acidic, sugar-rich feed favours acid-forming organisms over the slower-growing bacteria that polish the effluent. The result is a sour tank, poor settling, and a treatment train that struggles to catch up.

What Really Causes the Odour in a Food Industry ETP

What Really Causes the Odour in a Food Industry ETP

Odour is not a mystery. It is chemistry and biology reacting to a lack of oxygen, and it usually points to a few specific causes.

Volatile fatty acids and hydrogen sulphide

Volatile fatty acids (VFAs) are small organic acids such as acetic, propionic, and butyric acid. They form when organic matter ferments without enough oxygen. Butyric acid in particular has the sharp, rancid smell that plant staff describe as “something gone off”. Meat and poultry waste, with its fats and proteins, makes this worse.

Hydrogen sulphide odour is the rotten-egg smell. It comes from sulphate-reducing bacteria, which become active when oxygen is absent and sulphate is present in the water. Proteins also release sulphur compounds as they decay. H2S is more than a nuisance. It corrodes concrete and metal, irritates eyes and throats, and can reach levels that matter for worker safety.

Septic conditions and dead zones

Wherever wastewater sits still, it goes septic. Common culprits include:

  • Poorly mixed equalization tanks with settled solids at the bottom
  • Screen chambers and sumps where food solids stay for long periods
  • Corners and low-velocity zones in aeration basins
  • Sludge holding and handling areas
  • Long, flat drain lines that collect fats and fines

In these dead zones, oxygen runs out and anaerobic activity takes over. Even if your main aeration tank is healthy, a septic equalization tank can send VFAs and sulphides into the system continuously.

Why masking chemicals only hide the problem

Many plants reach for fragrances, oxidizing sprays, or neutralizing chemicals when complaints start. These products cover the smell for a while, but the source keeps producing it. Dosing has to continue, often at higher volumes in peak season, and chemical costs keep climbing.

Masking agents also do nothing for scum, poor sludge settling, or shock-load recovery. Your plant ends up paying for the cover-up and still facing the same underlying problem. Fixing the biology and the conditions behind the odour is slower to set up, but it costs less over time.

Struggling with odour complaints? Talk to our team about a site-specific bioremediation plan.

Compliance Pressure: What Plant Teams Are Really Worried About

Compliance Pressure: What Plant Teams Are Really Worried About

Ask an ETP manager what keeps them up at night and the answer is rarely about technology. It is about being caught out.

Your plant has to hold stable, continuous compliance with discharge limits set by the CPCB and your State Pollution Control Board. These CPCB discharge norms and SPCB compliance conditions typically cover BOD, COD, and total suspended solids (TSS), along with pH and oil and grease for many food categories. Odour and H2S emissions are also watched, especially where homes or commercial areas sit close to the plant.

Beyond the numbers, there are several other pressures:

  • Audit readiness. Food safety audits and regulatory inspections look at the condition of your treatment area, records, and housekeeping.
  • Community complaints. One persistent odour problem can lead to repeated visits and notices.
  • Permit conditions. If your site runs on Zero Liquid Discharge, any instability upstream affects the recovery and reuse stages. If you discharge to surface water or a common facility, quality has to hold on every sampling day, not just on average.

Limits differ by industry category, state, and discharge point. Treated BOD limits, for example, are often set within a range of a few tens of mg/L, and COD limits within a range of roughly one hundred to a few hundred mg/L. These are general values and will differ in every ETP depending on the product, process, and plant design. Always check your own consent conditions.

The real danger is not a single bad day. It is a pattern of instability that leaves you exposed whenever a sample is taken.

Practical Strategies to Handle Variable Load

Practical Strategies to Handle Variable Load

You cannot control what production sends down the drain, but you can control how your plant receives it. These steps work together, and most of them need discipline more than capital.

  • Equalization and flow balancing. A well-sized equalization tank evens out peaks in flow and strength. Retention time commonly sits in a range of several hours to about a day, depending on how erratic your discharge is. Make sure the tank is actually mixed, because a large tank that is not mixed just becomes a septic reservoir.
  • pH buffering. Sugar-rich and acid-forming waste can pull pH down quickly. Install online pH monitoring in the equalization tank and dose a suitable buffer in a controlled way. Keep the working pH in a near-neutral band, typically somewhere around the high six to low eight range for most biological systems.
  • Controlled feeding. Use a feed pump with a variable speed drive, or a timer-based schedule, so the aeration tank receives load gradually instead of in gulps. Resist the urge to pump the whole equalized volume forward the moment production ends.
  • Aeration management. Match air supply to actual demand. Dissolved oxygen in the aeration tank should generally be held in a range of about one to three mg/L. Too little invites septic pockets and filamentous growth. Too much wastes power and can break up flocs.
  • Sludge age and MLSS stability. Mixed liquor suspended solids (MLSS), the biomass in your aeration tank, should be held within a steady working band instead of being allowed to swing. Plan sludge wasting on a regular schedule, not only when the settling tank looks bad.
  • Seasonal preparedness. Before peak season, review your last year’s load pattern, service blowers and diffusers, stock up on required nutrients and consumables, and refresh your biological culture. Plan manpower for the weeks when your team is stretched thin.

These are general values and will differ in every ETP depending on the product, process, and plant design. Use them as a starting point and refine them with your own operating data.

Biological Odour Control That Works Without Masking Chemicals

Engineering fixes give your Biological Odour Control to work. The biology itself is what actually removes the odour at its source.

Biostimulation and bio-augmentation

Biostimulation means improving conditions so that useful bacteria already in your system grow better, for example by supplying micronutrients, balancing nitrogen and phosphorus, and correcting pH. Bio-augmentation means adding selected bacterial cultures to strengthen the population when the existing one cannot cope. In a food industry ETP the two often work best together. Nutrients and conditions support the biology, and added cultures bring extra capacity for fats, starches, and proteins.

This is the core of bioremediation for food industry plants. Instead of covering up the smell, you give the system the tools to consume what causes it.

Facultative bacteria in low-oxygen pockets

Not every corner of your ETP will ever be fully aerobic, however well you design it. That is where facultative bacteria earn their place. These strains can work with oxygen when it is available and keep working when it is scarce.

In a low-oxygen pocket, such as the bottom of an equalization tank or a screen chamber, they continue breaking down organic matter before it turns into VFAs. They also compete with sulphate-reducing organisms, which helps limit sulphide formation. The effect is that odour-forming compounds are consumed earlier in the process, instead of being produced and then chased downstream.

Localized bio-elimination at the source

Rather than treating the whole plant uniformly, target the places where odour begins:

  • Screens and grit chambers: food solids and fats collect here and start fermenting quickly
  • Sumps and collection pits: stagnant water that goes septic overnight
  • Equalization tank: the biggest single source in most food plants
  • Sludge handling areas: thickeners, drying beds, and holding tanks

Dosing a suitable microbial formulation at these points builds a working biology right where the problem starts. It supports odour reduction without adding fragrance chemicals to the air or the effluent.

Less scum, faster recovery

Scum forms when fats, oils, and partially degraded solids float and trap gas. A strong, diverse bacterial population breaks down fats and surface organics so they do not collect as a thick layer. This helps reduce surface scum control efforts and manual skimming.

After a shock load, a resilient biological system can return to normal sooner. It does not remove the need for good operation. What it does is shorten the time between a bad day and a stable effluent, which is where compliance is won or lost.

A Simple Action Checklist for ETP Managers

Print this and keep it near the control panel.

  • Walk the plant every day and note where smell is strongest. Odour is your cheapest early warning.
  • Check pH in the equalization tank and aeration tank at the start of every shift.
  • Confirm that mixers and aerators are running and that no dead zones have formed.
  • Review production schedules each week so you know when wash-downs and heavy batches are coming.
  • Feed the aeration tank gradually after large discharge events.
  • Keep dissolved oxygen and MLSS inside your working band, and record both.
  • Clear screens and sumps on a fixed schedule, not only when they overflow.
  • Look at your scum layer each day. A change in colour or thickness usually means a change in load or biology.
  • Keep nutrient and culture stock available before peak season starts.
  • Update your logbook so audits find clear, consistent records.

Want a second opinion on your plant? Book a free consultation or technical discussion with our team.

How Team One Biotech Supports Your Food Industry ETP

Team One Biotech manufactures bioremediation solutions in India for industrial wastewater treatment, including food and beverage effluent. We are not a chemical masking supplier, and we do not believe a single product fits every plant.

Our approach starts with understanding your process. We look at your product mix, discharge pattern, tank layout, and current problem areas. From there, we suggest microbial and nutrient solutions that support your existing treatment steps, whether the issue is odour, scum, slow recovery after shock loads, or sludge handling.

In practical terms, this can include:

  • Microbial formulations selected for fats, starches, proteins, and VFAs
  • Facultative strains for equalization tanks, sumps, and other low-oxygen zones
  • Guidance on dosing points, monitoring, and operating adjustments
  • Support during seasonal peaks, when your plant is under the most stress

Results depend on your plant design, load, and operating discipline, and we will tell you plainly what biology can and cannot do for your site.

Ready to get ahead of the next production surge? Request a plant assessment or book a consultation with our bioremediation experts, and get a site-specific treatment plan.

Frequently Asked Questions

Why does my food industry ETP smell worse during peak season?

Peak season sends higher and more variable organic loads, while your oxygen supply and biomass stay the same. The extra load turns parts of the system septic, and VFAs and H2S begin to form. Dead zones in the equalization tank and screen areas usually get worse first.

How can biological treatment handle sudden BOD and COD spikes?

Biological treatment copes better when you pair it with flow balancing and gradual feeding. Biostimulation and added bacterial cultures increase the system’s capacity to consume organic matter quickly. This helps reduce the time your effluent stays out of range, though no biology can absorb unlimited load.

Can bioremediation replace odour masking chemicals?

In many plants, bioremediation can reduce or replace routine masking chemicals, because it addresses the cause instead of covering the smell. Microbes consume the compounds that form VFAs and sulphides at the source. Results depend on how well the system is mixed, aerated, and monitored, so it works best alongside good operating practice.

What causes thick scum on the aeration tank surface?

Scum usually comes from fats, oils, and grease that were not removed upstream, along with poorly degraded solids and certain filamentous organisms. Low dissolved oxygen, unstable sludge age, and sudden shock loads make it worse. Better pre-treatment, steady aeration, and a stronger bacterial population help reduce it.

How do I stay compliant with CPCB and SPCB limits during production surges?

Plan for surges before they arrive. Balance flow in the equalization tank, buffer pH, feed gradually, and keep MLSS and dissolved oxygen steady. Support the biology with suitable cultures and nutrients, and keep clear records. Always check your own consent conditions, since limits vary by industry and state.

Stable Food Processing Wastewater Treatment Is a Daily Habit

Managing food processing wastewater is less about one big fix and more about small, consistent habits. Balance the load, keep the tanks mixed, watch your pH, and give your biology the support it needs to handle whatever production sends your way. A stable food industry ETP means fewer odour complaints, calmer audits, and an operator who is not firefighting every weekend.

Masking chemicals will always be a temporary answer. Biostimulation, facultative strains, and targeted bio-elimination at the source tackle the problem where it begins, and they can improve your plant’s resilience season after season.

A final reminder: every number mentioned here is a general range. Values for BOD, COD, pH, retention time, dissolved oxygen, and limits will differ in every ETP depending on the product, process, and plant design, so confirm them against your own data and consent conditions.

If your plant is dealing with odour, scum, or unpredictable loads, we would like to help. Talk to our bioremediation experts, request a plant assessment, and get a site-specific treatment plan.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!
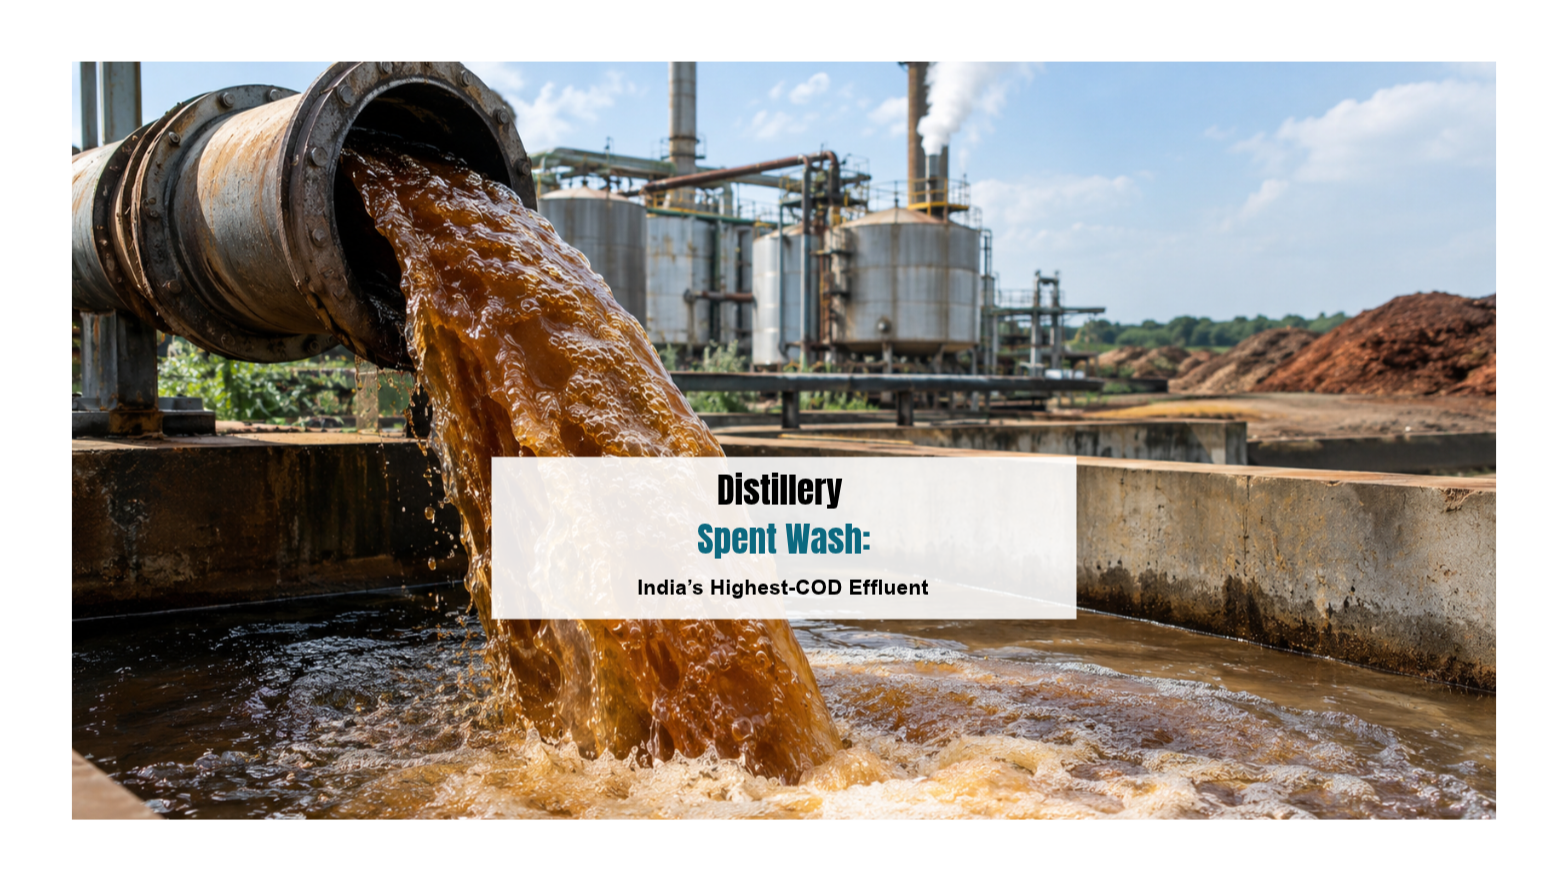
Distillery Spent Wash: India’s Highest-COD Effluent

Last Monday your digester was behaving. Gas flow was steady, the flare was quiet, and the lab sheet looked boring in the best way. This morning the VFA readings have climbed overnight, gas production has dropped, the pH is sliding, and the whole reactor smells sour. A pollution board inspection date is sitting on your calendar.

If that sounds familiar, you already know why distillery spent wash treatment is unforgiving. This is the strongest distillery effluent produced by any Indian industry, with spent wash COD typically in the range of 80,000 to 1,50,000 mg/L. Every small mistake in feed, temperature or biology shows up fast.

This article covers why the stream behaves the way it does, what is inside it, where biomethanation fails, and how specialized methanogenic cultures, aerobic polishing and ZLD fit together.

These are general values and will differ from one ETP to another based on feedstock, distillery process, and plant design.

Why Spent Wash Is in a Category of Its Own

Why Spent Wash Is in a Category of Its Own

Most industrial effluents are a nuisance. Spent wash is a different class of problem. It leaves the distillation column hot, acidic, dark brown, and loaded with dissolved organics at a concentration that no conventional treatment train was designed to handle.

Put the scale in perspective. Domestic sewage typically carries COD in the range of a few hundred mg/L. Spent wash can carry hundreds of times that. A distillery producing a few hundred kilolitres of alcohol per day generates spent wash in volumes that can run to several multiples of that figure, so you are dealing with high strength and high volume together.

Molasses and grain feedstocks behave differently, and you should know which one your plant is dealing with:

  • Molasses distillery ETP: Very high COD, intense dark colour from melanoidins, high sulfate and potassium, and heavy salt load. Colour and sulfate dominate the design conversation.
  • Grain distillery effluent: Usually lower in colour and sulfate, but richer in suspended solids, proteins and fibre. Thin stillage, wet cake handling and fats bring foaming and solids carryover problems.

Both break conventional ETP logic for the same reason. A standard aerobic system cannot supply enough oxygen economically at this strength, and a standard anaerobic system struggles with the inhibitors riding along with the organics. The stream needs a staged approach, where each step prepares the effluent for the next.

Values such as COD and volume vary widely across plants. Treat all ranges here as indicative only.

What Is Really Inside Distillery Effluent

What Is Really Inside Distillery Effluent

COD tells you how much organic load you have. It does not tell you why your biology is struggling. That depends on what is in the COD.

  • Melanoidin pigments: Formed by Maillard reactions during molasses processing and distillation. They give the spent wash its dark brown colour and resist biological breakdown. Anaerobic treatment removes only a limited portion, so colour often survives into the downstream stages.
  • Volatile fatty acids (VFA): Acetic, propionic and butyric acids are natural intermediates, but a high incoming VFA fraction narrows your safety margin. Once acid production outruns methane formation, the digester tips towards souring.
  • Phenolic and polyphenolic compounds: These come from the raw material and the cooking and fermentation steps. At elevated levels they inhibit methanogens and slow granule formation.
  • Sulfates: Particularly high in molasses spent wash. Sulfate-reducing bacteria compete with methanogens for the same substrates and produce H2S, which is toxic to methanogens and lowers the quality of your biogas.
  • Temperature: Spent wash leaves the column at a temperature well above what most digesters tolerate. Cooling is a mandatory step, and poorly controlled cooling is a common cause of upset.
  • Low pH: Raw spent wash is acidic, typically in the range of 3.5 to 5. Feeding it without adequate pH correction or recycling dilution invites acidification.
  • Potassium and salts: These raise conductivity and can contribute to osmotic stress on microbes and to scaling in pipes and heat exchangers.

Each of these is a separate failure path. Many plants fix one and keep losing to another.

These are general values and will differ from one ETP to another based on feedstock, distillery process, and plant design.

The Compliance Reality: CPCB, SPCB and the ZLD Mandate

The Compliance Reality: CPCB, SPCB and the ZLD Mandate

Indian distilleries operate under a clear direction from the regulators: no untreated or partially treated effluent leaves the plant. CPCB norms and SPCB compliance requirements push molasses and grain distilleries toward Zero Liquid Discharge (ZLD). Surface discharge of spent wash, even in small amounts or “just during monsoon,” is exactly the kind of lapse that draws attention.

The consequences are practical, not theoretical:

  • Closure notices that can halt production
  • Environmental compensation levies tied to the duration and volume of violation
  • Directions that restrict operations until corrective action is verified
  • Reputational pressure from lenders, auditors and brand owners

Compliance is not a one-time audit event. It is a daily operational pressure. Your SPCB can review your records, sample your effluent and visit unannounced. A digester upset on a Tuesday can become a compliance problem by Friday if the overflow has nowhere to go.

There is also the matter of incineration boiler feed. In the concentration and incineration route, the concentrated spent wash needs to meet the solids content, viscosity and consistency your boiler can handle. A poorly stabilized upstream process delivers inconsistent feed, which means unstable combustion, fouling and more downtime.

Meeting the prescribed CPCB/SPCB norms starts upstream, with a stable biological system. Everything downstream depends on it.

Where Biomethanation Systems Fail (And Why)

Where Biomethanation Systems Fail (And Why)

Biomethanation is the backbone of spent wash treatment. High-rate reactors such as the UASB reactor and the CSTR digester convert a large share of the organic load into biogas, and biogas recovery pays back part of the cost of operating the ETP. But these systems fail in recognisable patterns.

Shock loads. A sudden jump in organic loading, a change in feed pH, or a spike in temperature overwhelms the methanogens. This is the classic anaerobic digester shock load. Acid formers keep working at pace, methanogens slow down, and the balance tips.

VFA accumulation and pH crash. When acids build up faster than methanogens can consume them, alkalinity is used up, pH falls, and methanogens slow down even further. It becomes a self-reinforcing loop. Once pH has crashed, recovery takes much longer than the upset did.

Sulfate inhibition. High sulfate pushes sulfate-reducing bacteria ahead of methanogens. H2S builds up, biogas quality drops, and corrosion risk rises in gas lines, scrubbers and engines.

Biomass washout. In a UASB, high upflow velocity, gas hold-up or poor granule quality can carry biomass out of the reactor. Rebuilding a granule bed is slow.

Foaming. More common with grain-based effluent, and with sudden VFA changes. Foam can clog gas lines and damage downstream equipment.

Scaling. Calcium, magnesium and struvite-type deposits can foul pipes, heat exchangers and gas systems, quietly reducing capacity.

The table below links symptoms to causes and the biological response that typically helps.

Observed signProbable causeTypical biological response
Rising VFA, falling pHOrganic overload or inhibited methanogensReduce feed, restore alkalinity, support with active methanogenic culture
Gas production dropping steadilyMethanogen loss or phenol/sulfate inhibitionCheck inhibitors, bioaugment with tolerant strains
High H2S in biogasSulfate-reducing bacteria dominatingManage sulfate load, rebalance consortium
Granules breaking up, solids in outletWashout, poor granule integrityReduce hydraulic stress, reseed with granule-forming cultures
Persistent foamingSudden VFA shifts, proteins, fatsStabilize loading, review feed variability

These are general values and will differ from one ETP to another based on feedstock, distillery process, and plant design.

Share your digester data with us. If you are seeing any of these signs, send us your recent VFA, alkalinity, pH, gas production and loading data. Our team can review it and tell you whether the pattern points to a biological problem, a process problem, or both.

How Specialized Methanogenic Cultures Stabilize the System

This is where biology does what chemicals and hardware cannot. Methanogens are slow growers, sensitive to shock, and easily outcompeted when conditions turn. Specialized methanogenic cultures give you a stronger, more tolerant microbial base, so the digester recovers faster and survives upsets with less damage.

Strain-selection logic. Not every methanogenic culture suits every plant. Selection should reflect:

  • Feedstock type (molasses or grain)
  • Reactor type (UASB or CSTR)
  • Operating temperature range (mesophilic or thermophilic)
  • Sulfate and phenol load
  • The role of acetoclastic and hydrogenotrophic methanogens in your consortium

A consortium suited to a molasses plant with high sulfate will not necessarily suit a grain plant with a fatty, fibrous feed.

Acclimatization. Even a good culture needs time to adapt to your spent wash. Gradual loading, with close monitoring of VFA, pH and gas yield, lets the consortium adjust to your inhibitors instead of being shocked by them. Rushing this step is one of the most common reasons a new culture fails to perform.

Bioaugmentation. Bioaugmentation is the planned addition of selected cultures to strengthen a working or struggling digester. It is useful during commissioning, after a washout, during seasonal feed shifts, and when you see early signs of instability. A well-timed dose can help rebuild the methanogenic population before the problem deepens.

Restart after upset. After a souring event, the typical recovery path is to stop or reduce feed, restore pH and alkalinity gradually, let VFA fall, reintroduce an active culture, and then bring loading back step by step. Skipping straight to full feed is how digesters fail a second time.

Granule health. In UASB systems, granules are your biological asset. Healthy granules carry diverse, layered consortia and settle well. Cultures that support granule formation and stability can help limit washout and improve resilience to load variation.

Tolerance to phenols and sulfates. Some methanogenic strains handle moderate phenolic and sulfide stress better than others. Selecting and maintaining these populations can help narrow the gap between what your feed delivers and what your biology can absorb.

None of this removes the need for good operations. A culture is not a substitute for loading discipline, cooling control or pH management. What it can do is widen your margin for error, which is exactly what a distillery ETP needs.

Request a strain-selection consultation or trial. Tell Team One Biotech your feedstock, reactor type and current performance, and our team will help you shortlist a culture and an acclimatization plan for your digester.

Operating Parameters That Matter

Good process control is the baseline that cultures build on. These are general working ranges for high-rate anaerobic treatment of spent wash:

  • Temperature (mesophilic operation): Roughly 33 to 40 degrees Celsius
  • Temperature (thermophilic operation): Roughly 50 to 58 degrees Celsius
  • Reactor pH: Roughly 6.8 to 7.6
  • Organic loading rate (OLR): Varies widely by reactor type, typically in the range of 4 to 12 kg COD per cubic metre per day
  • Hydraulic retention time (HRT): Typically in the range of several days to over two weeks, depending on reactor type and feed strength
  • VFA to alkalinity ratio: Ideally kept below roughly 0.3 to 0.4
  • Biogas methane content: Commonly in the range of 55 to 70 percent
  • Biogas yield: Often in the range of 0.3 to 0.5 cubic metres per kg COD removed

Watch the trends, not just the numbers. A VFA to alkalinity ratio that creeps upward over a few days tells you more than a single reading.

These are general values and will differ from one ETP to another based on feedstock, distillery process, and plant design.

From Anaerobic Output to ZLD: Polishing and Beyond

Even a well-run anaerobic system does not finish the job. Digester outlet still carries residual COD, colour, ammonia and dissolved salts. Reaching ZLD needs several more steps.

  • Aerobic polishing: Activated sludge or similar aerobic treatment reduces remaining organics and ammonia. It also helps stabilize the stream before the next stage. Aerobic polishing works better when anaerobic output is consistent, which is another reason upstream stability matters.
  • Colour removal: Melanoidins that survive biological treatment can be addressed through selected biological, adsorptive or oxidative approaches, depending on the site. This stage matters where colour limits or reuse targets apply.
  • Concentration: Evaporation, often multiple-effect, concentrates the treated stream into a thick syrup and produces condensate.
  • Incineration or composting route: The concentrate is fed to an incineration boiler, or in some plants blended into composting systems, subject to approvals. Consistent feed quality from upstream protects boiler performance.
  • Condensate recycling: Condensate can be treated and reused in process water, cooling or dilution, which reduces freshwater demand and supports ZLD.

Each step depends on the one before it. A digester that swings between healthy and sour sends variable feed downstream, and the damage compounds. That is why biological stability is a compliance asset, not only a process goal.

Frequently Asked Questions

Why is distillery spent wash COD so high compared with other effluents?

It carries large amounts of dissolved sugars, organic acids, proteins and recalcitrant pigments left over after fermentation and distillation. Little of this is removed before it leaves the column, so the COD stays in the range of tens of thousands to over a lakh mg/L.

Can a UASB reactor handle spent wash on its own?

It can handle a large part of the organic load, but it rarely delivers discharge-ready quality alone. Aerobic polishing, concentration and incineration or similar routes are typically needed to reach ZLD.

What causes a digester to sour, and how can it be recovered?

Souring usually follows overloading, a sudden change in feed pH or temperature, or inhibition of methanogens. Recovery generally involves reducing feed, restoring alkalinity and pH, reintroducing an active methanogenic culture, and rebuilding load gradually.

Does bioaugmentation work for sulfate-heavy molasses spent wash?

It may help when strains are chosen for sulfide and phenol tolerance and the process is well controlled. It works best alongside sulfate management, not instead of it.

Conclusion

Distillery spent wash treatment is not forgiving, and no single piece of equipment solves it. A stable ETP rests on disciplined loading, proper cooling and pH control, a resilient methanogenic population, and downstream polishing and ZLD steps that can rely on consistent input. When the biology holds, biogas recovery improves, compliance pressure eases, and your team spends less time firefighting.

If your digester has already given you a scare, or you want to be ready before it does, bring us your data. Talk to our bioremediation team before your next shock load does the talking for you. Share your VFA, alkalinity and gas trends, and we will help you build a culture and restart plan fitted to your plant.

Disclaimer: All values and parameters mentioned in this article are general, indicative ranges. Actual figures vary for every ETP depending on raw material, process, effluent characteristics, and design. A site-specific study is always recommended.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!
Dairy Effluent Treatment: FOG and Shock Load Management

It is Monday morning, and you have barely parked the car. You walk over to the aeration tank and there it is: a thick, greasy scum layer sitting on the surface, grey and stubborn. A sour smell is drifting toward the plant gate. Before you reach your desk, the phone rings. The environment officer wants to know what happened over the weekend. If that scene feels uncomfortably familiar, you are not alone.

Almost every ETP manager in a dairy has lived some version of this morning. The cause is rarely one big failure. It is usually a quiet build-up of fats, a cleaning cycle that dumped a sudden load, and a biomass that simply could not keep up.

Dairy effluent treatment is hard because the wastewater changes character through the day, and fats do not behave like ordinary organic matter. This article walks you through what really happens inside your dairy ETP, why FOG and shock loads cause so much trouble, and how lipolytic biocultures, enzymatic pre-treatment and biological equalization can bring your system back under control. We will also cover what your team can do this week, before a single product is dosed.

Why Milk Processing Wastewater Is One of the Toughest Streams to Treat

Why Milk Processing Wastewater Is One of the Toughest Streams to Treat

Milk is food. That is the root of the problem. Every drop that reaches the drain carries lactose, proteins and fat, all easy meals for bacteria. The result is milk processing wastewater with an organic strength far above most domestic and many industrial streams. Raw BOD and COD commonly sit in the thousands of mg/L.

Strength is only half the story. Variation is the real enemy. A cheese plant, a butter line and an ice cream unit each produce different effluent, and even inside one plant the stream changes by shift, by product and by season. Peak milk season brings more volume and more whey. Hot weather brings warmer effluent that sours faster.

Then come the cleaning chemicals. Caustic washes and acid rinses from CIP systems push the pH well outside the comfortable range for microbes, which prefer roughly 6.5 to 8.5. Add sanitisers and detergents, and you have a stream that feeds your bacteria and stresses them at the same time.

Note: These are general values. Actual figures vary from one ETP to another depending on product mix, plant design, cleaning practices and operating conditions.

Dairy wastewater is not just strong. It is strong, changeable and chemically unpredictable, and your treatment plan has to respect all three.

Understanding FOG in Dairy Effluent: What Really Happens Inside Your ETP

Understanding FOG in Dairy Effluent: What Really Happens Inside Your ETP

How fats turn into LCFAs and why they inhibit biomass

Milk fat is made of triglycerides: three fatty acid chains attached to a glycerol backbone. Bacteria cannot swallow that whole molecule. They first need enzymes called lipases to cut the chains loose. Once that happens, you get glycerol, which is easy to digest, and long-chain fatty acids, or LCFAs, which are not.

Here is where plants get caught. When fats arrive faster than the biomass can process them, LCFAs accumulate. At high concentrations they coat bacterial cell walls and interfere with how cells take in food and oxygen. Picture a thin oily film over every microbe in your tank. Activity slows, treatment efficiency drops, and the fat that should have been consumed floats to the top instead.

Cold effluent makes it worse. Fats solidify, stick together and travel through the system as lumps rather than fine droplets that bacteria can reach.

Scum, clogged diffusers, foul odor and filamentous growth: the chain reaction

Once fats collect, a chain reaction begins. It usually runs in this order:

  • Fats float and form a scum layer in the equalization tank and aeration basin.
  • Grease coats diffuser membranes and pipework, cutting oxygen transfer.
  • Dissolved oxygen falls in pockets of the tank, and anaerobic zones appear.
  • Those zones release sour, rotten odors from volatile fatty acids and sulfur compounds.
  • Filamentous bacteria, which thrive on low oxygen and fatty food, take over and cause sludge bulking.
  • Sludge settles poorly in the clarifier, solids carry over, and TSS, BOD and oil and grease in the final discharge climb.

Every step feeds the next. That is why chasing odor alone, with masking agents or extra chemicals, rarely works. You have to break the chain where it starts, at the point where fat enters.

Scum, odor and bulking are usually one problem seen from three angles. Control the FOG, and the other two often ease.

Shock Loads and pH Swings: The Silent Killers of Your Aeration Basin

Common shock load sources inside a dairy plant

A shock load is any sudden jump in organic strength, flow or pH that your biomass has not had time to adapt to. In dairy plants, the usual suspects are:

  • CIP cycles, especially when pre-rinse and final rinse streams go straight to the drain
  • Product changeovers that flush concentrated residues out of pipelines and tanks
  • Whey or buttermilk spills, and rejected batches sent to drain instead of being collected
  • Batch dumping of expired, returned or off-spec product
  • Shift-end washdowns, when several sections discharge together
  • Fat-heavy cleaning from butter, cheese vat and ice cream lines

Most of these are not failures. They are normal operations. The problem is timing. Everything arrives together, and your ETP sees it as one big gulp.

What a shock does to the microbial population

Your aeration basin is a living community. The bacteria in it need steady food, steady oxygen and a steady pH. A sudden organic surge makes them consume oxygen faster than your blowers can supply it. Dissolved oxygen collapses, sensitive species die back, and the survivors tend to be the filamentous ones that cope better with low oxygen.

A pH swing does similar damage in a different way. A strong caustic slug can rupture cells outright, while an acid slug favours fungi and filaments over healthy flocs. Recovery is slow because the community has to rebuild, and rebuilding takes days to weeks while your discharge keeps going to the regulator.

The signs are familiar: rising foam, brown or grey scum, cloudy supernatant, poor settling and a sharp smell. If your microscope also shows fewer protozoa and more filaments, shock has already done its work.

Note: These are general values. Actual figures vary from one ETP to another depending on product mix, plant design, cleaning practices and operating conditions.

Aeration basin stability depends on predictability. Shock management is really about making your load and pH arrive in a way your biomass can handle.

Struggling with recurring scum or sudden BOD spikes? Talk to the Team One Biotech technical team about a site-specific assessment of your dairy ETP.

The Biological Approach to Dairy ETP Management

The Biological Approach to Dairy ETP Management

A biological approach does not mean doing nothing and hoping. It means giving your biomass the tools to handle fats and fluctuations, and the conditions to do its job. Three tools carry most of the weight.

Lipolytic biocultures for FOG breakdown

Lipolytic biocultures are selected bacterial strains that produce lipases and can break down fats, oils and grease. Dosed at the right point, they establish themselves in the system, attack the scum layer and stop fat from building up again. Because they work on the triglycerides and also help consume the LCFAs that follow, they deal with the inhibition problem at both ends.

Results depend on choosing cultures that tolerate the real conditions of your plant: fluctuating pH, variable temperature and traces of cleaning chemicals. A culture that performs well in a lab can struggle in a working dairy ETP. That is why site-specific selection matters, and why dosing should be steady rather than occasional. Many plants see visible improvement in scum and odor within a few weeks of consistent dosing, though this varies.

This is the heart of bioremediation for ETP: use living microbes to do what chemicals only partly achieve, without adding to your sludge.

Enzymatic pre-treatment to open up fats before they reach the aeration tank

Enzymes are the fast starters. Lipase-based formulations dosed in the grease trap, collection sump or equalization tank begin splitting fats before they ever reach the aeration basin. Fats that are already opened up are easier for bacteria to take in and less likely to form floating mats.

Think of it this way. Enzymes cut the big pieces, and biocultures eat the smaller ones. Together they shorten the path from stubborn fat to digestible material. Contact time matters, so dose where there is enough retention for the enzymes to act and where temperature and pH are reasonably favourable.

Enzymatic pre-treatment also helps keep sewer lines, pumps and screens cleaner. That means fewer blockages and less foul odor around the collection area.

Biological equalization to buffer load and pH

An equalization tank is where you flatten the peaks. In many plants it is treated as a simple holding tank, but it can do far more. When it is mixed, gently aerated and seeded with the right cultures, it becomes a first biological stage that starts consuming easily degradable load and buffers the pH before the stream reaches the main reactor.

The benefits add up:

  • Flow and load reach the aeration basin at a steadier rate, so the biomass is never surprised.
  • Caustic and acid streams from CIP partly neutralise each other, narrowing pH swings.
  • Fats are partially degraded, which reduces scum at the next stage.

Keep the tank mixed enough to avoid settling and septic conditions, but not so hard that you create foam. A pH range of roughly 6.5 to 8.5 at the equalization outlet is a practical target.

Note: These are general values. Actual figures vary from one ETP to another depending on product mix, plant design, cleaning practices and operating conditions.

Biocultures do the long-term work, enzymes give a head start, and equalization protects both from the worst of your load swings.

Operational Best Practices Your Team Can Start This Week

Operational Best Practices Your Team Can Start This Week

None of these need a capital project. Your team can begin today.

  • Grease trap upkeep: Inspect and clean traps on a fixed schedule rather than after they overflow. Remove fat solids by hand and never wash them down the drain.
  • Flow equalization: Spread discharges across the day where possible. Use the equalization tank as a true buffer and avoid bypassing it during cleaning or spills.
  • CIP scheduling coordination: Sit down with production and sanitation teams. Stagger CIP cycles so caustic, acid and rinse streams do not hit the ETP together, and collect first rinses for separate handling.
  • DO and MLSS monitoring: Check dissolved oxygen at several points in the basin, not just one. Track MLSS and settling behaviour so you spot drift before it becomes a failure.
  • Regular microscopic checks: A simple microscope shows filaments, protozoa and floc structure long before lab results do. Make it a routine, not an emergency tool.
  • Dosing discipline: Biocultures and enzymes work through consistency. Dose at the same points and times, and keep a log. Skipping doses in busy weeks is a common reason for relapse.

Also keep whey, buttermilk and rejected product out of the drain wherever possible. These are worth more as by-products or feed than as effluent, and they are among the biggest single causes of sudden BOD spikes.

A calm ETP is built on small, boring habits done every day.

Compliance Benefits: Staying Ahead of CPCB and SPCB Norms

CPCB and SPCB discharge norms for BOD, COD, oil and grease and TSS leave little room for erratic performance. A plant that meets limits on a good day and misses them on a bad one is still exposed to notices, penalties and, in serious cases, closure directions. Regulators care about consistency, and consistency is where biology does well.

Chemical-heavy approaches can bring quick clarity, but they carry costs. Coagulants and flocculants create chemical sludge that must be handled, stored and disposed of, and that disposal is itself a liability. Chemical use also rises with every spike. In a biological system, much of the organic load is converted into biomass and gas rather than concentrated into chemical sludge.

A biological approach is designed to help support compliance in several ways:

  • It can make BOD and COD reduction steadier by keeping the biomass active and healthy.
  • It helps with oil and grease removal by degrading fats directly instead of just skimming them.
  • It supports better settling, which helps TSS control.
  • It can reduce chemical sludge and the disposal burden attached to it.
  • It helps protect municipal sewers and surface receiving bodies from fat-laden, oxygen-hungry discharge.

Better odor control also protects you from neighbour complaints, which are often what trigger an inspection in the first place. No product can guarantee compliance, and operation, monitoring and housekeeping still matter. But a stable biological system gives you something chemical dosing rarely does: a margin of safety.

Quick Takeaway: Regulators reward steady performance. Biology helps you deliver it without piling up chemical sludge.

Want to know where your plant stands? Request a free consultation to review your current ETP performance against CPCB and SPCB norms.

Frequently Asked Questions

How do you control FOG in dairy wastewater biologically?

Start with good grease trap practice, then add lipolytic biocultures and lipase enzymes at the trap, sump or equalization tank. The enzymes open up the fat and the cultures consume what is left. Steady dosing and good mixing are what make it work.

Why does my dairy ETP smell worse after cleaning cycles?

CIP discharges bring a surge of organic load, fats and sudden pH change. Oxygen demand spikes, anaerobic pockets form, and volatile acids and sulfur compounds are released. Staggering cleaning and buffering in equalization usually reduces this.

How can a dairy ETP handle sudden shock loads?

Buffer first, then biology. A well-mixed equalization tank, coordinated CIP schedules and a robust, regularly dosed culture help the system absorb surges. Watching dissolved oxygen closely also gives you time to react.

Can bioremediation reduce chemical sludge in milk processing wastewater?

Yes, it can. When biology handles more of the organic and fat load, the need for coagulants and flocculants often drops, and so does the sludge they generate. The extent depends on your plant design and current practice.

How long before I see results?

Many plants notice changes in scum and odor within a few weeks of consistent dosing, followed by steadier BOD, COD and oil and grease trends. Timelines depend on loading, temperature and how well the basics are managed.

Bringing Your Dairy ETP Back Under Control

Dairy effluent treatment will never be effortless. Milk processing wastewater is rich, variable and loaded with fats, and your cleaning routines will always create peaks. But a Monday morning with scum, smell and a phone call is not inevitable. When you control FOG at its source, buffer shocks through biological equalization and keep a healthy, well-fed culture working in the aeration basin, your dairy ETP becomes calmer, cheaper to run and far easier to defend in front of a regulator.

Team One Biotech works with milk, cheese, butter and ice cream plants to build site-specific biological programs around lipolytic biocultures and enzymatic solutions. You do not have to guess your way through it..

Your aeration tank can recover. Team One Biotech will help you get there, one stable day at a time.

Disclaimer: The information in this article is for general guidance only. Wastewater characteristics, treatment performance and dosing requirements differ in every ETP. A site-specific assessment is recommended before any process change.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!
Pharmaceutical Wastewater Treatment: Reducing COD and BOD Without Chemical Overdose

It’s rarely a good sign when your phone rings after midnight and it’s the ETP shift supervisor. Maybe the outlet COD reading spiked. Maybe the pH swung outside range during a batch discharge. Maybe there’s a CPCB inspection scheduled in three days and the numbers from last week still haven’t stabilized. If you manage Industrial wastewater treatment at a pharmaceutical API plant, you already know this feeling, the quiet dread that sits behind every consent-to-operate renewal, every surprise sampling visit, every conversation with a plant head who wants to know why the treatment system that worked fine last quarter suddenly can’t keep up.

The instinctive response, when COD and BOD numbers start creeping toward the edge of compliance, is to reach for more chemicals. More coagulant. More oxidant. More nutrient dosing to keep the biological stage alive under stress. It feels like the safe move, something is clearly better than nothing, and chemicals are fast.

But this is exactly where a lot of pharmaceutical effluent treatment plants get stuck. Chemical overdosing doesn’t just fail to solve the underlying problem, it often creates new ones: more sludge to dispose of, more corrosion in tanks and piping, more residual toxicity hitting the biological stages downstream, and a slow, steady rise in operating cost that never quite translates into proportional compliance gains.

This article is about what actually works instead, the biological, oxidation, and segregation-based strategies that reduce COD and BOD in a way that holds up over time, rather than just buying a few weeks before the next crisis call.

Why API Plant Effluent Is So Difficult to Treat

Pharmaceutical Wastewater Treatment: Reducing COD and BOD Without Chemical Overdose

Pharmaceutical API manufacturing effluent is a different animal from most industrial wastewater. It isn’t simply “high strength” in the way people casually describe difficult effluent, it’s structurally resistant to the kind of treatment that works well for more conventional waste streams.

A few things make API effluent especially stubborn:

  • Recalcitrant organic molecules. Many active pharmaceutical ingredients and their intermediates are specifically designed to resist biological breakdown, that’s part of what makes them effective as drugs, and it’s exactly what makes them hard to treat as waste.
  • Antibiotic and solvent residues. Trace antibiotics can suppress the very microbial populations you’re relying on to digest organic load, while solvent carryover adds toxicity and unpredictability to the mix.
  • Imbalanced COD-to-BOD ratios. A lot of API effluent carries a high proportion of non-biodegradable COD relative to biodegradable BOD, which means standard activated sludge systems are working against the composition of the waste itself, not just its volume.
  • Batch-driven variability. Unlike continuous manufacturing processes, API production tends to generate effluent in batches, so pH, temperature, and organic load can swing significantly from one discharge to the next.

It’s worth pausing on how this compares to something like textile industrial waste BOD challenges, since the two are often discussed in the same breath. Textile effluent is typically high-volume with dyes, salts, and moderate organic load, difficult, but largely biodegradable once color and salinity are managed. Pharmaceutical effluent flips that equation: lower volume, in many cases, but far more chemically stubborn, and far less forgiving of a “treat and forget” approach.

The real risk here isn’t just a failed outlet reading. Undertreated pharma effluent that slips past the primary and secondary stages can disrupt the biological ecosystem further down the treatment train, killing off the microbial cultures a plant depends on for consistent performance, and turning a one-time problem into a weeks-long recovery effort.

The Chemical Overdose Trap, Why More Isn’t Better

The Chemical Overdose Trap, Why More Isn't Better

When COD or BOD numbers start trending in the wrong direction, chemical dosing is the lever every ETP operator can pull immediately, no equipment change, no retrofit, no waiting. Increase the coagulant. Push more oxidant into the system. Add nutrients to try to keep a struggling biological stage functioning. In the short term, it can look like it’s working.

The trouble is what happens after that.

  • Sludge volume climbs. Higher chemical dosing generally means more chemical sludge, which drives up disposal frequency and cost, often the single biggest hidden expense in an over-dosed ETP.
  • Equipment wears faster. Excess oxidants and coagulants are corrosive by nature, and tanks, pumps, and piping degrade faster under chronic overdosing.
  • Downstream biology suffers. Residual chemicals from an overdosed primary stage can carry through and suppress the very biological cultures the secondary stage depends on, creating a cycle where more chemical dosing is needed just to compensate for damage the last round of dosing caused.
  • Costs rise without matching results. Plants often find that operating expense keeps climbing while COD/BOD reduction plateaus, a sign the system is fighting the wrong problem.
  • Secondary parameters drift. Overdosing to fix one parameter can push others, like TDS, or residual chlorine, out of their own compliance range, effectively trading one non-conformance for another.

A quick note before going further: any figures or ranges referenced in this article, including the ones ahead, are general, indicative values meant to illustrate typical patterns, not guaranteed outcomes. Actual dosing thresholds, sludge generation, and treatment results vary significantly depending on ETP design, influent characteristics, and operating conditions, and should always be validated through a site-specific assessment.

Compliance Pressure: Why This Isn’t Just an Operations Problem

Compliance Pressure: Why This Isn't Just an Operations Problem

It’s tempting to treat COD and BOD management as a purely technical exercise, get the numbers within range, move on. But for pharmaceutical API plants, this is fundamentally a business continuity issue, not just an environmental one.

CPCB norms for the pharmaceutical sector are specific and increasingly strict, and many pharma clusters now operate under Zero Liquid Discharge expectations that leave very little margin for error. A pattern of non-compliance doesn’t just mean a warning letter, it can mean:

  • Financial penalties that compound with repeat violations
  • Consent-to-operate revocation, which can halt production entirely
  • Plant shutdown orders, sometimes with limited notice
  • Reputational damage that follows a facility long after the technical issue is resolved

For the ETP manager, this pressure is deeply personal. You’re often the one whose name is on the compliance report, whose judgment gets questioned in the plant head’s office, and whose sleep gets interrupted when a reading looks off. Getting ahead of this, rather than reacting to it, is the difference between managing a routine operational challenge and managing a crisis.

If your plant has an upcoming CPCB inspection cycle, it’s worth getting an effluent and compliance assessment done now, before the pressure builds, not after a notice arrives. A proactive review can surface the gaps that a reactive chemical top-up will never fix.

A Smarter Path, Advanced Biological, Oxidation, and Segregation Strategies

A Smarter Path, Advanced Biological, Oxidation, and Segregation Strategies

The alternative to chemical overdosing isn’t doing less, it’s being more deliberate about where and how treatment effort is applied.

Bioculture-Led Biological Treatment

Standard activated sludge systems are built for general municipal or light industrial waste, they weren’t designed with recalcitrant pharmaceutical molecules in mind. Targeted bioculture treatment, using microbial consortia selected and acclimatized specifically for API effluent characteristics, changes that equation.

These engineered cultures are chosen for their ability to break down the specific complex organics present in a given plant’s effluent stream, rather than relying on a generic microbial population to muddle through. Over time, plants using this kind of targeted biological approach tend to see benefits like:

  • Lower overall sludge generation compared to chemical-heavy treatment
  • Reduced dependency on coagulants and oxidants for routine load
  • More stable, consistent BOD/COD reduction across varying batch conditions

Again, these are general patterns observed across different plant configurations, actual performance depends heavily on the specific bioculture selected, the effluent profile it’s matched to, and how gradually it’s introduced and monitored.

Advanced Oxidation Processes (AOPs)

For the fraction of effluent that resists biological breakdown entirely, certain solvent residues or highly recalcitrant intermediates, advanced oxidation processes serve a different purpose. Ozone-based systems, Fenton-type reactions, and UV-based oxidation work by breaking down these non-biodegradable compounds chemically, converting them into simpler, more biodegradable forms.

The key here is positioning: AOPs work best as a targeted pre-treatment step applied to the hardest-to-treat fraction of the stream, not as a blanket treatment for the entire effluent volume. Used this way, they reduce the biological load that the downstream stage has to handle, rather than trying to replace biological treatment altogether.

Waste Segregation at Source

Of the three strategies here, segregation is often the most overlooked, and frequently the most cost-effective. Mixing high-strength or solvent-laden streams with general wash water dilutes the problem without solving it, and creates shock loading that makes every downstream stage work harder than it needs to.

Practical segregation practices worth implementing:

  • Isolating solvent recovery streams before they reach the main effluent line
  • Separating high-COD batch discharges for dedicated pre-treatment rather than blending them into the general flow
  • Installing or expanding equalization tanks to buffer load variability before it hits the biological stage

Plants that get segregation right often find that the biological and chemical stages downstream perform more predictably simply because they’re no longer absorbing unpredictable shock loads.

Building a Chemical-Light ETP Strategy, What to Prioritize

Pulling this together into something actionable, here’s a practical sequence for ETP managers looking to move away from a chemical-heavy default:

  • Characterize effluent streams individually before designing or redesigning any treatment approach, blended, averaged data hides the streams actually causing problems
  • Introduce bioculture augmentation gradually, with close monitoring, rather than switching over all at once
  • Apply AOPs selectively, targeting the hardest-to-treat fractions rather than the entire effluent volume
  • Segregate at source wherever the plant layout allows it, even partial segregation reduces shock loading meaningfully
  • Track COD/BOD trends over time, rather than reacting to any single reading in isolation, since one anomalous sample rarely tells the full story

If your plant hasn’t had a tailored bioculture or AOP feasibility study done for its specific effluent profile, that’s a reasonable next step before committing to any major treatment redesign. A feasibility study grounded in your actual influent characteristics avoids the guesswork that leads plants back into chemical overdosing in the first place.

FAQ Section

Can biological treatment alone handle high-COD pharmaceutical effluent?

In many cases, biological treatment, particularly bioculture-led systems matched to the specific effluent, can handle a significant portion of the organic load, but the most resistant fractions typically still benefit from a pre-treatment step like advanced oxidation. The right mix depends on the plant’s specific COD composition and how much of it is genuinely biodegradable versus recalcitrant.

How is API plant wastewater different from textile industrial waste in terms of BOD load?

Textile effluent tends to carry high volume with dyes and salinity as the primary challenge, and is generally more readily biodegradable once those factors are addressed. API plant wastewater, by contrast, often carries a lower BOD relative to its COD, with a larger share of non-biodegradable and recalcitrant organic content, making it structurally harder to treat even at similar overall strength.

Does reducing chemical dosing affect compliance with CPCB and ZLD norms?

Reducing chemical dosing doesn’t inherently threaten compliance, in fact, a well-designed biological and segregation-first approach can improve consistency of compliance over time by reducing the swings and side effects that come with chemical overdosing. That said, any change to dosing strategy should be validated through monitoring and, ideally, a site-specific assessment before scaling it across the full plant.

How long does it take to see COD/BOD improvement after introducing bioculture treatment?

Timelines vary considerably depending on the culture used, the effluent characteristics, and how the transition is managed, but plants often begin to see measurable stabilization within a few weeks to a couple of months of gradual introduction. As with all figures in this article, this is a general indicative range, not a guarantee, actual results depend on site-specific conditions and should be tracked and validated through ongoing monitoring.

Conclusion, Compliance Without Compromise

Chemical overdosing feels like the responsible move when COD or BOD numbers start slipping, but it’s a short-term fix that tends to generate long-term costs, from mounting sludge disposal bills to equipment wear to biological systems that never quite stabilize. A biological, oxidation, and segregation-led strategy takes more upfront thought, but it holds up in a way that chemical overkill never does, and it puts the plant in a stronger position for the next CPCB cycle, not just the current one.

If your plant is dealing with persistent COD/BOD challenges, chronic chemical dependency, or the kind of compliance anxiety that keeps you checking readings at odd hours, it’s worth having a real conversation about what a chemical-light strategy would look like for your specific effluent profile. Connect with Team One Biotech for an effluent assessment or a bioculture trial suited to your plant’s actual load and compliance requirements, not a generic fix, but a treatment path built around what your effluent is actually doing.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!
Aerobic vs Anaerobic Wastewater Treatment: Choosing the Right Method

There’s a particular kind of stress that comes with running an effluent treatment plant. It’s not the loud, obvious kind, it’s the quiet dread that builds in the days before a CPCB or SPCB inspection, when you’re not entirely sure your numbers will hold up. It’s the sinking feeling when influent load spikes unexpectedly and you watch your treatment system struggle to keep pace. It’s the budget meeting where someone asks why energy costs keep climbing, and you don’t have a satisfying answer.

If you’re a plant manager, utility head, or process engineer, you already know that the treatment method you choose isn’t just a technical decision, it’s a risk management decision. Pick the wrong system for your load profile, and you’re staring down non-compliance flags, penalty notices, or worse, closure directives. Pick a system that’s technically sound but poorly matched to your space and manpower constraints, and you’re fighting an uphill battle every single day just to keep things running.

This is where the aerobic versus anaerobic wastewater treatment question becomes so important, and so often misunderstood. Both are proven, widely used approaches. Both can deliver compliant discharge quality. But they behave very differently under real-world industrial conditions, and the “right” choice depends heavily on your specific effluent characteristics, available infrastructure, and operational bandwidth.

In this article, we’ll walk through how aerobic sewage treatment and anaerobic wastewater treatment actually work, where each one shines, how they stack up against each other operationally, where an anoxic tank fits into the picture, and how to think through the decision in a way that protects your compliance standing rather than gambling with it. We’ll also touch on the microbiology driving these processes, because understanding what’s actually happening inside your tanks makes troubleshooting, and future-proofing, a lot easier.

Understanding Aerobic Sewage Treatment

Understanding Aerobic Sewage Treatment

Aerobic sewage treatment relies on oxygen-dependent microorganisms to break down organic pollutants in wastewater. Air or pure oxygen is introduced into the treatment tank, through diffusers, surface aerators, or mechanical agitation, creating an environment where aerobic microbes can thrive and metabolize organic matter efficiently. The by-products of this reaction are primarily carbon dioxide, water, and biomass, which is why aerobic systems are generally associated with lower odor generation compared to their anaerobic counterparts.

This method tends to be best suited for effluents with a low-to-moderate organic load, think domestic sewage, or industrial wastewater from sectors like food and beverage, textiles, or light manufacturing, where the organic strength isn’t extreme but consistency and speed of treatment matter.

Energy and aeration considerations:

  • Aerobic systems generally require a continuous or near-continuous supply of oxygen, which translates to a meaningful and ongoing energy demand, a real concern given how energy tariffs have been trending upward across most industrial zones.
  • Aeration equipment (blowers, diffusers, surface aerators) needs regular maintenance, and any inefficiency here directly inflates operating costs.
  • Retention times in aerobic systems tend to fall on the shorter end relative to anaerobic processes, meaning you can often achieve target reductions in a comparatively smaller treatment footprint, a genuine advantage for retrofitted or space-constrained plants.
  • Sludge generation in aerobic systems tends to be higher than in anaerobic systems, which brings its own downstream cost in the form of sludge handling and disposal.

For plants where energy cost isn’t the primary constraint but space and speed of treatment are, aerobic sewage treatment is often the more practical starting point.

Understanding Anaerobic Wastewater Treatment

Understanding Anaerobic Wastewater Treatment

Anaerobic wastewater treatment works in the complete absence of oxygen. Instead of oxygen-breathing microbes, this process relies on anaerobic microbes that break down organic matter through a multi-stage biological pathway, hydrolysis, acidogenesis, acetogenesis, and finally methanogenesis, ultimately producing biogas (a mixture largely composed of methane and carbon dioxide) as a valuable by-product.

This is precisely why anaerobic treatment is often the preferred route for high-strength, high-organic-load effluent, the kind you’d typically see from distilleries, dairies, sugar mills, pulp and paper units, or other sectors where influent BOD and COD levels can vary from moderately high to significantly elevated depending on the process generating the wastewater.

Energy recovery potential vs slower process dynamics:

  • One of the standout advantages of anaerobic treatment is energy recovery. The biogas generated can, in many setups, be captured and used as a fuel source, partially offsetting the plant’s overall energy burden, which is a meaningful counterbalance to rising utility costs.
  • However, anaerobic systems generally operate on longer retention times compared to aerobic systems, since the microbial breakdown pathway is more complex and the organisms involved tend to be slower-growing.
  • Anaerobic microbes are also more sensitive to fluctuations in temperature, pH, and toxic shock loads. A sudden change in influent characteristics can disrupt the microbial balance and take considerably longer to recover from compared to an aerobic system.
  • Odor management is a more prominent consideration here, since by-products like hydrogen sulfide can be generated, meaning that anaerobic systems typically require more robust gas handling and odor control infrastructure.

For plants dealing with consistently high organic loads and looking for a way to offset energy costs through biogas recovery, anaerobic wastewater treatment often makes strong operational and financial sense, provided the system is designed to handle load variability without tipping into instability.

Thinking through whether your influent profile is better suited to aerobic or anaerobic treatment isn’t something you need to work out alone, a plant-specific assessment from Team One Biotech’s bioremediation team can help clarify which direction actually fits your load and infrastructure.

Aerobic and Anaerobic Treatment of Wastewater, Key Operational Differences

Aerobic and Anaerobic Treatment of Wastewater, Key Operational Differences

When you line them up side by side, the aerobic and anaerobic treatment of wastewater differ across nearly every operational dimension that matters to a plant manager under compliance pressure:

  • Organic load handling capacity: Aerobic systems perform well with low-to-moderate organic loads; anaerobic systems are generally better equipped to handle high-strength, high-organic-load effluent.
  • Energy requirement: Aerobic treatment tends to demand higher ongoing energy input for aeration; anaerobic treatment tends to require less external energy and can offset a portion of demand through biogas recovery.
  • Sludge generation: Aerobic processes generally produce a higher volume of sludge requiring disposal; anaerobic processes tend to generate comparatively lower sludge volumes.
  • Space and infrastructure needs: Aerobic systems often need less land area for a given treatment capacity; anaerobic systems, particularly those using lagoons or larger digesters, can require a larger footprint, though compact anaerobic reactor designs have narrowed this gap considerably.
  • Retention time: Aerobic systems typically operate on shorter retention times; anaerobic systems generally require a longer retention period to achieve comparable reductions.
  • Odor and by-product management: Aerobic systems tend to generate lower odor levels; anaerobic systems require more deliberate gas capture and odor mitigation measures, though this is offset by the value of biogas recovery.

None of this is abstract for a compliance-focused plant manager. Your ability to consistently hit target reductions in BOD, COD, and suspended solids, the numbers CPCB and SPCB inspectors care about, depends directly on matching your treatment method to your actual load profile. A plant running an aerobic system against a load it wasn’t designed for will chronically underperform, and repeated underperformance is exactly what triggers regulatory scrutiny and penalty exposure.

Where the Anoxic Tank Fits In

This is where a lot of confusion creeps in, so let’s clear it up directly: an anoxic tank is not the same as an anaerobic tank, even though the terms sound similar and are frequently mixed up in casual conversation.

An anoxic tank in a sewage treatment plant operates in a low-oxygen environment, not entirely oxygen-free like an anaerobic system, but with dissolved oxygen levels low enough that specific microbial processes, particularly denitrification, can occur. In an anoxic tank, facultative bacteria use the oxygen bound in nitrate molecules (rather than free dissolved oxygen) to break down organic matter, converting nitrates into nitrogen gas that’s released to the atmosphere.

The distinction matters because:

  • Anaerobic conditions involve a complete absence of oxygen (and nitrates), typically used for organic load reduction and biogas generation.
  • Anoxic conditions involve a controlled, low-oxygen environment specifically used for nitrogen removal.

This is why many modern ETPs are moving toward a hybrid approach, combining anaerobic, anoxic, and aerobic stages in sequence to tackle organic load reduction, nitrogen removal, and final polishing all within one integrated system. For plants facing stricter nutrient discharge norms alongside conventional BOD/COD requirements, incorporating an anoxic stage is often what closes the compliance gap that a purely aerobic or purely anaerobic system can’t address on its own.

The Microbiology Behind It, Anaerobic Microbes vs Heterotrophic Microbes

The Microbiology Behind It, Anaerobic Microbes vs Heterotrophic Microbes

You don’t need a microbiology degree to run a compliant plant, but understanding the basic players involved makes a real difference when something goes wrong and you’re trying to figure out why.

Anaerobic microbes are organisms that survive and function without oxygen. They work in coordinated stages, some breaking down complex organic molecules into simpler compounds, others converting those compounds into acids, and finally, methanogenic organisms converting those acids into methane-rich biogas. These microbes tend to be slower-growing and more sensitive to environmental swings, which is why anaerobic systems can take noticeably longer to recover from a shock load or process upset.

Heterotrophic microbes, on the other hand, are organisms, typically found in aerobic and anoxic systems, that derive their energy from consuming organic carbon compounds, using oxygen (or in the anoxic case, nitrate-bound oxygen) as part of their metabolic process. They tend to be faster-growing and generally more resilient to moderate fluctuations in load, which contributes to the comparatively quicker recovery times seen in aerobic systems.

Why does this matter for compliance outcomes? Because microbial balance is essentially the engine driving your treatment performance. If your system’s dominant microbial population isn’t well-matched to your actual influent characteristics, too much organic shock for a slow-recovering anaerobic culture, or insufficient oxygen supply for a heterotrophic-dominant aerobic system, you’ll see it directly in your effluent quality reports, and eventually in your inspection outcomes.

Anoxic vs Anaerobic vs Aerobic Treatment, Which One Do You Actually Need?

This is the question that actually matters at the end of the day. Here’s a practical way to think through it:

Choose aerobic sewage treatment if:

  • Your influent organic load is low to moderate and relatively consistent
  • You have significant space constraints and need a smaller treatment footprint
  • You need faster treatment cycles and quicker recovery from minor load variations
  • Energy cost is a manageable line item relative to your overall operating budget

Choose anaerobic wastewater treatment if:

  • Your influent is high-strength or high-organic-load in nature
  • You want to offset energy costs through biogas recovery
  • You have adequate space and can accommodate longer retention times
  • Your influent characteristics are relatively stable, minimizing the risk of shock-load disruption

Consider a hybrid or anoxic-inclusive approach if:

  • You’re facing both organic load and nitrogen removal requirements
  • Your existing system is aerobic-only or anaerobic-only but isn’t consistently hitting compliance targets
  • You’re retrofitting an older plant and need a more flexible, multi-stage design that can absorb fluctuating loads without triggering non-compliance flags
  • You want a more dependable buffer against the kind of variability that industrial effluent often brings

When it comes to reliability under fluctuating load conditions, which is the reality for most industrial plants, a well-designed hybrid system generally offers the most dependable path to consistent compliance, since it isn’t relying on a single microbial process to absorb every kind of variability your influent throws at it.

A Note on the Numbers

Throughout this article, we’ve deliberately avoided citing exact figures for BOD, COD, retention times, or efficiency percentages, and there’s a good reason for that: every ETP is different. The values and ranges referenced here are general industry indicators only. Actual performance figures for your plant will depend on your specific influent characteristics, system design, hydraulic and organic loading rates, temperature conditions, and day-to-day operating practices.

Treating any generic number as a benchmark for your own plant can be misleading, and in a compliance context, misleading assumptions are exactly what create risk. If you want to understand where your plant genuinely stands relative to CPCB and SPCB norms, the most reliable path is a plant-specific assessment, not a generic industry figure.

This is exactly the kind of clarity Team One Biotech’s bioremediation experts can provide, a detailed look at your actual influent profile, existing infrastructure, and compliance gaps, so your treatment decisions are based on your plant’s reality rather than general assumptions.

FAQs

Is aerobic or anaerobic treatment better for compliance with CPCB norms?

Neither is universally “better”, it depends on your influent load and design. Aerobic sewage treatment often performs more predictably for low-to-moderate organic loads, while anaerobic wastewater treatment is generally more effective for high-strength effluent. Many plants achieve the most dependable CPCB and SPCB compliance through a hybrid system that combines both approaches.

Can a plant use both aerobic and anaerobic treatment together?

Yes, and many modern ETPs do exactly this. A common configuration uses anaerobic treatment as a first stage to handle high organic loads and generate biogas, followed by aerobic (and often anoxic) stages for further polishing and nitrogen removal before final discharge.

What is the role of an anoxic tank in a sewage treatment plant?

An anoxic tank operates in a low-oxygen environment specifically to support denitrification, the conversion of nitrates into nitrogen gas, which helps plants meet nutrient-related discharge norms alongside conventional BOD and COD reduction targets.

How do heterotrophic microbes differ from anaerobic microbes in treatment performance?

Heterotrophic microbes generally operate in aerobic and anoxic environments, tend to be faster-growing, and recover more quickly from load fluctuations. Anaerobic microbes operate without any oxygen, work through a multi-stage biological pathway, and tend to be slower-growing and more sensitive to shock loads, though they offer the added benefit of biogas generation.

Making the Right Call for Your Plant

Choosing between aerobic sewage treatment, anaerobic wastewater treatment, or a hybrid anoxic-inclusive design ultimately comes down to a handful of decision factors:

  • Your load profile, how strong and how variable is your influent, realistically?
  • Your space availability, are you working within a fixed retrofitted footprint, or do you have room to expand?
  • Your energy budget, can you absorb the ongoing demand of an aerobic system, or would biogas recovery meaningfully help your bottom line?
  • Your compliance risk tolerance, how much buffer do you need against shock loads and inspection uncertainty?
  • Your manpower and O&M capacity, do you have the skilled staff to manage a more complex multi-stage system, or do you need something more straightforward to operate day to day?

There’s no universally “correct” answer here, only the answer that’s correct for your specific plant. And getting that answer right the first time is far less costly, in every sense, than retrofitting a poorly matched system after a compliance failure.

If you’re weighing this decision right now, whether you’re designing a new ETP from scratch, troubleshooting an underperforming system, or trying to figure out why your current setup isn’t holding up under inspection, Team One Biotech’s bioremediation experts are ready to help. From plant-specific assessments to customized bioaugmentation and treatment optimization solutions, we work directly with plant managers and engineers to build treatment systems that hold up under real operating pressure, not just on paper. Reach out to explore what a properly matched aerobic, anaerobic, or hybrid treatment solution could do for your compliance standing and your operating costs.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!
Scan the code