Hospital Wastewater Treatment: Why Healthcare Facilities Need Dedicated ETP Systems

A busy government hospital in Lucknow or a sprawling private medical complex in Hyderabad. Thousands of patients pass through every week. Surgeries happen around the clock. Dialysis units run in shifts. Oncology wards administer chemotherapy. And from every one of these activities, water flows out, carrying with it a chemical and biological burden that most people never think about.

This is not ordinary wastewater. What leaves a hospital through its drainage network is a complex mixture of blood, body fluids, residual pharmaceuticals, heavy metals from imaging chemicals, disinfectants, antibiotic compounds, and, critically, drug-resistant microbial organisms. This “toxic cocktail,” as environmental engineers who work in this space often call it, finds its way into municipal sewage lines, open drains, and, in far too many cases, directly into local water bodies without meaningful treatment.

For communities living near these facilities, especially in India’s densely populated urban corridors, this is not an abstract environmental concern. It is a daily, silent public health crisis.

Why Hospital Wastewater Is Not Like Industrial Wastewater
Why Hospital Wastewater Is Not Like Industrial Wastewater

Most EHS managers working in pharma, dairy, food processing, or paper manufacturing already understand effluent treatment. You manage BOD, COD, TSS, pH. You run your ETPs, maintain compliance records, and file reports with your State Pollution Control Board (SPCB). That experience is valuable, but it does not fully prepare you for the unique complexity of healthcare effluent.

Here is what makes Hospital Wastewater Treatment fundamentally different:

  • Pharmaceutical Residues: Patients excrete a significant fraction of the drugs they consume. Antibiotics, hormones, cytotoxic agents, and analgesics enter the wastewater stream in concentrations ranging between 0.01–100 micrograms per litre depending on the drug and ward type. Conventional biological treatment units are not designed to break these down.
  • Antimicrobial Resistance (AMR) Genes: This is the sleeper issue that’s now getting serious attention from the World Health Organization. Hospital wastewater is a known hotspot for AMR gene transfer. When resistant organisms and genetic material pass into water bodies, they seed environmental reservoirs for superbugs. The Yamuna, Ganga, and Musi rivers have all shown alarming AMR profiles in research conducted over the last decade.
  • Pathogenic Load: Unlike industrial effluent, hospital wastewater carries active pathogens, bacterial, viral, and fungal. Without proper disinfection stages, these organisms survive into receiving water bodies. The BOD of hospital wastewater typically ranges between 150–350 mg/L, and COD can run anywhere from 250–600 mg/L depending on facility type and case mix.
  • Variable Flow and Composition: A textile mill produces a fairly predictable effluent stream. A hospital does not. Morning OPD hours, ICU operations, dialysis sessions, and laundry peaks create wide variation in both volume and pollutant load, sometimes within the same 24-hour period.

This variability is one reason generic ETPs routinely underperform in healthcare settings.

The Regulatory Picture in India: CPCB and NGT Are Watching
The Regulatory Picture in India: CPCB and NGT Are Watching

The Central Pollution Control Board (CPCB) has issued specific discharge standards for hospitals under the Environment Protection Act, and the Bio-Medical Waste Management Rules, 2016 (amended 2018) govern liquid waste disposal. Many states have gone further, Maharashtra, Karnataka, Tamil Nadu, and Delhi have SPCB-level directives that impose tighter standards on larger healthcare establishments.

The National Green Tribunal (NGT) has become increasingly assertive. In multiple landmark orders, the NGT has penalized healthcare institutions, including government hospitals, for discharging untreated or inadequately treated effluent into municipal drains and water bodies. Fines have ranged from lakhs to crores, and in some cases, facility operations have been restricted.

And yet, a 2023 audit by environmental researchers across Tier-1 and Tier-2 Indian cities found that a substantial proportion of hospitals, particularly nursing homes, smaller private facilities, and district hospitals, either lack functional ETPs or operate systems that were designed for domestic sewage rather than clinical-grade effluent. This is a compliance gap waiting to become a liability.

If you are an administrator or EHS manager responsible for a healthcare facility, the question is not whether your facility will face scrutiny. It is whether you will be ready when it does.

If your current ETP setup was not specifically designed for hospital wastewater, this is the right time to request a professional Wastewater Audit from Team One Biotech. Our team will evaluate your current system, identify gaps in CPCB compliance, and give you a clear action plan, no obligations.

What a Dedicated ETP for Hospitals Actually Looks Like
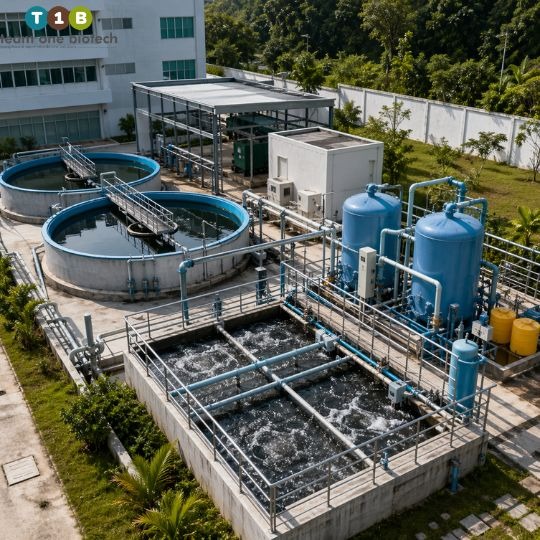
What a Dedicated ETP for Hospitals Actually Looks Like

A properly engineered hospital ETP is a multi-stage system that addresses the specific threat vectors of healthcare effluent. Here is a simplified breakdown of what that looks like in practice:

Primary Treatment

Screening, grit removal, and equalization. The equalization tank is particularly important in healthcare applications, it buffers the wide flow variations mentioned earlier and ensures that downstream biological stages receive a consistent load.

Secondary Biological Treatment

This is where the heavy lifting happens. Activated sludge processes, Moving Bed Biofilm Reactors (MBBR), or Sequencing Batch Reactors (SBR) are common choices. BOD and COD reduction at this stage can bring levels down to 30–100 mg/L and 100–250 mg/L respectively, when properly sized and operated.

Tertiary and Advanced Treatment

Given the pharmaceutical and AMR concerns unique to hospitals, tertiary treatment is non-negotiable. This typically includes:

  • Coagulation and flocculation for suspended solids
  • Activated carbon adsorption for pharmaceutical residue removal
  • Chlorination or UV disinfection for pathogen kill
  • Ozonation in high-specification systems

Sludge Management

Hospital ETP sludge is classified as hazardous. It requires proper dewatering, containment, and disposal in line with Bio-Medical Waste Rules, a step that many facilities overlook when setting up basic treatment units.

Technical Deep Dive: Why Bioremediation Outperforms Traditional Chemical Dosing

This is where things get genuinely interesting, and where the gap between legacy practice and modern science becomes very clear.

Traditional hospital ETPs lean heavily on chemical treatment: coagulants like alum or ferric chloride, hypochlorite for disinfection, and acid/alkali for pH adjustment. These approaches work in narrow parameters. But they have well-documented limitations in healthcare applications:

  • They do not biodegrade pharmaceuticals. Chemical coagulation removes suspended matter. It does not break down dissolved drug molecules, hormones, or AMR genetic material.
  • They generate high volumes of chemical sludge, which itself becomes a disposal burden.
  • Operating costs are persistent and high. Chemical procurement, handling, and dosing add recurring expenditure running into lakhs per year for medium-to-large facilities.
  • System sensitivity to load variation means that during peak hours, chemical dosing systems can underperform, leading to compliance breaches.

Bioremediation, Team One Biotech’s core area of expertise, takes a fundamentally different approach. Rather than adding synthetic chemicals to suppress or precipitate pollutants, bioremediation introduces specialized microbial consortia that actively metabolize contaminants.

In hospital wastewater applications, this means:

  • Pharmaceutical degradation at the molecular level. Carefully selected microbial strains can break down antibiotic residues, hormonal compounds, and certain cytotoxic metabolites, converting them into water, carbon dioxide, and biomass rather than leaving them in altered chemical form.
  • AMR risk reduction. Research increasingly supports that robust biological treatment with diverse microbial communities can suppress the proliferation of resistant organisms. A healthy microbial ecosystem outcompetes pathogens and ARB (antibiotic-resistant bacteria) for resources.
  • Lower sludge generation. Biological processes typically produce 30–50% less sludge than comparable chemical treatment systems, a significant operational and disposal cost advantage.
  • Greater operational stability. Well-established biofilm and suspended growth systems can tolerate load fluctuations better than chemical dosing when properly maintained.
  • CPCB-compatible output. With the right system design, bioremediation-based ETPs can consistently achieve treated effluent quality within CPCB General Standards for discharge.

Team One Biotech’s proprietary microbial formulations have been deployed across healthcare, pharmaceutical, and industrial facilities across India. Our approach is site-specific: we do not sell a generic solution because hospital wastewater in Mumbai does not look the same as hospital wastewater in Bhopal.

Want to understand whether a bioremediation-based ETP could replace or supplement your existing system? Talk to our technical team for a Custom Bioremediation Plan tailored to your facility’s effluent profile.

Common Mistakes Healthcare Facilities Make With Their ETPs
Common Mistakes Healthcare Facilities Make With Their ETPs

A few patterns come up repeatedly when our team evaluates existing hospital wastewater systems:

  • Undersizing the equalization tank. This single error leads to more ETP performance failures than almost any other design flaw.
  • Treating the ETP as a one-time capital project rather than a living system that requires monitoring, microbial replenishment, and periodic process adjustment.
  • Ignoring the pharmacy and laundry streams. These two sources often carry disproportionately high pharmaceutical and surfactant loads and need targeted pre-treatment before they reach the main ETP.
  • Relying on third-party lab reports without in-house monitoring. By the time an external lab flags a problem, a compliance breach has already occurred.
  • Not planning for the NGT audit cycle. Regulatory bodies are increasingly coordinating surprise inspections, and facilities that rely on compliance-by-paperwork rather than compliance-by-performance are the most exposed.

Liquid Medical Waste Management: The Overlooked Last Mile

Even facilities with reasonably functional ETPs often have a blind spot around liquid medical waste management at the source. Properly segregating and pre-treating high-risk liquid streams, from pathology labs, operation theatres, dialysis units, and isolation wards, before they enter the main drainage network is both a regulatory requirement and a practical necessity.

Without source-level segregation protocols, a single high-load event (say, a dialysis session’s concentrated effluent or a pathology lab’s chemical waste) can overwhelm downstream biological treatment stages. Our recommendation: treat liquid medical waste management as a facility-wide discipline, not just an ETP engineering problem.

The Business Case for Getting This Right

Beyond compliance, there is a straightforward business case. Hospitals that invest in properly designed, professionally maintained dedicated ETP systems typically see:

  • Reduced risk of NGT/SPCB penalties, which can range from Rs. 5 lakh to Rs. 5 crore depending on severity and jurisdiction
  • Lower long-term operating costs compared to chemical-heavy legacy systems
  • Stronger positioning for NABH accreditation and green hospital certifications
  • Reputational protection in an era when environmental accountability is increasingly a factor in institutional trust

This is not a regulatory checkbox exercise. It is an investment in the long-term operational resilience of your facility.

Ready to move from compliance risk to compliance confidence? Team One Biotech offers end-to-end support, from initial Wastewater Audit to system design, microbial supply, and ongoing monitoring. Contact our EHS advisory team today and take the first step toward a fully compliant, bioremediation-powered hospital ETP.

Disclaimer: The values mentioned in this article, including BOD, COD, flow rates, cost ranges, and treatment performance benchmarks, are general estimates and industry benchmarks. Actual requirements and performance metrics vary based on individual ETP design, specific facility loads, local regulatory conditions, and operational parameters. Always consult a qualified EHS engineer or licensed ETP designer before making facility-specific decisions.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!
Paper and Pulp Effluent Treatment: How Biological Cultures Cut Colour and BOD

If you manage an ETP at a paper or pulp mill in India, you already know the feeling. The consent conditions sit on your desk. The CPCB ambient water quality norms have been tightened. Your State Pollution Control Board inspector is due next quarter, and the treated effluent flowing out of your clarifier still carries that unmistakable brown tint.

Paper mill effluent treatment is not a checkbox exercise anymore. In the current regulatory climate, with the National Green Tribunal actively penalizing non-compliant industrial units and SPCBs empowered to issue closure notices, the margin for error at your ETP is essentially zero. Real-time online monitoring systems (OCEMS) now transmit your treated effluent data directly to CPCB servers. There is no hiding a bad day at the plant.

The operators who are sleeping soundly at night are the ones who have moved beyond conventional treatment and invested in understanding the biology of their wastewater. This post explains exactly how Biological Cultures for Paper and Pulp Effluent Treatment are now doing what chemicals and physical processes alone never could: breaking down the stubborn organic load in paper and pulp effluent and delivering consistent compliance, month after month.

Why Paper Mill Effluent Is Among the Hardest Industrial Wastewaters to Treat

Why Paper Mill Effluent Is Among the Hardest Industrial Wastewaters to Treat

Before we discuss solutions, we need to respect the problem. Paper mill effluent treatment is uniquely challenging, and anyone who tells you otherwise is selling something oversimplified.

The core difficulty comes down to three factors:

1. Lignin-based colour is chemically recalcitrant

Lignin is the structural polymer that gives wood its rigidity. During the pulping process, whether kraft, sulphite, or mechanical, lignin is broken down and released in large quantities into the process water. The resulting effluent carries complex, high-molecular-weight chromophores that give paper mill discharge its characteristic dark brown to black colour.

These compounds do not respond well to conventional biological treatment because most common heterotrophic bacteria simply lack the enzymatic machinery to attack aromatic ring structures. Chlorine bleaching in older mills adds chlorinated lignin derivatives to the mix, further complicating biodegradation and potentially pushing you into the territory of acute aquatic toxicity.

2. High and variable Organic Loading Rates (OLR)

Paper mills do not produce uniform effluent. A mill running 100% recycled fibre will generate a different effluent profile than one using virgin wood pulp. OLR can swing dramatically based on:

  • Grade of paper being produced (tissue, kraft board, newsprint, writing paper)
  • Seasonal raw material variations
  • Machine wash-down cycles and felt changes
  • Chemical recovery system upsets

This variability is the enemy of a stable biological treatment system. A conventional activated sludge process tuned for average conditions will underperform on peak-load days, precisely the days when you can least afford it.

3. The BOD:COD ratio problem

Healthy aerobic digestion processes thrive on a favourable BOD:COD ratio. In paper mill effluent, the presence of non-biodegradable COD, principally from lignin and its derivatives, can push the BOD:COD ratio to values where standard microbial communities struggle to deliver meaningful COD removal. You can have perfectly functioning biomass and still fail your discharge norms because the recalcitrant fraction passes through untouched.

The Biological Solution: Bio-Augmentation for Lignin Degradation and BOD Reduction

The Biological Solution: Bio-Augmentation for Lignin Degradation and BOD Reduction

This is where the science becomes genuinely powerful, and where paper mill effluent treatment has seen the most significant advances in the last decade.

Bio-augmentation refers to the deliberate introduction of selected microbial strains or consortia into an existing biological treatment system. These are not generic cultures. For paper and pulp applications, the relevant organisms are typically:

  • White-rot fungi such as Phanerochaete chrysosporium and related basidiomycetes, which produce lignin peroxidase and manganese peroxidase, extracellular enzymes specifically evolved to depolymerise lignin
  • Laccase-producing bacteria including select Bacillus, Pseudomonas, and Streptomyces strains capable of oxidising phenolic compounds
  • Specialised heterotrophic consortia that efficiently convert the lower-molecular-weight fragments produced by the above into carbon dioxide and water through conventional aerobic metabolism

The process works in a cascade. Lignin peroxidase and laccase break the high-molecular-weight chromophores into smaller, more biodegradable units. Downstream heterotrophic bacteria then mineralise these fragments, reducing both colour and soluble BOD simultaneously.

What does this look like in practice?

When properly applied and acclimatised to your specific effluent, a well-designed bio-augmentation programme targeting paper mill wastewater can be expected to deliver:

  • BOD reduction in the range of 85% to 95%
  • COD reduction in the range of 70% to 88%
  • Colour reduction (ADMI units) in the range of 60% to 80%

Important Disclaimer: The numerical ranges cited in this article are general performance benchmarks drawn from field experience across multiple installations. Actual results will vary based on your specific ETP design, hydraulic retention time (HRT), sludge retention time (SRT), influent chemistry, temperature, and operational discipline. Contact Team One Biotech for a site-specific performance assessment before setting internal targets.

Paper Mill Effluent Treatment in the Indian Context: The Challenges Nobody Talks About

Paper Mill Effluent Treatment in the Indian Context: The Challenges Nobody Talks About

Global case studies are useful. Indian field realities are what matter when your phone rings at 2 AM because the final effluent is failing colour.

Seasonal temperature swings

Biological treatment systems are temperature-sensitive. In northern and central India, effluent temperatures in January can drop to 12°C to 16°C, dramatically slowing microbial metabolism. The same system in May may see influent temperatures exceeding 38°C to 42°C, stressing mesophilic organisms and risking process upset. A culture formulation that works in Maharashtra in February may behave very differently in Uttarakhand in December.

Effective bio-augmentation for Indian mills must account for this range. The microbial consortia supplied should demonstrate metabolic activity across a broad thermal window, and dosing protocols should be adjusted seasonally, not set once and forgotten.

Raw material and process variability in Indian mills

Many Indian paper mills operate on a mixed furnish, recycled OCC, agricultural residues like bagasse and wheat straw, and imported pulp. This creates an influent with a compositional complexity that European or North American mills rarely encounter. Bagasse-based effluents carry different hemicellulose fractions and silica loading than wood-based effluents. Your biological culture needs to be acclimated to your specific substrate chemistry, not a generic paper mill profile.

MLSS management under load shock

Maintaining Mixed Liquor Suspended Solids (MLSS) within the target range during production upsets is a persistent operational challenge. When a mill runs a grade change or recovers from a machine breakdown, the OLR spike that hits the aeration tank can crash a fragile biomass within 24 to 48 hours, setting back your compliance position by weeks.

Bio-augmented systems, particularly those using spore-forming bacterial strains, show significantly higher resilience to OLR shocks than conventional activated sludge alone. Dormant spores survive the upset and germinate rapidly once conditions stabilise, shortening recovery time considerably.

The push toward Zero Liquid Discharge

ZLD is no longer a future aspiration for many Indian paper mills, it is a regulatory condition of consent in several states. Biological pre-treatment quality directly determines the efficiency and cost of the downstream ZLD train (ultrafiltration, RO, MEE, and ATFD). Poor COD and colour removal at the biological stage means your RO membranes foul faster, your evaporator scaling increases, and your overall cost per kilolitre of recovered water rises sharply.

Investing in high-performance biological cultures is not just a compliance decision. In a ZLD framework, it is an operational cost management decision.

How Team One Biotech’s Biological Cultures Are Formulated for Paper Mill Applications

At Team One Biotech, our approach to paper mill effluent treatment begins with understanding that no two mills are identical. Our process:

Step 1, Influent characterisation. We analyse your raw effluent for BOD, COD, colour (ADMI), TSS, pH, TDS, sulphate, chloride, and the BOD:COD ratio. This tells us the biodegradable fraction we are working with and the recalcitrant COD we need to attack enzymatically.

Step 2, Culture selection and acclimation. Based on your effluent chemistry, we select and acclimate a consortium specifically prepared for your substrate. This is not an off-the-shelf product, it is a living, engineered microbial community tuned to your wastewater.

Step 3, Dosing protocol and integration. We provide a structured seed dosing protocol, typically delivered over a phased startup period of two to four weeks, followed by a maintenance dosing regime. Our technical team supports your plant operators through the process.

Step 4, Performance monitoring. We recommend a monitoring schedule targeting BOD, COD, MLSS, SVI, and colour at defined intervals through the startup phase to verify culture establishment and performance trajectory.

The result is a biological system that is more robust, more consistent, and better positioned to absorb the operational variability inherent in Indian paper mill production.

Practical Guidance for ETP Operators Running Paper Mill Wastewater

Practical Guidance for ETP Operators Running Paper Mill Wastewater

Whether or not you are currently using bio-augmentation, the following operational disciplines will strengthen any paper mill effluent treatment system:

  • Monitor your F/M ratio regularly. Food-to-microorganism ratio is your early warning system for biomass health. A declining F/M in the face of consistent loading often signals a culture quality issue before it becomes a compliance event.
  • Maintain dissolved oxygen in the aeration basin between 2.0 and 3.5 mg/L. Lignin-degrading organisms are obligate aerobes with high oxygen demand. Inadequate DO is the single most common reason bio-augmentation programmes underperform.
  • Track SVI (Sludge Volume Index) weekly. Bulking sludge is a frequent consequence of low F/M and poor selector design in paper mill ETPs. High SVI will compromise your secondary clarifier and push TSS into your final effluent.
  • Avoid sudden pH swings. Maintain aeration basin pH between 6.8 and 7.6. Paper mill effluents can be acidic or alkaline depending on the process stage contributing to the drain. Buffering capacity matters.
  • Document OLR trends. If you can predict the days your OLR spikes, grade changes, week-end startups, rainy-season dilution events, you can pre-dose your biological cultures to have elevated biomass activity ready before the shock arrives, rather than reacting after.

The Bottom Line for EHS Managers

Colour and BOD in paper mill effluent are not problems that chlorine dosing or coagulant overdosing will solve sustainably. They are fundamentally biological problems that require biological solutions, specifically, the right microbial consortia, properly acclimated, correctly integrated, and operationally supported.

With CPCB and SPCB enforcement intensifying and ZLD mandates expanding, the question is no longer whether to invest in biological treatment performance. The question is whether you are getting the best possible biological performance from your current system.

If you are not consistently achieving your consent conditions, or if you are achieving them on borrowed time through chemical patches, it is time for a professional audit of your ETP’s biological health.

Team One Biotech offers site-specific ETP audits and customised microbial culture formulations for paper and pulp mills across India. Our technical team works directly with your plant operators, not just your corporate procurement team, because we understand that compliance is won or lost at the plant floor level.

Reach out to Team One Biotech today to schedule your consultation. Bring your last three months of influent and effluent data, and we will bring the science.

This Blog is intended for informational purposes for ETP/STP operators and EHS professionals. All performance ranges cited are general benchmarks only and do not constitute guaranteed outcomes. Actual treatment performance is dependent on site-specific conditions including ETP design, hydraulic and sludge retention times, influent chemistry, temperature, and operational management. Team One Biotech recommends a site-specific technical assessment before implementing any biological treatment programme.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!
Tannery Wastewater Treatment: Removing Chromium and Sulfide with Bioremediation

If you manage environmental health and safety at a tannery unit in Kanpur, Ambur, or Ranipet, you already know what it feels like to walk into your ETP shed at 6 AM and wonder whether today is the day an SPCB inspection team shows up unannounced. You know the weight of being responsible for what goes into the drain, and what that means for a river downstream, for a community nearby, and for your facility’s operating license.

Bio Cultures for Tannery Wastewater Treatment is not a back-of-house problem. It sits at the intersection of industrial survival and environmental accountability. The leather industry contributes billions to India’s export economy and employs millions of workers, but it also produces one of the most chemically complex effluent streams in any industrial sector. Chromium. Sulfides. High BOD. Extreme pH swings. And CPCB norms that grow stricter with every revision of the Environmental Protection Act.

For EHS managers who have been navigating this pressure for years, the real question is no longer whether to treat, it is how to treat smarter, at lower cost, with less sludge, and with outcomes that actually hold up during third-party audits. That is where bioremediation is changing the conversation.

What Makes Tannery Effluent So Difficult to Treat

What Makes Tannery Effluent So Difficult to Treat

Before talking solutions, it helps to be honest about the problem, because too many vendors oversimplify it.

Traditional chrome tanning processes use trivalent chromium (Cr III) as a tanning agent. Under most ETP conditions, this is manageable. The challenge emerges when your ETP is not optimized: pH fluctuations, oxidizing conditions, and high redox potential can convert Cr(III) to hexavalent chromium (Cr VI), a compound classified as a carcinogen under multiple international standards and explicitly listed under CPCB’s hazardous waste rules.

Indian discharge norms for total chromium in tannery effluent are set at 2 mg/L for inland surface water discharge and 1 mg/L for land application under General Standards for Discharge of Environmental Pollutants (Schedule VI of the Environment Protection Rules, 1986). Facilities operating in river-sensitive zones, particularly those near the Ganga basin in Uttar Pradesh or Palar River basin in Tamil Nadu, face even tighter scrutiny under NGT directives and state-level notifications.

Then there is the sulfide problem. Beam-house operations, liming, de-hairing, and soaking, generate effluent with sulfide concentrations that can range from several hundred to well over a thousand mg/L, depending on process chemistry and hides processed per day. Sulfide in untreated or undertreated discharge creates toxic hydrogen sulfide gas, causes acute aquatic toxicity, and contributes to the foul odor conditions that draw community complaints and media attention to tannery clusters.

The conventional response has been chemical precipitation, adding ferrous sulfate or lime to crash chromium out of solution, and using aeration or chlorination to oxidize sulfide. These methods work, to a point. But they generate enormous volumes of chemical sludge, require significant reagent procurement and storage, and often struggle to consistently hit discharge limits when influent quality fluctuates, which in tanneries, it does frequently.

The Bioremediation Shift: Microbes That Work Where Chemicals Fall Short

Bioremediation in tannery wastewater treatment is not a new concept, but its practical implementation in Indian industrial ETPs has accelerated significantly in the last several years, driven partly by the push for ZLD compliance and partly by the economics of chemical sludge disposal.

What Team One Biotech brings to this domain is a library of specialized microbial consortia that have been selected and conditioned specifically for high-chromium, high-sulfide industrial environments. These are not off-the-shelf bacterial cultures from a generic microbiology catalogue. They are strains that have been adapted to perform under the high-salinity, high-toxicity conditions that are typical of tannery ETPs in the Kanpur cluster or the Ambur-Ranipet belt.

The core distinction between chemical treatment and bio-based treatment is what happens after the contaminant is captured. Chemical precipitation immobilizes chromium in a sludge cake that must then be landfilled or treated as hazardous waste. Bioremediation does something different, and, in many ways, more elegant.

How the Microbial Mechanism Actually Works

How the Microbial Mechanism Actually Works

Chromium Sequestration Through Microbial Reduction

Certain strains of chromate-reducing bacteria, including species from genera such as Bacillus, Pseudomonas, and Desulfovibrio, are capable of enzymatically reducing hexavalent chromium (Cr VI) to the far less toxic trivalent form (Cr III). This reduction typically occurs through electron transfer driven by organic carbon in the effluent, which means the bacteria are using the wastewater’s own chemistry as fuel.

Once reduced, Cr(III) can be further immobilized through biosorption, a process where microbial cell walls, with their negatively charged surface groups, bind to metal cations and remove them from solution. The result is chromium locked into a biomass matrix rather than floating in solution or leaching from a chemically unstable sludge cake.

In optimized bioaugmentation programs, total chromium reduction efficiencies in tannery ETPs have been reported in the range of 70% to 90% in the biological treatment stage alone, before any final polishing. Specific results depend on influent loading, hydraulic retention time, microbial acclimatization period, and the baseline performance of the existing ETP. These figures are benchmarks; actual outcomes vary from plant to plant and require site-specific evaluation.

Sulfide Oxidation Through Microbial Metabolism

The sulfide challenge is addressed through a different but equally elegant mechanism. Sulfur-oxidizing bacteria, which naturally thrive in environments rich in reduced sulfur compounds, convert sulfide (S²⁻) to elemental sulfur and ultimately to sulfate (SO₄²⁻), which is far less toxic and odorous.

In a bioaugmented ETP, this process is accelerated and stabilized compared to what happens in a conventional aeration system. The biological pathway does not require continuous addition of chemical oxidants, and it does not produce the chlorinated by-products associated with hypochlorite-based sulfide control.

Sulfide removal efficiencies in augmented biological treatment stages typically fall in the range of 75% to 92% under stable operating conditions. Again, these are generalized ranges. Actual performance depends on your specific influent sulfide load, reactor configuration, and dissolved oxygen management.

The Indian Industry Context: Why This Matters More Here

The Indian Industry Context: Why This Matters More Here

Indian tannery clusters operate at a scale that makes chemical reagent costs a serious line item. A mid-sized tannery processing 500 to 1,000 hides per day can spend significantly on ferrous sulfate, lime, and acid for pH adjustment alone, before accounting for the cost of sludge disposal, which in hazardous waste categories under the Hazardous and Other Wastes (Management and Transboundary Movement) Rules, 2016 requires authorized TSDF facilities.

Bioaugmentation does not eliminate chemical treatment entirely, most ETPs will continue to use some chemical precipitation for rapid chromium knockdown, but it substantially reduces reagent consumption and sludge volume. Facilities that have integrated microbial treatment into their process have reported reductions in chemical sludge generation in the range of 30% to 55%, though this varies considerably depending on baseline chemistry and process configuration. These figures are indicative and should not be assumed to apply universally without a proper site assessment.

From a ZLD compliance standpoint, reducing the contaminant load entering your RO or evaporation systems also extends membrane life and reduces scaling, which translates directly into lower maintenance costs and longer intervals between system overhauls.

For EHS managers under SPCB scrutiny or NGT compliance orders, particularly those operating in notified zones around the Ganga, Yamuna, or Palar river basins, demonstrating a biological treatment layer in your ETP is increasingly viewed favorably during compliance reviews as evidence of best-available-technology adoption.

If your facility is currently navigating a compliance notice or preparing for a renewal inspection, this is exactly the kind of documented process improvement that regulators want to see. Contact Team One Biotech for a no-obligation audit of your current ETP’s biological treatment potential.

Integrating Bioremediation Into Your Existing ETP: A Practical Path

Retrofitting an existing tannery ETP for bioaugmentation does not require demolishing what you have. The approach is additive, not disruptive. Here is how the implementation typically unfolds:

  • Baseline ETP Assessment, Team One Biotech’s technical team evaluates your current influent parameters: chromium speciation, sulfide load, BOD/COD ratio, pH profile, and sludge generation rates. This gives you a data-backed starting point rather than a guess.
  • Microbial Strain Selection, Based on the assessment, a specific consortium is recommended. High-chromium environments need strains with proven chromate-reduction capacity; high-sulfide environments need dominant sulfur oxidizers. The formulation is not one-size-fits-all.
  • Seeding and Acclimatization, Microbial cultures are introduced into your existing biological treatment tanks, typically the aeration tank or equalization basin. An acclimatization period of two to four weeks is standard before performance benchmarks are meaningful.
  • Monitoring and Optimization, Effluent quality is tracked at defined intervals. Dosing frequency and quantity are adjusted based on observed performance. This is not a one-time application; it is a managed biological process.
  • Documentation for Compliance, Treatment logs, influent and effluent data, and microbial performance records are maintained in a format suitable for SPCB submissions and third-party environmental audits.

Speak to Team One Biotech’s technical team today to understand whether your ETP’s existing infrastructure is ready for bioaugmentation, or what modifications might be needed to maximize outcomes.

Long-Term ROI and the Environmental Legacy You Leave Behind

The economics of bioremediation in tannery wastewater treatment improve over time. In the first year, the primary returns are in chemical savings, reduced sludge disposal costs, and improved consistency in hitting discharge limits. Over a three-to-five year horizon, the return also includes reduced equipment wear on downstream systems, lower compliance-related legal and administrative costs, and the reputational capital that comes with demonstrably responsible effluent management.

For tannery units in clusters like Kanpur, where the Ganga Action Plan and successive NGT orders have made the leather industry a focal point of environmental scrutiny, this is not a peripheral benefit. It is a strategic necessity.

The EHS managers who are building facilities that will still be operating a decade from now are not just chasing compliance thresholds. They are making a considered decision about the kind of industrial legacy their facility leaves in the local ecosystem, the local water table, and the communities around them.

Bioremediation is one of the most credible tools available to make that decision count.

To explore a site-specific bioremediation strategy for your tannery ETP, reach out to Team One Biotech for a detailed technical audit and customized treatment recommendation.

Disclaimer: All numerical values, reduction percentages, and concentration ranges cited in this article are general industry benchmarks compiled from published literature and field observations. Actual results vary from plant to plant and depend on influent characteristics, ETP design, operational parameters, and site-specific conditions. These figures should not be used as guaranteed performance indicators without a formal site assessment.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!
Sugar Mill Effluent Under Pressure: Biological Solutions for High-Load Shocks and CPCB Compliance

Every October, the same alarm starts ringing across sugar belt states,  Uttar Pradesh, Maharashtra, Karnataka, Tamil Nadu. The cane arrives faster than any ETP was designed to absorb. Clarifier overflow. Sludge turning grey. COD spiking to levels that would make an inspector reach for his clipboard before he even finishes his chai.

For an EHS manager standing between a 24-hour production cycle and an SPCB show-cause notice, this is not a theoretical problem. This is a recurring operational crisis,  one that can trigger NGT fines, plant shutdowns, and reputational damage that lingers long after the season ends.

The hidden cost of non-compliance is rarely just the penalty. It is the productivity loss during corrective shutdowns, the cost of emergency chemical dosing, the overtime hours troubleshooting a biological system that was never built for the load it is receiving. And increasingly, with CPCB tightening effluent discharge standards under the Environment Protection Act and NGT maintaining active oversight on Red Category industries, the margin for error has narrowed to almost nothing.

Biological treatment for sugar mills done right is not a backup plan. It is the foundation of a compliant, resilient sugar mill operation.

What Makes Sugar Mill Effluent a Biological Treatment Challenge

Sugar mill effluent is not ordinary wastewater. It is a concentrated, chemically complex mix that includes washings from cane preparation, barometric condenser water, juice spillage, molasses residues, and floor washdowns from the boiling house. During peak crushing, this mix arrives in volumes and concentrations that fluctuate dramatically,  sometimes hour to hour.

The core parameters that drive treatment difficulty:

COD loads typically range from 2,000–15,000 mg/L depending on the unit operation and dilution, though values outside this range are documented during startup and peak throughput.

BOD values commonly fall in the 800–6,000 mg/L range in raw influent, with significant variation tied to molasses carryover and process leakages.

pH swings across 4.5–9.5 in untreated streams, driven by fermentation of residual sugars in collection channels and alkaline process water from sulphitation.

Suspended solids, including bagasse fines and soil from cane washing, regularly read between 500–3,000 mg/L in raw streams entering primary treatment.

Colour, primarily from melanoidins,  the compounds formed when amino acids react with reducing sugars under heat,  is one of the most persistent treatment challenges and a visible indicator of non-compliance even when COD numbers look acceptable.

All values expressed throughout this article represent general industry ranges. Actual figures vary significantly based on plant-specific machinery, cane variety, feedstock quality, process water management, and ETP/STP design configuration. Site-specific characterisation is essential before any treatment design decision.

The Science Behind Biological Degradation of Sugar Mill Wastewater

The Science Behind Biological Degradation of Sugar Mill Wastewater

Why Microbial Consortia Outperform Chemical Treatment Alone

Chemical treatment,  coagulation, flocculation, lime dosing,  addresses the physical load. It does not address the dissolved organic fraction that drives your COD reading and determines whether your discharge will pass consent conditions.

That work is done by microorganisms. Specifically, by diverse consortia of aerobic heterotrophs, facultative anaerobes, and specialised fermenters that collectively degrade the complex organic matrix of sugar mill effluent.

The primary substrates these organisms are breaking down include:

Sucrose, glucose, and fructose,  rapidly consumed fermentable sugars that provide a fast-acting BOD spike in the early stages of biological treatment.

Polysaccharides and starches,  from bagasse and cane pith, which require cellulolytic and amylolytic bacterial populations to hydrolyse before further degradation is possible.

Organic acids,  acetic, lactic, and butyric acids formed during fermentation of residual sugars in collection sumps and anaerobic pockets of the treatment system.

Melanoidins,  high-molecular-weight recalcitrant compounds requiring specialised peroxidase-producing fungi and bacteria, such as Phanerochaete-type organisms or ligninolytic populations, that many generic microbial seed cultures simply do not contain in sufficient density.

The Anaerobic-Aerobic Sequence: Getting the Biology Right

Well-designed biological treatment of sugar mill effluent typically follows a staged approach:

Anaerobic pretreatment,  UASB reactors or anaerobic lagoons reduce the gross organic load, converting 55–70% of incoming COD to biogas and reducing the aerobic stage loading. COD reduction across the anaerobic stage typically falls in the 50–65% range.

Aerobic biological treatment,  Extended aeration, activated sludge, or sequencing batch reactors (SBRs) handle the residual BOD and COD. Well-seeded and maintained aerobic systems achieve BOD reductions of 88–96% across the combined treatment train.

Tertiary polishing,  Filtration, constructed wetlands, or advanced oxidation handles colour and residual suspended solids before ZLD or discharge.

The biology only performs at this level when the microbial population is correctly seeded, adequately fed, and protected from shock events.

Where Operations Go Wrong, The Most Common ETP Failures in Sugar Mills

Sludge Bulking and Settleability Collapse

One of the most frequently reported operational failures in sugar mill ETPs is filamentous sludge bulking,  the proliferation of thread-like bacterial species that create a voluminous, poorly settling sludge blanket. This typically occurs when:

Carbon-to-nitrogen ratios are skewed by high sugar loads without proportional nitrogen supplementation. The ideal C:N:P ratio for aerobic biological treatment is approximately 100:5:1, but in sugar mill systems, this ratio can be thrown to 300:5:1 or worse during high-load periods.

Dissolved oxygen sags below 1.5–2.0 mg/L in aeration tanks during peak load, favouring filamentous organisms over floc-forming bacteria.

Hydraulic retention times are shortened during peak production to maintain inlet flow acceptance, starving the biological population of contact time.

The Failure of Generic Microbial Seeding

This is a pattern that repeats across sugar mills that are attempting biological recovery without specialist input. The plant inoculates with cow dung slurry or municipal sludge,  standard practice passed down through operating teams,  and then waits for the biomass to establish.

The problem is selection pressure. The microbial populations in generic seed material were never exposed to the specific substrates in sugar mill effluent,  melanoidins, complex polysaccharides, high-temperature process water. Establishment is slow, COD reduction remains in the 40–60% range instead of the 85–95% range a specialist consortium can achieve, and the plant operates in a perpetual state of marginal compliance.

Monsoon-Season Biomass Instability

Monsoon creates specific problems for sugar mill ETPs in India that are rarely addressed in treatment design documents but are felt acutely by every plant operator.

Temperature drops across aerobic tanks of 8–14°C relative to pre-monsoon conditions can reduce microbial metabolic rates by 30–50%, stretching biological treatment response times and elevating discharge COD.

Stormwater ingress dilutes mixed liquor suspended solids (MLSS),  the active biological mass,  from stable operating ranges of 2,500–4,000 mg/L down to values below 1,000 mg/L in poorly bunded facilities.

Additionally, the crushing season in northern states begins immediately post-monsoon, meaning biomass is already stressed before it faces the season’s peak organic shock.

Regulatory Pressure and ZLD,  What CPCB and NGT Are Actually Demanding

Regulatory Pressure and ZLD,  What CPCB and NGT Are Actually Demanding

Under CPCB’s effluent standards for sugar industries and the downstream pressure from NGT judgments on critically polluted areas, many large sugar mills are now operating under consent conditions that require discharge COD below 250 mg/L,  and in some states, below 150 mg/L,  into inland surface water bodies.

ZLD aspirations are growing. Several state pollution control boards have begun mandating ZLD compliance for sugar mills in water-stressed districts of Maharashtra, Rajasthan, and parts of Uttar Pradesh. ZLD shifts the entire treatment objective from effluent quality to volume reduction, a target that cannot be achieved without a stable, high-performing biological treatment stage at the base of the system.

For EHS managers preparing for SPCB renewals or NGT submissions, the biological treatment performance records , MLSS logs, SV30 data, effluent quality trends,  are no longer optional documentation. They are evidence.

Download Team One Biotech’s ETP Health Checklist for Sugar Mills,  a field-tested audit framework covering biological performance indicators, sludge management, and CPCB compliance documentation.

The Team One Biotech Approach,  Specialised Biology for Specialised Loads

Team One Biotech works with sugar mills not as a chemical supplier, but as a biological treatment partner. The difference is in the specificity of the microbial products and the depth of the technical support behind them.

The core of the approach involves:

Strain-selected microbial consortia formulated specifically for high-sucrose, melanoidin-heavy wastewater streams. These are not general-purpose cultures,  they carry cellulolytic, lipolytic, and ligninolytic populations capable of degrading the recalcitrant organic fraction that generic seed material misses.

Nutrient balancing protocols that accompany every dosing plan, addressing the N:P deficiencies that are almost universal in sugar mill treatment systems.

Biomass protection strategies ahead of the crushing season,  a pre-seeding programme that builds MLSS levels and microbial diversity before the high-load shock arrives, rather than attempting biological recovery in the middle of peak production.

Ongoing monitoring support across aerobic and anaerobic stages, with dosing adjustments tied to incoming load data rather than fixed schedules.

Team One Biotech’s product range spans industrial wastewater treatment, agricultural soil health, and aquaculture water quality,  a breadth of biological expertise that brings cross-sector learning into every site-specific solution.

Request a site audit from Team One Biotech’s technical team,  field diagnostics, effluent characterisation, and a biological treatment gap analysis built around your plant’s specific operational profile.

Moving From Firefighting to Forward Management

The sugar mill operations that achieve consistent CPCB compliance and are positioned for ZLD mandates are not necessarily those with the most capital-intensive infrastructure. They are the ones whose biological treatment is actively managed,  seeded correctly at the start of the crushing season, supported through monsoon transition, monitored through the season’s peak loads, and backed by a technical partner who understands the difference between sugar mill effluent and generic industrial wastewater.

The shift from reactive crisis management to proactive biological stability is not a technology upgrade. It is an operational philosophy, supported by the right microbial science.

Sugar mill effluent treatment has a biological solution. The season does not have to be a crisis every year.

Contact Team One Biotech today for a customised microbial dosage plan built around your mill’s effluent profile, crushing schedule, and compliance targets. Treatment that works with your biology, not against your operational calendar.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!
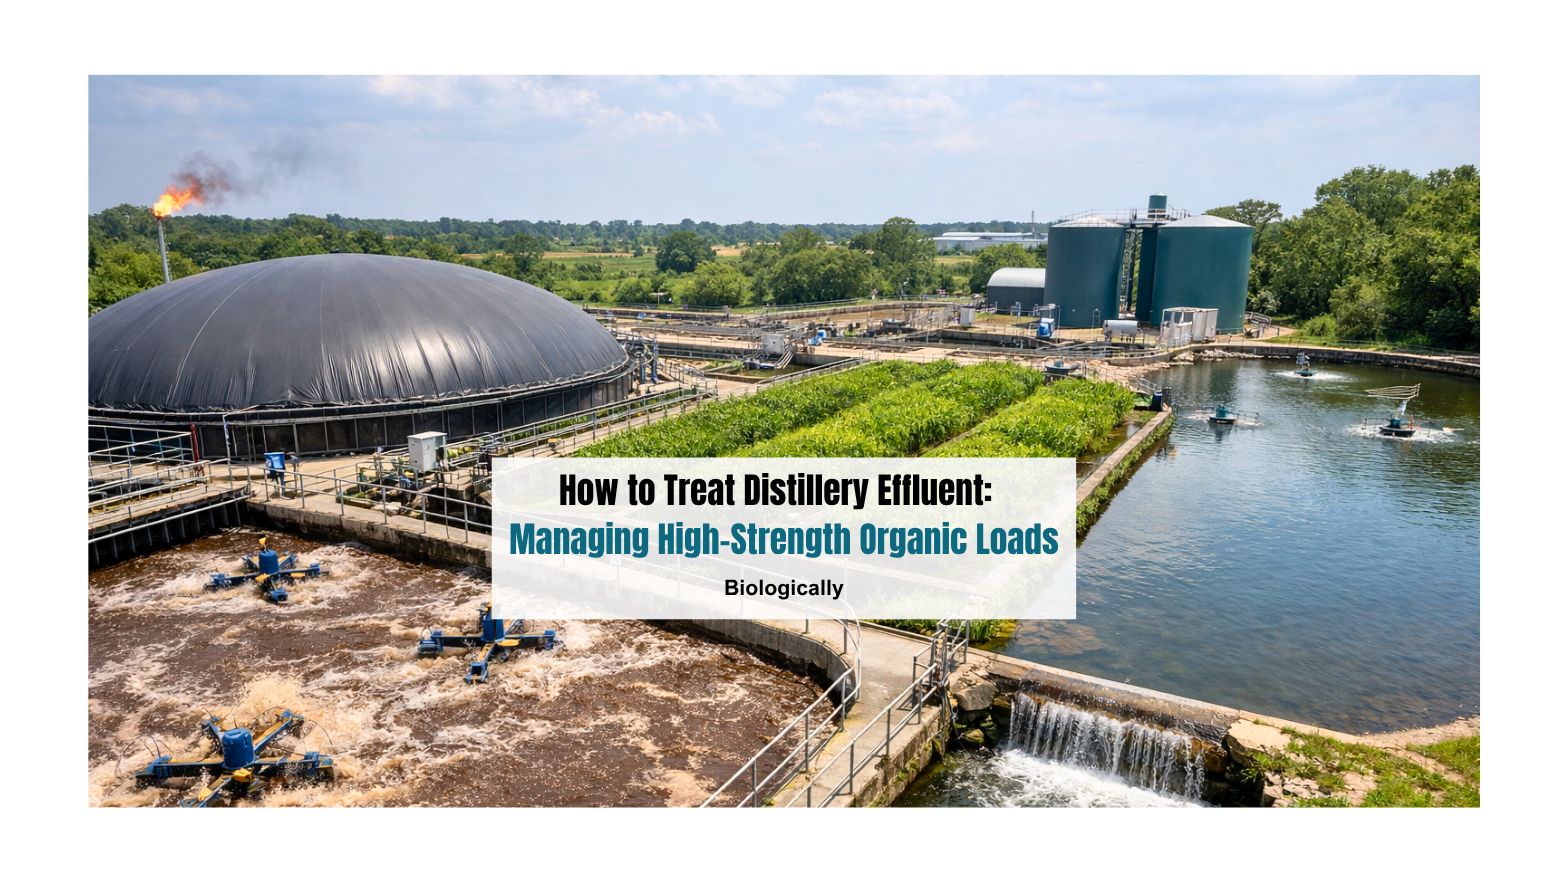
How to Treat Distillery Effluent: Managing High-Strength Organic Loads Biologically

The modern industrial landscape in India has reached a critical juncture. The dual pressures of economic expansion and environmental preservation are no longer negotiable; they are the two pillars upon which any successful enterprise must stand.

For the seasoned plant operator or the Environmental Health and Safety (EHS) manager, the transition from conventional treatment to the current era of Zero Liquid Discharge (ZLD) has been a profound paradigm shift. There is a specific, visceral kind of stress that only a professional in this field truly understands: standing on the catwalk of a treatment plant at two in the morning during a peak monsoon downpour, watching the foam rise in an aeration tank. In those moments, the weight of responsibility is heavy; a single non-compliant discharge could lead to a permanent closure notice from the National Green Tribunal (NGT) or the Central Pollution Control Board (CPCB).

The “hidden” cost of non-compliance is not merely the financial penalty, though those can reach into the crores, but the existential threat to the business itself. In today’s regulatory climate, authorities no longer just issue warnings; they revoke the Consent to Operate (CTO).

To thrive, the industry is moving away from a “hardware-centric” approach of simply building larger tanks. Instead, we are seeing a sophisticated, “biology-first” movement that prioritizes the optimization of microbial systems as the primary engine of detoxification. For the distillery sector, where organic loads are exponentially higher than municipal sewage, mastering this biological wastewater management is the only viable path forward.

The Anatomy of a High-Strength Challenge: Understanding Spent Wash

Distillery effluent, often called spent wash, stillage, or vinasse, is widely considered one of the most difficult industrial waste streams to treat globally. In India, where molasses is the primary feedstock for ethanol, the volumes are staggering. For every liter of alcohol produced, a typical distillery generates between 8.0 to 15.0 liters of spent wash.

The raw effluent is a dark brown, foul-smelling liquid that exits the process at high temperatures (up to 81°C) and with a highly acidic pH. Its organic strength is almost unparalleled. The Chemical Oxygen Demand (COD) and Biological Oxygen Demand (BOD) values are so high that direct discharge into a water body would result in the immediate and total depletion of dissolved oxygen, creating “dead zones” in our aquatic ecosystems.

Typical Characteristics of Raw Distillery Spent Wash

ParameterTypical Value Range (Raw)Units
pH3.8–4.5–
Temperature71.0–81.0°C
Chemical Oxygen Demand (COD)70,000–150,000mg/L
Biological Oxygen Demand (BOD)35,000–60,000mg/L
Total Dissolved Solids (TDS)58,000–76,000mg/L
Potassium (K_2O)5,000–15,475mg/L

The persistent brown color isn’t just an aesthetic problem. It is caused by melanoidins, complex polymers formed during fermentation. These compounds are remarkably resistant to standard treatment; they act as antioxidants that can actually be toxic to the very microorganisms meant to break them down. Furthermore, they block sunlight from entering rivers, halting photosynthesis and disrupting the entire food chain.

The Indian Regulatory Evolution: CPCB, NGT, and the ZLD Mandate

The regulatory landscape in India has evolved from simple “end-of-pipe” standards to a comprehensive, life-cycle approach. The mandate for Zero Liquid Discharge (ZLD) is now a baseline requirement for “Red Category” sectors like distilleries.

Under ZLD, no liquid waste is permitted to cross the plant boundary. Every drop must be treated, recovered, and recycled, leaving only dry solids for disposal. In states like Uttar Pradesh, the state pollution boards have been aggressive in enforcing these rules through Online Continuous Effluent Monitoring Systems (OCEMS).

Digital Surveillance and Continuous Compliance

With OCEMS, regulators have a 24/7 window into your plant’s performance. Parameters like pH, COD, and flow rate are transmitted directly to government servers. Deviations for even short durations can trigger automatic alerts and closure orders. This “digital surveillance” makes the role of specialized microbial cultures even more critical, as they provide the biological resilience needed to handle the “shock loads” that often lead to regulatory red flags.

The Science of Bioremediation: How Microbes Conquer Pollutants

At the heart of a successful distillery Effluent Treatment Plant (ETP) is a complex ecosystem. Bioremediation is the strategic use of microbes to transform toxic substances into harmless forms. This is typically divided into two crucial phases.

1. Anaerobic Digestion: The First Line of Defense

The heavy lifting begins in anaerobic reactors, such as the Upflow Anaerobic Sludge Blanket (UASB). Here, a consortium of bacteria breaks down 60% to 85% of the COD, producing valuable biogas as a byproduct.

However, this stage is a delicate balancing act. If the organic loading rate is increased too quickly, the system can “acidify.” This is where the production of volatile fatty acids outpaces their conversion to methane, leading to a total system crash.

2. Aerobic Polishing and the Challenge of Recalcitrance

The effluent exiting the anaerobic stage still carries a significant organic load and that signature dark color. This is where aerobic treatment, the Activated Sludge Process (ASP), takes over.

To break down the stubborn melanoidins, you need “specialist” microbes like Bacillus, Pseudomonas, and Nitrosomonas. These microbes act like mini-biochemical factories, producing extracellular enzymes that function like chemical scissors to snip apart complex polymers.

EnzymeMechanism of ActionImpact
LaccaseBreaks down aromatic ringsKey for decolourisation
Manganese PeroxidaseDegrades phenolsDeep COD reduction
Lignin PeroxidaseCleaves complex C-C bondsBreaks down recalcitrant matter

Operational Hurdles: The “Pain Points” of the ETP Operator

Operational Hurdles: The "Pain Points" of the ETP Operator

Maintaining a high-load ETP is a constant battle against biological instability. Operators often face three recurring nightmares:

Sludge Bulking

This occurs when the microbial mass becomes less dense and refuses to settle. Often caused by an overgrowth of filamentous bacteria during low oxygen levels, it can lead to a total loss of biological capacity as the biomass washes out of the system.

The Nutrient Imbalance

Microbes need a balanced diet. While distillery effluent is rich in nitrogen, it is often deficient in phosphorus. Without the right BOD:N:P ratio (generally 100:5:1), the microbes produce a “slimy” coating that makes the sludge notoriously difficult to manage.

The Monsoon Shock

In India, the monsoon is the ultimate test. Heavy rains can dilute effluent or cause rainwater ingress that exceeds the plant’s capacity. Power fluctuations during storms can also disrupt aeration, quickly turning a healthy aerobic tank into a foul-smelling swamp.

The Team One Biotech Advantage: Engineering Nature’s Solutions

Team One Biotech was founded on a simple principle: the world’s most significant pollution problems can be solved by its smallest inhabitants, microbes. Founded by Tejas Gathani, a veteran with nearly three decades of hands-on experience, the company addresses the “software” gap in wastewater treatment.

While many companies focus on selling heavy machinery, Team One Biotech positions itself as a strategic partner. They optimize existing infrastructure by enhancing the microbial engine that performs the actual detoxification.

Case Study: A Turnaround in Performance

A distillery struggling with high COD and unstable biomass implemented a targeted bioaugmentation program using the T1B Aerobio consortia. The results were transformative:

  • COD Reduction: Effluent COD fell to a stable range of 650–870 ppm (an 80–89% improvement).
  • Capacity Restoration: The plant returned to its full design capacity of 1,500 KLD from a restricted 500 KLD.
  • Energy Savings: Improved oxygen transfer efficiency led to significantly lower power consumption for aeration.

Beyond Wastewater: A Holistic Ecosystem

The expertise of Team One Biotech extends across the entire environmental spectrum:

  • Agriculture: Products like T1B Soil Biome enhance soil productivity and reduce the need for chemical fertilizers.
  • Aquaculture: Probiotic solutions improve water quality and gut health for shrimp and fish farming without antibiotics.
  • Lake Restoration: Reviving polluted urban water bodies using nano-bubble technology and microbial consortia.
  • Commercial Cleaning: Nature-based enzyme cleaners that provide sanitation without a harsh chemical footprint.

Future-Proofing: The Path to Resource Recovery

As we move toward 2026, “success” is being redefined. The most advanced distilleries are no longer viewing effluent as waste, but as a source of revenue.

  • Bio-CNG: The high organic content of spent wash is ideal for methane production, which can meet up to 60% of a plant’s energy requirements.
  • Potash Recovery: Molasses-based wash is rich in potassium. The salts recovered during the ZLD process can be turned into potash-rich ash, a valuable fertilizer.
  • Water Circularity: By optimizing biological treatment, distilleries can achieve water recovery rates of up to 98%, providing a stable water supply even in water-stressed regions.

A Vision for Sustainable Growth

The era of “dilution as the solution to pollution” is over. For the modern distillery, survival depends on a deep commitment to environmental stewardship. The regulatory pressure from the NGT and CPCB is not a hurdle to be jumped, but a permanent feature of the landscape.

Achieving excellence requires a shift in mindset. A treatment plant is not just a collection of steel and concrete; it is a living, breathing biological entity. By prioritizing the health of your microbial population and leveraging advanced bioaugmentation, you can transform your ETP from a source of stress into a cornerstone of operational stability.

The future of the Indian distillery sector is green, and it is powered by the intersection of science and nature. By embracing these biological solutions, we can ensure long-term viability, providing economic value to the nation and a cleaner environment for generations to come.

Move from compliance stress to process stability. Partner with Team One Biotech for your next biological audit.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!
Dairy Effluent Treatment: Reducing BOD in Milk Processing Plant Wastewater

You know the feeling. A notice from the Pollution Control Board lands on your desk, and suddenly your entire week pivots. The ETP that has been “managing” your dairy plant’s effluent is now under a microscope, and the BOD levels in your discharge report are not going to make the conversation easy.

For dairy plant managers across India, this is not a hypothetical. It is Tuesday morning.

The Indian dairy industry is among the country’s most economically vital sectors, processing millions of litres of milk daily across states like Punjab, Rajasthan, Uttar Pradesh, and Maharashtra. But behind every chilled packet and processed dairy product is a wastewater story that does not get told enough. Milk processing generates some of the most organically loaded effluent in the food industry, high in BOD, COD, fats, oils, and suspended solids. Left inadequately treated, it does not just attract regulatory action. It ferments. It smells. It kills aquatic life in nearby water bodies and quietly poisons the groundwater your neighbouring community depends on.

This piece is for the EHS manager who is tired of patching a broken system with chemicals and hoping the next inspection goes smoothly. There is a better way, and it starts with understanding what you are actually dealing with.

Why Dairy Effluent Is a Different Beast

Why Dairy Effluent Is a Different Beast

Most industrial wastewater is complicated. Dairy wastewater is complicated and stubborn.

When your plant cleans processing equipment, rinses pasteurisation lines, flushes out cheese vats, or disposes of off-spec batches, what goes down the drain is a concentrated cocktail of organic matter. Milk proteins, lactose, casein, butter fat, cleaning chemical residues, and in some cases animal waste from nearby collection points, all of it lands in your ETP. BOD levels in untreated dairy effluent routinely range across a broad spectrum, from a few hundred to several thousand mg/L depending on the product mix and plant hygiene practices. COD follows a similar trajectory, often running two to three times the BOD value.

This is what makes dairy effluent treatment technically demanding:

  • FOG (Fats, Oils, and Grease): These float to the surface, coat pipes, clog biological treatment media, and create a suffocating layer over aeration basins that kills the microbial activity you need.
  • High Nitrogen Load: Casein degradation releases ammonia-nitrogen into the effluent stream, complicating secondary treatment and raising Kjeldahl nitrogen values.
  • Fluctuating Organic Load: Seasonal milk procurement peaks, post-monsoon flush milk, festival season production surges, mean your ETP experiences dramatic influent swings, which destabilise conventional treatment systems.
  • Low pH Events: Acidic whey from paneer or curd production can crash your aeration basin’s pH and wipe out your microbial population almost overnight.

When untreated or poorly treated dairy effluent reaches surface water bodies, the consequences are severe. Dissolved oxygen depletes rapidly as microorganisms consume the organic load. Fish kills, algal blooms, and foul odours in surrounding areas follow. For a plant operating near agricultural land or a town water source, the liability, legal and reputational, is immense.

Bioremediation: The Green Future for Dairy Wastewater

Bioremediation: The Green Future for Dairy Wastewater

The conventional approach to dairy effluent treatment has largely relied on coagulation-flocculation, chemical dosing, and extended aeration. These methods work, partially. They are also expensive to run continuously, sensitive to load fluctuations, and generate large volumes of chemical sludge that create their own disposal headache.

Bioremediation offers a fundamentally different model.

At Team One Biotech, we have spent years developing and refining microbial consortia specifically engineered for high-FOG, high-BOD industrial wastewater. The principle is straightforward: instead of fighting the organic load chemically, you deploy the right microbial strains to consume it biologically, faster, more completely, and at a fraction of the residual impact.

Here is what happens when you introduce our specialised bacterial cultures into your ETP:

  • Lipase-producing bacteria break down FOG fractions that would otherwise coat your aeration tank surfaces and reduce oxygen transfer efficiency.
  • Protease-active strains digest milk proteins and casein, reducing nitrogen loading and preventing the build-up of putrefying solids.
  • Facultative and aerobic heterotrophs drive BOD reduction through accelerated organic oxidation.
  • Biosurfactant producers enhance the bioavailability of emulsified fats, allowing microbial attack on compounds that conventional systems simply cannot degrade.

The result is a measurable, consistent reduction in BOD and COD, without the chemical costs, without the sludge volume spike, and with a microbial community that adapts to your plant’s specific effluent fingerprint over time.

This is not a theoretical promise. It is applied microbiology in action.

Reducing BOD Step by Step: A Practical Framework

Reducing BOD Step by Step: A Practical Framework

Step 1, Primary Treatment (Physical Separation First)

Before any biological intervention can work effectively, your ETP needs a clean primary stage:

  • Screening and Grit Removal: Remove coarse solids and packaging remnants.
  • Grease Traps and DAF (Dissolved Air Flotation): Critical for dairy. A well-maintained DAF unit removes a significant fraction of FOG before it reaches biological treatment. This alone reduces the organic load entering secondary treatment substantially.
  • Equalisation Tank: Given the fluctuating nature of Indian dairy plant operations, an adequately sized equalisation basin is non-negotiable. It buffers pH swings and load spikes before they damage your microbial culture in the aeration basin.

Step 2, Secondary (Biological) Treatment

This is where bioremediation does its most important work:

  • Activated Sludge Process (ASP) or Sequential Batch Reactor (SBR): Both are viable platforms for microbial treatment. The key variable is MLSS (Mixed Liquor Suspended Solids), maintaining this within the right operational range ensures your biological community has enough active biomass to handle the load.
  • Sludge Age Management: One of the most overlooked parameters in dairy ETPs. Too short a sludge retention time, and nitrifying organisms wash out. Too long, and you accumulate inert solids that reduce treatment efficiency. Team One Biotech’s bioaugmentation products help stabilise this balance, particularly after a load shock or chemical dosing event that has crashed your native microbial population.
  • Nutrient Dosing: High-carbohydrate, high-protein dairy effluent sometimes lacks sufficient phosphorus for optimal microbial growth. Balancing the BOD:N:P ratio supports a more robust biological community.

Step 3, Tertiary Treatment and ZLD Compliance

Zero Liquid Discharge (ZLD) is increasingly mandated by CPCB and various SPCBs for food processing units in ecologically sensitive zones and those drawing on groundwater. For dairy plants, ZLD means:

  • Treated effluent passing through filtration, ultrafiltration, and Reverse Osmosis (RO) stages before water recovery.
  • The biological quality of effluent entering the tertiary stage directly impacts RO membrane life and fouling rates, which is why effective secondary BOD reduction is not optional, it is foundational.
  • Recovered water can be cycled back into CIP (Clean-in-Place) operations, cooling towers, or utility use, reducing freshwater consumption.

Our bioaugmentation programme reduces the organic burden reaching RO systems, extending membrane replacement intervals and lowering your tertiary treatment operational costs.

Compliance, Climate, and Cost For Dairy Effluent Treatment

Compliance, Climate, and Cost For Dairy Effluent Treatment

CPCB guidelines set discharge standards for food processing industry effluent that include specific BOD, COD, suspended solids, and oil-grease thresholds. State Pollution Control Boards often apply additional, more stringent norms. Non-compliance attracts penalties, closure notices, and in repeat cases, criminal liability under the Environment Protection Act.

But Indian dairy plants face a challenge that CPCB norms do not account for: seasonality. Post-monsoon flush milk production in states like UP, Punjab, and Gujarat significantly increases both milk procurement and processing volumes, and therefore effluent generation, over a relatively short window. Conventional chemical treatment systems, sized for average loads, are overwhelmed. Microbial systems, by contrast, scale biologically. A higher substrate load simply means more microbial growth and accelerated BOD removal, provided the system is seeded with the right culture and given adequate oxygen and nutrients.

Hot-climate fermentation is another reality. Organic matter in Indian dairy ETPs degrades faster in summer months, generating odours that affect community relations and invite complaints to the local SPCB. Deploying odour-control microbial blends alongside your treatment programme addresses this at the source rather than masking it with deodorants.

Team One Biotech: Your Compliance Partner, Not Just a Product Supplier

Team One Biotech’s product portfolio for industrial wastewater treatment India covers the full spectrum of dairy ETP needs:

  • Bioaugmentation cultures for BOD/COD reduction in ASP and SBR systems.
  • FOG-degrading microbial blends for grease trap and DAF system enhancement.
  • Odour management bioproducts for equalisation tanks and sludge handling areas.
  • Sludge volume reduction formulations that lower your dewatering and disposal costs.

Beyond dairy, our solutions are trusted across pharma effluent treatment, paper and pulp, sugar mill wastewater, and food processing sectors, which means if your facility handles multiple product lines or if you manage a diversified portfolio of plants, we have a solution tailored for each.

We do not hand you a product catalogue and leave. Our team conducts site-specific assessments, reviews your current ETP performance data, and recommends a dosing protocol calibrated to your actual effluent characteristics. We stay engaged through the stabilisation period, adjusting the programme as your plant’s operational conditions evolve.

Stop Reacting. Start Treating Properly.

The next PCB inspection is coming. The question is whether you will be explaining a compliance failure or presenting a treatment system that actually works.

BOD reduction in dairy is not a one-time fix, it is an ongoing operational commitment. Bioremediation, done right, makes that commitment sustainable, cost-effective, and genuinely compliant with CPCB wastewater compliance standards.

Ready to get your dairy ETP under control?

Request a Free Site Audit, Let our bio-experts assess your current ETP performance and identify gaps. Consult Our Industrial Wastewater Specialists, Speak with a senior team member about bioremediation for milk plants and get a customised treatment roadmap.

Team One Biotech. Bioremediation that works. Compliance you can stand behind.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!
Pharmaceutical Wastewater Treatment: How API Manufacturers Can Meet CPCB Discharge Norms

If your Consent to Operate renewal is coming up in the next six months, this post is worth reading carefully. CPCB and SPCB inspection teams across Baddi, Vapi, Hyderabad, and Ankleshwar have sharpened their scrutiny of API manufacturing units over the past two years. Effluent quality records, real-time monitoring data from OCEMS, and third-party lab reports are being cross-verified with a level of technical rigor that most legacy ETPs were simply not designed to withstand.

The problem is not that plant managers are careless. The problem is that pharmaceutical effluent, particularly from API synthesis, is one of the most technically complex wastewater streams in Indian industry. High chemical oxygen demand (COD) in the range of 8,000 to 25,000 mg/L, sharp TDS spikes during solvent recovery operations, low biodegradability indices (BOD:COD ratios below 0.3 in many cases), and the persistent presence of refractory organics such as sulfonamides, beta-lactam intermediates, and heterocyclic compounds, none of this is manageable through conventional physicochemical treatment alone.

If your plant is still relying on a coagulation-flocculation-filtration sequence as the primary treatment mechanism, you are already operating at a structural compliance deficit. Effective biological wastewater treatment requires adaptive biological management.

What CPCB Discharge Norms Actually Require from API Units

What CPCB Discharge Norms Actually Require from API Units

The Regulatory Baseline You Cannot Negotiate Around

Under the Environment Protection Act and the rules framed thereunder, API manufacturing units classified under the Red Category are subject to stringent effluent discharge standards. The current CPCB general standards for discharge into inland surface water include:

  • COD: Not exceeding 250 mg/L
  • BOD (5-day, 20°C): Not exceeding 30 mg/L
  • Total Suspended Solids (TSS): Not exceeding 100 mg/L
  • pH: 5.5 to 9.0
  • Total Dissolved Solids (TDS): No Universal Fixed Limit

For units operating in ecologically sensitive zones or discharging into coastal waters, state-level norms enforced by SPCBs such as GPCB in Gujarat or TSPCB in Telangana are often more stringent than the national baseline. In Hyderabad’s Patancheru-Bollaram cluster, for example, combined effluent treatment plants have faced closure orders not because individual units violated any single parameter, but because cumulative biological oxygen demand loading breached the receiving water body’s assimilative capacity.

The Shift Toward Biological Stabilization

The regulatory shift over the last five years has been unmistakable. CPCB’s technical guidance documents and NGT-driven action plans have increasingly moved away from the notion that physicochemical treatment alone constitutes adequate ETP design for pharmaceutical and bulk drug units. The current compliance expectation, whether stated explicitly in your CTO conditions or implied through inspection scoring rubrics, is biological stabilization, the treatment of effluent to the point where residual organic load is not merely precipitated or filtered out, but metabolically degraded.

This is where the operational gap is widest for most API plants, and where bioremediation-led solutions have moved from being a niche option to a mainstream compliance necessity.

Why Standard Activated Sludge Processes Fail in API Effluent

Why Standard Activated Sludge Processes Fail in API Effluent

The Refractory Organic Problem

Conventional activated sludge processes (ASP) depend on a mixed microbial community adapted to biodegrade organic matter using dissolved oxygen. These microbial communities perform adequately on domestic sewage, food processing wastewater, and moderate-strength industrial effluent. They are not equipped, by design or by acclimatization, to degrade the complex aromatic structures, halogenated compounds, and nitrogen-rich organics that characterize API manufacturing effluent.

When your aeration tank receives a batch discharge containing synthesis intermediates or solvent residues, two outcomes are typical. Either the MLSS concentration crashes due to biological toxicity, or the sludge becomes bulky with SVI values exceeding 200 mL/g, causing blanket carryover into the secondary clarifier and a direct spike in effluent TSS.

The Hydraulic and Seasonal Loading Variable

There is a complicating factor that rarely gets discussed in ETP audits but has a measurable impact on biological treatment performance: hydraulic loading variability driven by monsoon infiltration. In industrial clusters across Himachal Pradesh, Gujarat coastal belt, and Telangana, groundwater ingress into underground sewer networks during heavy rainfall months can dilute influent COD by 30 to 60%, disrupting the food-to-microorganism (F:M) ratio in aeration basins and destabilizing the biological equilibrium your system took weeks to establish.

Designing treatment responses around a static influent quality assumption is a common ETP design flaw.

Bioremediation in ETP: The Science Behind Specialized Microbial Cultures

Bio-Augmentation vs. Bioaugmentation-Plus-Acclimatization

Team One Biotech’s approach to pharmaceutical effluent treatment is grounded in targeted bio-augmentation, the introduction of specialized, pre-screened microbial consortia capable of degrading specific classes of refractory organics that the indigenous mixed liquor cannot metabolize.

These are not generic bacterial cultures. The strains developed and deployed by Team One Biotech for API manufacturing effluent are selected for:

  • Tolerance to high solvent concentrations and low BOD:COD ratios
  • Capacity to degrade aromatic ring structures including benzimidazole, pyrimidine, and chlorinated phenol intermediates
  • Stability under fluctuating pH (5.5 to 9.5) without requiring biological system restart
  • Compatibility with existing SBR, MBR, and extended aeration configurations without requiring capital modifications

Operational Performance Metrics

In bio-augmented systems treating pharmaceutical and API effluent, the following operational improvements are typically observed:

  • COD reduction efficiency: 75% to 92% across aeration and secondary treatment stages
  • BOD:COD ratio improvement in treated effluent: from a pre-treatment range of 0.15–0.30 to post-treatment values of 0.05–0.10
  • MLSS stabilization: 2,500 to 4,500 mg/L maintained without the sludge bulking events common in uninoculated systems
  • SVI normalization: typically brought within 80 to 150 mL/g range within 3 to 6 weeks of consistent dosing
  • Sludge volume reduction: 15% to 35% depending on influent organic load and existing digestion capacity

Note: These are general performance values. Specific results and operating parameters vary depending on the unique characteristics of each individual ETP and influent quality.

Cross-Sector Applicability, Dairy, Food Processing, Sugar, Tannery, and Paper Industries

Cross-Sector Applicability, Dairy, Food Processing, Sugar, Tannery, and Paper Industries

The biological treatment challenges described above are not exclusive to pharmaceutical units. Plant managers and EHS heads across several other high-load sectors face structurally similar compliance pressures.

Dairy and Food Processing

Dairy effluent carries high BOD loads (typically 1,500 to 4,500 mg/L) from fats, lactose, and cleaning chemical residues. The challenge here is less about refractory organics and more about rapid organic loading variability tied to production schedules. Bio-augmentation with lipase-producing and lactose-degrading microbial consortia accelerates treatment kinetics significantly in extended aeration systems.

Sugar and Distillery

Distillery spent wash remains one of the most challenging effluents in Indian industrial wastewater management, with COD values routinely between 80,000 and 120,000 mg/L. Melanoidin compounds, the dark-colored refractory polymers formed during fermentation, are highly resistant to conventional biological treatment. Specialized ligninolytic and melanoidin-degrading cultures can meaningfully reduce color and residual COD in the post-anaerobic treatment stage. 

Tannery Sector

In tannery clusters across Kanpur and Tamil Nadu, effluent contains sulphide, chromium, and protein degradation products in combination. Bio-augmented systems using sulphide-oxidizing and chromium-tolerant microbial consortia have demonstrated effective secondary treatment performance where standard ASP systems have repeatedly failed SPCB inspections.

Paper and Pulp

Lignocellulosic effluent from paper mills, with COD loads of 5,000 to 15,000 mg/L and high color values driven by lignin derivatives, responds well to fungal-bacterial consortium-based bioaugmentation, particularly in CETP-linked secondary treatment stages.

Note: These are general performance values. Specific results and operating parameters vary depending on the unique characteristics of each individual ETP and influent quality.

Next Steps for EHS Managers and Plant Technical Heads

If your ETP is consistently producing treated effluent with COD above 350 mg/L, if your sludge is bulking intermittently, or if your next CTO renewal is within the next 12 months, the time for remediation is before the inspection, not after the notice.

Team One Biotech provides:

  • On-site technical ETP audits covering biological process assessment, influent characterization, and CPCB compliance gap analysis
  • Customized microbial dosing charts specific to your effluent composition, ETP configuration, and seasonal hydraulic loading profile
  • Ongoing technical support through dosing adjustment, performance monitoring, and pre-inspection documentation review

To schedule a technical ETP audit or request a customized microbial dosing recommendation for your pharmaceutical, dairy, sugar, or tannery unit, contact Team One Biotech’s technical team directly. Bring your last three months of ETP monitoring data to the first consultation. The more specific the input, the more precise the solution.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!
Solving the ETP Sludge Crisis: 5 Ways to Reduce Sludge Volume and Disposal Costs

Every plant manager who oversees an ETP in India knows the feeling. It usually hits around budget review time, or worse, right before a regulatory inspection. You look at the disposal invoices stacking up, you look at the sludge drying beds that never seem to empty fast enough, and somewhere in the back of your mind a number keeps growing, a number that represents money leaving your plant for no productive reason whatsoever.

Sludge. Not the effluent you treat. Not the water you discharge. The leftover mass that your biological treatment process generates and that nobody, not your operators, not your contractors, not your compliance team, has a clean answer for.

This problem is not unique to any one sector. Textile dyeing units in Surat, API manufacturers in Hyderabad, dairy processors in Punjab, tanneries in Kanpur, the conversation is identical across all of them. Too much sludge, nowhere adequate to send it, and a cost curve that only moves in one direction. CPCB and SPCB inspection cycles are not getting more lenient. Third-party disposal contractors charge more every year and their compliance trail is increasingly under the scanner, which means your liability does not end when the tanker pulls out of your gate.

What compounds this in India specifically is the nature of industrial production itself. Seasonal peaks, inconsistent raw material quality, the monsoon’s effect on influent dilution, your ETP was designed around a baseline that real operations almost never maintain. Tropical temperatures accelerate microbial activity in ways that can swing sludge generation rates dramatically from one month to the next. Your operators are managing a living system under conditions that shift constantly, and the sludge output reflects every one of those shifts. Often, the solution lies in Advanced Bioremediation: Using Microbial Cultures to Solve Complex Industrial Waste as a way to stabilize these biological fluctuations.

The result is a reactive posture that most plants are stuck in: manage the sludge that already exists rather than address why so much is being produced in the first place. More dewatering capacity, more disposal contracts, more compliance paperwork, all of it treating the symptom while the underlying biology keeps generating the problem.

That reactive posture is exactly what needs to change. The five strategies below are not quick fixes. They are a biology-first approach to cutting ETP sludge at the source, and keeping it cut, season after season.

Way 1: Bio-Augmentation ,  Putting the Right Microorganisms to Work in Your Bioremediation System

Bio-Augmentation ,  Putting the Right Microorganisms to Work in Your Bioremediation System

Here is something most ETP operators already know intuitively but rarely act on: the microbial population running your aeration tank is probably not well-suited to your effluent.

Naturally seeded microbial communities are generalists. They colonize your system over time, establish a working equilibrium, and do a passable job under average conditions. The operative word is passable. When your influent COD spikes because production shifted to a higher-strength product, or when a batch of toxic intermediates hits your collection sump ahead of the ETP, those generalist populations struggle. They produce excess sludge as a byproduct of incomplete organic degradation, biomass that should have been converted to energy and CO₂ instead ends up in your sludge press.

Using Specialized Microorganisms in Bioremediation to Tackle Toxic Industrial Effluents 

To counter this, modern ETP management relies on the strategic deployment of specialized microorganisms selected for high-toxicity resistance. Unlike standard cultures, these “specialist” strains are capable of breaking down recalcitrant molecules like phenols, cyanides, and halogenated hydrocarbons that typically inhibit or kill off standard biomass. By integrating these specialized microbes into your bioremediation strategy, you ensure that even the most toxic industrial effluents are mineralized at the source. This targeted approach prevents the accumulation of hazardous chemical intermediates in the sludge, effectively lowering the toxicity profile of the resultant waste and making disposal significantly safer and more cost-effective.

Bio-augmentation addresses this directly. The principle is straightforward: instead of waiting for nature to seed your system with whatever microorganisms happen to be present, you deliberately introduce specialized, high-density microbial consortia that are matched to your specific effluent matrix. These are not generic culture products. Effective bio-augmentation uses organisms selected or developed for the particular compounds your plant generates, sulfate-reducing bacteria for tannery effluent, nitrifiers and denitrifiers for food processing wastewater, hydrocarbon-degrading strains for petrochemical ETPs.

The impact on sludge volume is direct. When microorganisms in bioremediation are well-matched to the organic compounds they are degrading, more of that organic load gets converted into energy and CO₂ rather than new biomass. Net sludge yield drops, typically by 20–35% compared to a poorly adapted mixed culture running the same load. (Note: These are general estimates and actual performance parameters will vary based on specific ETP design, effluent characteristics, and operating conditions.)

For Indian plants dealing with high seasonal variability, bio-augmentation also functions as an operational buffer. A robust, diverse microbial population recovers faster from shock loads. It bulks less. It bounces back from monsoon-related influent swings without the week-long process instability that typically follows, instability that is itself a significant driver of sludge generation spikes.

The work involved in bio-augmentation goes beyond adding a culture to your aeration tank. Microbial selection, dosing protocols, system monitoring, and periodic re-inoculation all require expertise. Getting the biology right is an investment. But the return, a lower, more stable sludge baseline, compounds over every month of operation.

Way 2: Fine-Tuning Your Aerobic and Anaerobic Processes for Smarter Biological Digestion

Running your ETP and running it well are two different things. Most plants operate in a fixed configuration that was set during commissioning and adjusted only when something goes wrong. Aeration runs at a fixed rate. The clarifier operates on a fixed cycle. Sludge gets wasted on a schedule that was set years ago and never revisited. The system produces effluent. Sludge accumulates. The cycle repeats.

What is almost never done is genuine process optimization, adjusting operating parameters based on what the biology actually needs at different load conditions. And the gap between a fixed-configuration ETP and an optimized one is where enormous quantities of excess sludge are quietly generated, day after day.

Understanding the difference between aerobic and anaerobic processes is central to this optimization.

The aerobic process is effective but biologically expensive. Aerobic bacteria consume oxygen to break down organic matter, and they produce significant biomass in the process, roughly one gram of sludge for every gram of COD removed under conventional conditions. That ratio is not fixed; it responds to operating parameters. But under standard activated sludge conditions, aerobic treatment is your biggest sludge generator.

The anaerobic process is fundamentally different. Anaerobic bacteria convert organic matter to biogas, primarily methane and CO₂, with dramatically lower biomass production. Anaerobic systems typically produce 80–90% less sludge than aerobic systems treating equivalent organic loads. (Note: These are general estimates and actual performance parameters will vary based on specific ETP design, effluent characteristics, and operating conditions.) For high-strength industrial effluents, distillery spent wash, dairy process water, chemical manufacturing effluent, a properly designed anaerobic pre-treatment stage can remove the bulk of the organic load before the aerobic polishing stage handles the rest. The aerobic system works on a fraction of the original load, generates a fraction of the original sludge, and consumes significantly less aeration energy in the process.

Beyond the aerobic-anaerobic balance, process fine-tuning also means:

  • Sludge retention time management: Longer SRTs give microorganisms time to metabolize their own cellular material, a process called endogenous respiration that directly reduces net biomass output.
  • Dissolved oxygen control: Maintaining DO in the right range prevents both anaerobic dead zones that cause bulking and over-aeration that wastes energy without improving treatment.
  • Load equalization: Smoothing influent peaks through equalization reduces shock loads, one of the primary drivers of excess sludge generation in Indian industrial ETPs where production schedules are rarely uniform.

These are not capital-intensive changes. They are operational disciplines that pay for themselves in reduced sludge volumes across every billing cycle.

Way 3: Mechanical Dewatering Combined With Biological Conditioning

Mechanical Dewatering Combined With Biological Conditioning

Let us be precise about what mechanical dewatering does and does not do. A belt press, filter press, or centrifuge does not reduce the mass of sludge your ETP generates. It removes water from the sludge that is already there, making it lighter, easier to handle, and cheaper to transport. The organic solids remain.

What determines how well your dewatering equipment performs is not the machine itself, it is the nature of the sludge going into it. And this is where biological conditioning changes everything.

Raw biological sludge dehydrates poorly. The reason is a substance called extracellular polymeric substances, EPS, which is essentially the structural glue holding microbial cells together in the sludge matrix. EPS is highly hydrophilic. It holds water tenaciously, which is why raw biological sludge going into a filter press often produces a cake with only 14–18% dry solids. The rest is water you are paying to transport and dispose of.

Biological conditioning treats this problem at the molecular level. Enzymatic preparations, specific enzyme blends selected for your sludge composition, break down the EPS matrix before dewatering. The sludge structure loosens. Water releases more freely. The same belt press or centrifuge that previously produced a 16% dry solids cake now produces one at 22–28%. (Note: These are general estimates and actual performance parameters will vary based on specific ETP design, effluent characteristics, and operating conditions.)

That improvement has a direct financial translation. Drier sludge is lighter sludge. Fewer disposal trips per tonne of dry solids. Lower transportation costs per cycle. And in many cases, particularly for plants in sectors like textiles or food processing where sludge composition is relatively consistent, improved dry solids content can shift the sludge from landfill disposal to co-processing in cement kilns, where it is used as an alternate fuel. The cost difference between those two disposal routes, calculated over a year of operations, often runs into significant lakhs for mid-to-large plants.

Biological conditioning requires no capital investment in new dewatering infrastructure. Your existing press or centrifuge remains the mechanical workhorse. The biology changes what goes into it, and dramatically improves what comes out.

A note before we continue: if you are spending more on sludge disposal than your operational budget can absorb comfortably, the answer is almost certainly in your process biology, not in more dewatering capacity or more expensive disposal contracts. Team One Biotech works with Indian industrial plants to identify exactly where excess sludge is being generated and what it is costing. Our sludge audits are detailed, specific, and actionable. If that conversation is relevant to where your plant stands right now, reach out to our technical team.

Way 4: Source Reduction and Hydraulic Retention Time Management

The most underrated sludge reduction strategy is also the most logical one: generate less organic load in the first place.

Source reduction is not glamorous. It does not involve advanced biology or specialized equipment. It involves looking honestly at your production process and identifying where organic waste enters your wastewater stream unnecessarily, and then doing something about it. In the Indian industrial context, this typically means three areas of focus.

Stream segregation is frequently overlooked in plants that grew incrementally without a master ETP design. High-strength process effluent, concentrated dye baths, mother liquor, high-COD process condensates, gets mixed with low-strength washdown water or cooling water before reaching the ETP collection sump. The result is a larger volume of moderate-strength effluent that your biological system has to process. Segregating these streams allows high-strength waste to be treated separately and efficiently, while low-strength streams bypass biological treatment entirely or receive minimal treatment. The reduction in total organic load hitting your ETP directly reduces biological sludge generation.

In-process water reuse reduces the total hydraulic volume entering your ETP. Less water means less biomass turnover and proportionally less sludge production. For water-intensive industries, textiles, food processing, paper, even modest reuse ratios can produce meaningful reductions in ETP load.

Process chemical substitution is a longer-term lever but a powerful one. Replacing poorly biodegradable surfactants, dispersants, or process aids with more biodegradable alternatives reduces the fraction of organic material that passes through biological treatment and ends up concentrated in sludge. This is particularly relevant for specialty chemical, pharmaceutical, and textile sector plants.

On the ETP operations side, HRT management deserves specific attention. Hydraulic retention time, how long wastewater spends in each treatment zone, directly affects how completely biological treatment removes organic load. When operators increase flow rates during production peaks to prevent upstream backup, HRT drops precisely when the biology needs more contact time. Organic material that should have been metabolized passes through instead, concentrating in the sludge fraction. Establishing HRT control protocols, supported by a proper equalization basin, keeps contact time consistent across load variations. The impact on sludge volumes, typically a reduction of 15–25% on a sustained operational basis, is one of the highest-return improvements available without any capital spend on new treatment infrastructure. 

(Note: These are general estimates and actual performance parameters will vary based on specific ETP design, effluent characteristics, and operating conditions.)

Way 5: Advanced Enzymatic and Biological Treatment to Break Down Refractory Organics

Every industrial ETP has compounds that its biological system cannot fully degrade. In textile plants, it is reactive dyes and their breakdown products. In pharmaceutical manufacturing, it is API intermediates and complex ring structures. In the leather sector, it is chromium complexes and vegetable tanning compounds. In specialty chemical plants, it is any number of synthetic polymers and aromatic compounds.

These are called refractory organics, compounds that resist conventional biological treatment because the microbial populations in a standard activated sludge system simply do not carry the enzymatic machinery to break them down. Instead of being metabolized, they accumulate in the sludge fraction. They increase sludge volume. They elevate the organic and sometimes hazardous content of your final sludge cake. And they complicate disposal, because sludge containing high concentrations of recalcitrant compounds often fails TCLP testing, forcing landfill disposal of material that might otherwise qualify for co-processing or land application.

Advanced enzymatic treatment targets these compounds specifically. Enzymes such as laccases, peroxidases, and hydrolases can depolymerize complex organic structures, breaking apart the molecular architecture of compounds that biological systems cannot attack directly. Once depolymerized, the simpler breakdown products become available for microbial consumption in the subsequent biological treatment stage. The result is a two-stage attack: enzymatic breakdown followed by biological assimilation.

When implemented as part of a comprehensive sludge treatment program, advanced enzymatic treatment delivers several compounding benefits:

  • Reduced total sludge mass: More complete degradation of organic compounds means less material accumulating in the sludge fraction.
  • Improved sludge biodegradability: Sludge with lower refractory organic content digests more effectively in downstream anaerobic digesters or co-composting systems, turning a disposal liability into a potential resource.
  • Improved regulatory classification: Lower TCLP values in the final sludge cake can shift disposal classification from hazardous to non-hazardous, a compliance milestone with direct cost implications that many Indian plants are actively working toward.
  • System stability: Better organic removal reduces the accumulation of inhibitory compounds in your biological system, improving overall treatment performance and reducing the frequency of process upsets that generate sludge spikes.

For sectors where refractory organics are a defining characteristic of the effluent, textiles, pharmaceuticals, specialty chemicals, this fifth strategy often delivers the most significant ROI precisely because it addresses both the compliance risk and the disposal cost simultaneously.

The ROI of Bioremediation: What Sludge Reduction Actually Means for Your Bottom Line

Put the five strategies above together and the cumulative impact on sludge generation is substantial. Plants implementing combined bio-augmentation, aerobic and anaerobic process optimization, biological conditioning, source reduction, and advanced enzymatic treatment have achieved total sludge output reductions in the range of 30–50% on a sustained operational basis. 

(Note: These are general estimates and actual performance parameters will vary based on specific ETP design, effluent characteristics, and operating conditions.)

For a mid-sized plant generating 500–800 tonnes of wet sludge annually, that reduction translates into measurable, line-item savings across every cost category associated with sludge management:

  • Fewer contractor disposal trips per month
  • Lower tipping fees per tonne of material disposed
  • Reduced dewatering equipment wear and maintenance
  • Smaller compliance documentation burden per audit cycle
  • In favorable cases, a shift in disposal classification that eliminates hazardous waste handling costs entirely

Beyond the direct financial impact, there is a strategic dimension that plant managers and CXOs increasingly recognize. Regulatory pressure on industrial sludge disposal in India is moving in one direction. CPCB and SPCB are tightening manifesting requirements, scrutinizing disposal contractor compliance trails more carefully, and in some states moving toward stricter limits on landfill-bound industrial waste. The plant that has already reduced its sludge volume by 35–40% enters that regulatory environment from a fundamentally stronger position than one still running a maximum-sludge-generation process.

Sludge reduction through bioremediation is not a cost center. When it is done correctly, it is one of the highest-return environmental investments an Indian industrial plant can make.

Stop Managing Sludge. Start Eliminating It.

Most plants dealing with a sludge problem respond with logistics: more trucks, bigger presses, higher-capacity storage. That approach does not solve the problem. It defers it at increasing cost, quarter after quarter, until the disposal invoices become impossible to ignore and a regulatory notice forces a more fundamental response.

The manufacturers getting ahead of this issue are taking a different approach. They are investing in the biological intelligence of their ETP, the microbial populations, the enzymatic toolkit, the process discipline, that converts organic load into energy and CO₂ rather than tonnes of wet sludge requiring disposal. They are treating their ETP not as a compliance obligation to be managed but as a biological system to be optimized.

Team One Biotech partners with Indian industrial plants across sectors to design and implement bioremediation-based sludge reduction programs built around your specific effluent chemistry, your existing infrastructure, and your compliance obligations. We do not sell generic microbial products or off-the-shelf enzyme packages. We start with a rigorous sludge audit, characterizing your effluent, assessing your biological treatment system, identifying the specific drivers behind your sludge generation, and quantifying what they are costing you. Then we build a program around what your system actually needs.

If sludge disposal costs are a recurring pressure in your operational budget, and for most Indian industrial plants they are, the first step is understanding exactly where that sludge is coming from and why it keeps coming.

Book a Sludge Audit with Team One Biotech. Our technical team will assess your ETP, map your sludge generation profile, and deliver a clear, specific, actionable reduction roadmap. No generic recommendations. No theoretical frameworks. A real plan for your plant, grounded in your actual numbers.

Contact Team One Biotech today and turn your most stubborn operational liability into a problem that stays solved.

Looking to improve your ETP/STP efficiency with the right bioculture?
Talk to our experts at Team One Biotech for customised microbial solutions.

Contact: +91 8855050575

Email:  sales@teamonebiotech.com

Visit: www.teamonebiotech.com

Discover More on YouTube – Watch our latest insights & innovations!-

Connect with Us on LinkedIn – Stay updated with expert content & trends!
Scan the code